


Choosing a Stamped Metal Parts manufacturer is a decision about repeatability, not just price. Grand View Research estimated the global metal stamping market at USD 218.5 billion in 2023 and projected a 4.3% compound annual growth rate from 2024 to 2030 in its 2024 market report. That scale signals a competitive, evolving industry; it does not prove that any individual supplier can meet your tolerances or delivery schedule.
W. Edwards Deming, a manufacturing quality expert, said, “Quality is everyone’s responsibility.” For buyers, that means looking beyond a polished capability sheet. Ask how the supplier controls tooling wear, verifies first-off parts, and tracks scrap. Request evidence: a sample inspection report, a production part approval record, and a clear explanation of how material changes are handled. If a press line runs overnight, who checks the first parts after a tool adjustment? Small details matter. A low quotation may omit inspection, packaging, or secondary operations, so compare the full scope. Also examine the supplier’s experience with your material, part geometry, and annual volume—not just its largest press tonnage.
No scorecard tells the whole story. A promising factory visit can still leave questions about communication or recovery plans when a tool fails. That uncertainty deserves attention, not a sales promise. The right choice is a manufacturer whose documented process, practical experience, and honest limits match your project’s real demands.
Before requesting quotes, turn the part drawing into a production brief. Specify the alloy and grade, sheet thickness, temper, finish, critical dimensions, tolerances, and acceptable burr direction. Identify which features need checking, such as a 0.2 mm slot or a hole-to-edge distance, and provide the expected inspection method where possible. Small details matter. A stamped part may look simple, yet a tight tolerance can affect die design, press choice, scrap rates, and inspection time. A drawing is not the whole story.
Define the production scope in numbers: prototype quantity, annual demand, order frequency, peak requirements, and expected program life. Tell manufacturers whether the quote should include tooling, deburring, plating, assembly, packaging, and inspection records. Ask who owns the tooling and how changes are handled. Deloitte’s 2024 Smart Manufacturing Survey found that 86% of manufacturing executives viewed smart factory solutions as a competitiveness driver over the next five years. That makes clear production data useful: ask how the supplier tracks runs, revisions, and quality results. Still, software cannot rescue a vague specification. I’ve seen estimates drift when “annual volume” meant a forecast to one buyer and a firm order to another. State what is confirmed, and what is only an estimate.

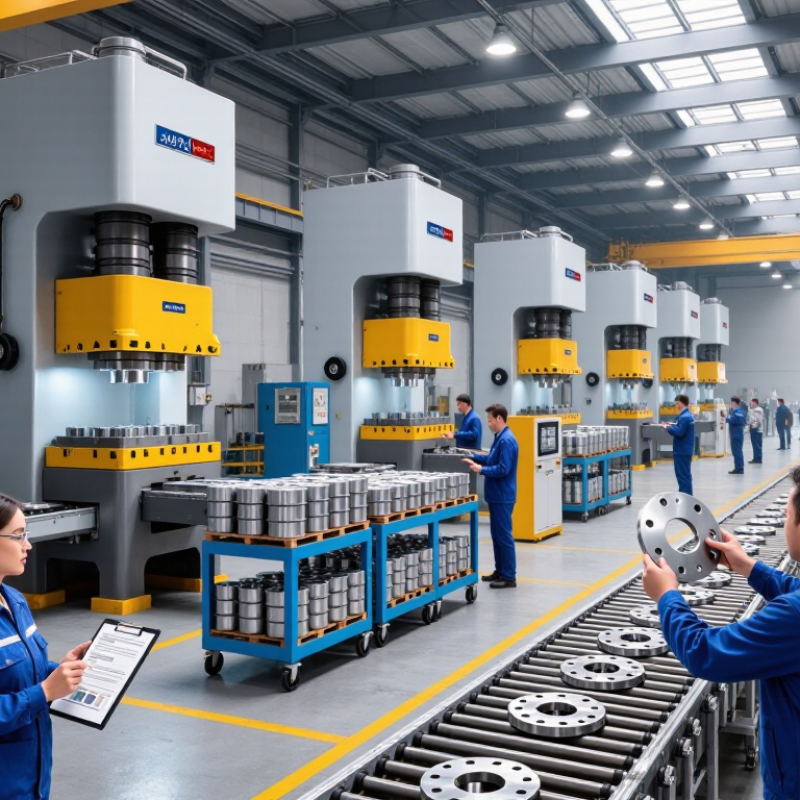
Choosing a stamped metal parts manufacturer starts with the machines behind the quote. Ask about press tonnage, bed size, stroke rate, and feeding systems. These details help show whether the shop can run your part consistently, not just make one sample.
A large press is not automatically the right press. The die must fit, and the material must feed without buckling or shifting. Tooling matters. For progressive dies, ask how operators monitor feed alignment, tool wear, and part dimensions during production. Look for practical controls, such as scheduled die inspections and documented checks with calipers or gauges. Ask who handles tool adjustments when a defect appears. Short sample runs can reveal issues before full production.
Material expertise matters just as much. Ask whether the team has worked with your specific alloy, thickness, temper, and surface finish. A slight change in sheet thickness or grain direction can affect bends and springback. Request material certifications and traceability records, then check that inspection results match the drawing’s critical dimensions. A manufacturer may list many capabilities, but the details can be less clear. I would not rely on a capability sheet alone. Discuss a real part and ask what risks the team sees. That judgment can be revealing.
| Assessment area | What to evaluate | Evidence to request | Positive indicators |
|---|---|---|---|
| Press capacity and configuration | Check whether press type, force capacity, bed size, stroke, and operating speed suit the part, material, and forming sequence. | Ask for equipment specifications and a proposed press-and-tooling plan for your part. Confirm that the required tonnage and working area are available. | The manufacturer explains how the press selection supports the part geometry and process, rather than relying on tonnage alone. |
| Stamping process options | Determine experience with the process relevant to the design, such as progressive-die, transfer, or single-operation stamping. | Review comparable part examples, process-flow descriptions, and the rationale for the recommended production method. | The team can discuss part complexity, production volume, tooling needs, and trade-offs between suitable processes. |
| Material knowledge | Verify experience with the specified alloy, thickness, temper or condition, and any material requirements affecting formability or strength. | Ask how material grade and condition are confirmed, how incoming material is identified, and how substitutions are approved. | The manufacturer considers material properties and tolerances during process planning and does not make unapproved material changes. |
| Material range and forming challenges | Discuss relevant materials, which may include aluminum, carbon or stainless steel, and copper alloys, as well as the challenges specific to your part. | Request examples of comparable material-and-feature combinations, such as bends, drawn features, or tight dimensional requirements. | The team identifies potential issues such as cracking, springback, galling, or surface marking and explains how these will be evaluated. |
| Feed and automation equipment | Assess coil or sheet handling, feeding, alignment, and automation appropriate to the material format and production plan. | Ask how feed setup is controlled and how the operation detects misfeeds or other process interruptions. | The setup and monitoring approach is clearly described, with controls suited to the selected press and material. |
| Tooling and die maintenance | Check how dies are designed, maintained, repaired, and protected against wear that could affect part quality or production continuity. | Review the tooling plan, maintenance practices, spare-parts approach, and responsibility for tooling changes. | Tooling condition and changes are managed systematically, with clear communication about ownership and maintenance responsibilities. |
| Inspection and process control | Determine how critical dimensions, material identification, and appearance requirements are checked during production. | Request sample inspection records, measurement methods, and the planned response to out-of-specification results. | Inspection methods are linked to drawing requirements, and nonconforming material is identified and controlled. |
| Capacity and production fit | Confirm that available equipment, staffing, and scheduling can support the expected order quantities and delivery plan. | Ask which production resources would be assigned, how capacity is planned, and how maintenance or downtime is considered. | The manufacturer provides a realistic production plan and explains how it will manage changes in demand or schedule. |
Compare manufacturers using the same part drawings, material specifications, annual volumes, and quality requirements so that equipment and expertise claims can be evaluated consistently.
When choosing a stamped metal parts manufacturer, look beyond polished samples. Ask how operators check critical dimensions, such as hole spacing or flange height, during production. A capable supplier should explain inspection frequency, gauge calibration, and what happens when a measurement drifts. Request sample inspection records, not just a verbal promise. Small details matter.
Certifications can indicate disciplined systems, but confirm that each certificate is current and covers the actual production site and process. Ask to review audit findings or corrective-action examples. A clean certificate alone may hide a weak process. Traceability should connect each shipment to material lot numbers, press settings, tooling, inspection results, and drawing revisions. If a defect appears, those records help isolate affected batches instead of relying on guesswork.
Tips: Ask for a sample traveler or lot record. Check whether it links the steel coil to the finished parts. Confirm how long records are retained and who can retrieve them. Then compare the paperwork with a real production run.
A factory visit can reveal gaps that documents miss. Look for labeled material racks, separated nonconforming parts, and gauges near the work cell. Ask an engineer to walk through one recent quality issue. The answer need not be perfect; it should be specific, documented, and candid about what changed afterward.
How to Choose a Stamped Metal Parts Manufacturer?
Compare Pricing, Lead Times, and Production Flexibility
Compare total cost, not just the quoted piece price. Ask suppliers to separate tooling, material, setup, inspection, packaging, and freight. A low unit price can hide expensive die revisions or minimum order quantities. Give every candidate the same alloy, thickness, annual volume, tolerances, and finish requirements. Check whether tooling maintenance is included. Details matter.
Break lead time into tooling, first-article approval, and recurring production. The Institute for Supply Management’s December 2023 Manufacturing Report on Business recorded a Supplier Deliveries Index of 49.9. Below 50 signals faster deliveries. This broad U.S. indicator is not a promise about stamped-part schedules. Coil availability, press capacity, and die trials still affect delivery. Request a dated launch plan with clear assumptions. One date without a production plan deserves scrutiny.
Tips: Send the same drawing revision to each supplier. Ask for sample schedules, change-order costs, backup press capacity, and weekly output ranges. Test flexibility with a realistic design change, such as moving a hole. Get the response in writing. Fast replies are useful, but they do not prove reliable production control.
A sample is more than a piece of metal. Use it to check critical dimensions, hole locations, edge condition, and fit with mating parts. Measure it against the drawing, and inspect the finish under consistent lighting. Ask whether the sample came from production-intent tooling and the proposed material. A hand-finished prototype may look excellent but reveal little about repeatability. Check a few parts, not just the best-looking one. Small differences matter.
Customer references can show how a manufacturer handles real production, not just a sales presentation. Ask about comparable part complexity, material, order volume, and delivery expectations. Find out how the supplier communicated when a quality issue or schedule change occurred. Specific examples are more useful than general praise. References may still be selective, so weigh their comments alongside your own sample inspection and documented process controls. No single check is enough.
Tips: Request a small sample set and record measurements. Ask references what they would change, too. That question can uncover useful details. Samples cannot predict every production variation, and I would not treat a polished finish as proof of consistent quality.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

