


7 Tips for Choosing a New Energy Car Production Line?

Choosing a New Energy Car Production Line is a major investment, not just a decision about machines. The line must match the vehicles you plan to build, your expected output, and the space available in your factory. A battery pack station, robotic welding cell, and final inspection bay each need room, reliable utilities, and clear material flow.

Small details matter. A bottleneck at one station can slow the entire operation. Before comparing suppliers, define practical targets for production capacity, product variation, automation, and future expansion. Ask how equipment handles different vehicle models, how quickly operators can change setups, and what maintenance support is available. Request specific performance data and references from comparable installations, rather than relying on headline figures alone.

There is no single production line that fits every manufacturer. A highly automated system may improve consistency, but it can also demand specialized skills and careful upkeep. A lower-cost option may suit a smaller launch, yet leave limited room to scale. That trade-off deserves honest review. Even a detailed plan can miss things; utility upgrades and staff training are easy to underestimate. The following seven tips offer a practical framework for assessing suppliers, process design, quality controls, energy use, and long-term service. Use them to ask sharper questions, compare proposals on the same basis, and choose a line that fits real operating needs—not just a polished presentation.
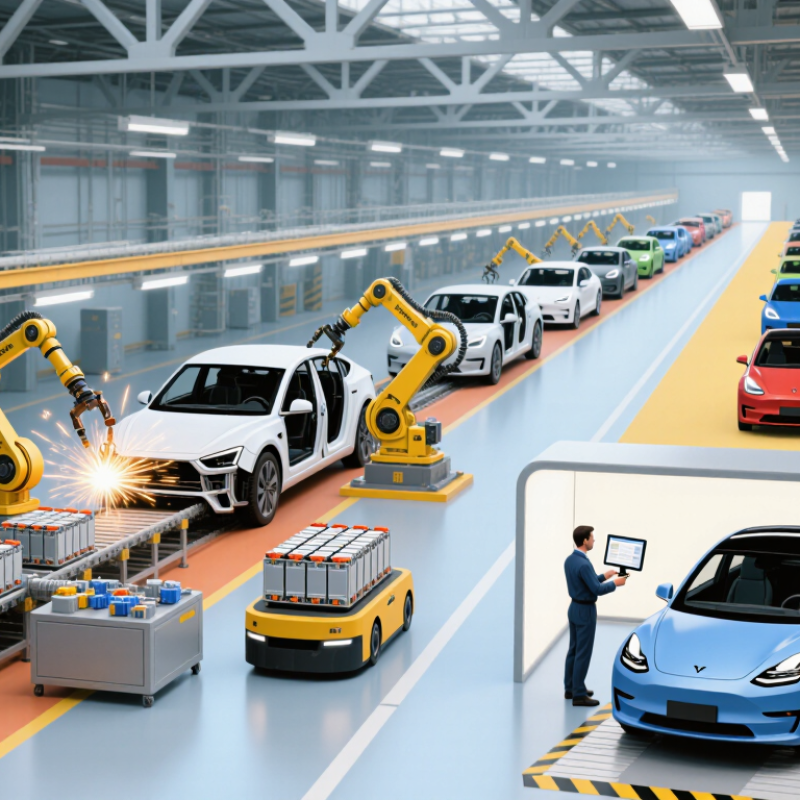
7 Tips for Choosing a New Energy Car Production Line?

Forecast Capacity Against 14 Million EV Sales in 2023 (IEA)

The International Energy Agency reported about 14 million electric-car sales worldwide in 2023, nearly one in five new cars. Its Global EV Outlook 2024 projected sales could reach around 17 million in 2024. These figures set a demand signal, not a factory order: regional mix, model size, and local sourcing all affect production needs. A line sized directly to global sales would be a risky assumption.

Tip: Build capacity scenarios, not a single forecast. Model a steady case and a faster-growth case, then test both against shifts in vehicle mix. The IEA’s 2023 sales figure includes different markets and vehicle types, so convert it into relevant units, such as packs per shift. Check cycle times at each station, from cell handling to end-of-line testing. That gap matters.

Tip: Leave room to adjust. Modular fixtures, expandable testing areas, and practical changeover plans can help a line respond without major reconstruction. Use weekly output, downtime, and first-pass yield to compare actual performance with the forecast. A planned buffer is useful, but oversized equipment can sit idle. Forecasts will miss sometimes; review assumptions with suppliers and operations teams before committing capital. Sources: IEA, Global EV Outlook 2024; IEA, Global EV Outlook 2023.


Planning New Energy Vehicle Production Capacity Against Global EV Sales

Global electric car sales and the IEA’s 2024 sales forecast, in millions of vehicles

Global electric car sales rose from about 3 million in 2020 to nearly 14 million in 2023. The IEA projected sales to exceed 17 million in 2024. Production-line plans should account for expected demand, ramp-up time, and the flexibility to scale output.

Source: International Energy Agency (IEA), Global EV Outlook 2024. 2024 figure is a forecast.

Map Cell-to-Pack Flow and Specify Battery Dry Rooms at ≤−40°C Dew Point

A cell-to-pack production line should be mapped around the battery’s actual journey, not just the equipment list. Track each cell from incoming inspection through sorting, module-free assembly, enclosure sealing, and end-of-line testing. Mark every handoff. A poorly placed buffer can expose open cells to humid air or create a queue beside a critical station. Walk the proposed route with operators and maintenance staff; they often spot access problems that drawings miss.

Specify battery dry rooms to maintain a dew point of −40°C or lower where the process requires it. That is not the same as setting a room temperature. Define the target at the product exposure zone, then check it with calibrated sensors near doors, transfer ports, and workstations. Use airlocks and controlled material transfer to limit moisture entering with carts or packaging. Keep logs for dew point, door openings, and alarms. Small details matter. A door left ajar can undo hours of stable conditions. Still, a very dry room alone does not guarantee dry cells; incoming materials, storage time, and open-process duration also need controls. Teams sometimes overlook those details, and the map should be revised when trial runs reveal them.

7 Tips for Choosing a New Energy Car Production Line? - Map Cell-to-Pack Flow and Specify Battery Dry Rooms at ≤−40°C Dew Point

Tip What to Map or Specify Useful Data or Check Selection Guidance
1. Map the complete cell-to-pack flow Show the route from incoming cell inspection through cell grouping, electrical connection, module or cell-stack assembly, pack enclosure, electrical testing, and end-of-line release. Include rework loops and material handoffs. For each station, record process time, buffer capacity, operator tasks, equipment interface, and quality check. Identify where the design uses a module-based route or a cell-to-pack route. Request a station-by-station flow diagram and a layout showing people, product, and material movement before approving the line concept.
2. Define the dry-room boundary and dew-point requirement Identify every operation where moisture-sensitive battery materials or exposed cells require controlled humidity. Specify a battery dry-room dew point of ≤−40°C for the applicable production zones. State the measurement locations, operating condition, alarm limits, monitoring frequency, recovery procedure, and records. Verify conditions at the product or process area, not only at the air-handling unit. Define the required dew point at the point of use and during normal production. Confirm that doors, pass-throughs, personnel entry, and material transfers are included in the moisture-load assessment.
3. Size capacity from demand and available production time Translate the required annual good-pack volume into a required line rate using the planned shifts, operating days, scheduled hours, and expected yield. A basic planning relationship is: required gross output rate = required good output ÷ planned production time ÷ expected yield. Validate cycle time at the constraint station and account for changeovers and planned downtime. Ask suppliers to show the assumptions behind their capacity figures and to identify the bottleneck, parallel equipment, and buffer strategy.
4. Specify cell handling and joining processes Describe cell identification, orientation, positioning, clamping, busbar or connector joining, insulation placement, and inspection. Match the process to the selected cell format and pack architecture. Specify process windows and verification methods for critical operations, such as weld monitoring, dimensional checks, electrical continuity, and insulation checks where applicable. Require trials with representative cells and components. Confirm that tooling accommodates approved tolerances and that failed or suspect cells can be safely segregated.
5. Build quality checks and traceability into the route Link cell, component, process, and pack records through a unique identifier. Define inspection gates, nonconformance handling, rework authorization, and final release criteria. List the data to capture at each operation, such as cell IDs, equipment and recipe IDs, timestamps, process results, operator or system status, and test outcomes. Demonstrate a complete genealogy record for a sample pack, including how the system prevents unapproved parts or failed process steps from advancing.
6. Plan battery safety and abnormal-event controls Review hazards and controls for cell storage, handling, electrical testing, charging or discharging steps, thermal events, and damaged-cell isolation. Coordinate design with site safety and applicable regulations. Document risk assessments, emergency stops, guarded equipment, electrical isolation, detection and alarm interfaces, safe storage arrangements, and response procedures as applicable to the process. Require a process-specific safety review and clear ownership for integrating equipment safeguards with facility alarms and emergency response plans.
7. Check utilities, maintainability, and acceptance criteria List electrical power, compressed air, cooling, exhaust, network, floor space, access, and dry-room interfaces. Define routine maintenance and calibration needs for production and measurement equipment. Agree on commissioning and acceptance tests for safety, cycle time, quality checks, traceability, uptime measurement, and the specified dry-room dew point under stated operating conditions. Use measurable, documented acceptance criteria and require training, spare-parts information, maintenance instructions, and handover of equipment and process records.

Choose Modular Automation for 400 V and 800 V Vehicle Platforms

A production line designed for one voltage architecture can become a bottleneck when product plans change. Modular automation lets manufacturers share core conveyors and handling systems while adapting battery assembly, high-voltage testing, and end-of-line stations for 400 V and 800 V platforms. The International Energy Agency’s Global EV Outlook 2024 reported nearly 14 million electric car sales in 2023, about 18% of global car sales. It projected roughly 17 million sales in 2024, or more than one in five cars sold.

Build flexibility into the physical line, not just its software. Use replaceable fixtures, adjustable locating pins, and clearly separated test recipes. An 800 V battery pack may need different insulation checks and test equipment from a 400 V pack. Small details matter. Shared stations can still handle platform-specific checks, provided operators cannot load the wrong recipe or connector. Validate those safeguards during pilot runs, with real packs and production timing.

A modular line is not magic. It can raise upfront costs, and extra changeover options may slow a poorly planned station. Ask suppliers to demonstrate an actual platform change, then measure the time, tooling needs, and quality checks involved. One uncomfortable question deserves attention: will the factory really change variants often enough to justify every module? The answer may be imperfect, but it should shape the investment.

Build Quality Gates Around IATF 16949 and ISO 26262 Requirements

7 Tips for Choosing a New Energy Car Production Line?
Build Quality Gates Around IATF 16949 and ISO 26262 Requirements

A production line should make defects visible before they travel downstream. Translate IATF 16949 controls into practical checks at each station: torque records, weld inspection, battery module identification, and verified software versions. Set clear acceptance limits and define who can stop the line. Small checks matter.

For safety-related functions, connect ISO 26262 activities to the actual production process. A gate might verify a controller’s programmed version, confirm test results, and retain traceability to its serial number. Keep records accessible, not buried in separate systems. When a test fails, the work instruction should explain how to contain the unit and investigate the cause.

Do not treat a signed checklist as proof of control. Review how operators use it during busy shifts, and sample real production records during audits. This can slow output at first. That pressure is real, especially during ramp-up. Still, weakening a gate to meet a daily target can hide recurring faults. Review the evidence with quality, manufacturing, and functional safety teams, then revise the process when actual results expose gaps. No line is perfect; the useful one makes problems easier to find and harder to repeat.

Compare Takt Time, Traceability, and OEE Before Approving Total Cost

7 Tips for Choosing a New Energy Car Production Line?

Compare Takt Time, Traceability, and OEE Before Approving Total Cost

A production line can meet its quoted cycle time and still miss customer demand. Calculate takt time from realistic shift hours, planned breaks, and forecast volume—not the best-case output on a supplier’s slide. The International Energy Agency reported nearly 14 million electric cars sold worldwide in 2023, about 18% of all car sales. That growth makes flexible capacity valuable, but forecast demand is not a production plan. Ask for cycle-time data from comparable battery, motor, and final-assembly processes, including changeovers and stoppages.

Traceability should connect each vehicle to its battery, critical components, process settings, and inspection results. Check that operators can retrieve a record by vehicle ID, and test what happens when a scanner fails or a data field is missing. Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 86% of surveyed manufacturing executives expected smart manufacturing to drive competitiveness within five years. Still, digital records alone do not guarantee better quality. A disconnected system can create tidy dashboards and incomplete evidence.

Compare OEE using the same definitions for availability, performance, and quality; otherwise, supplier figures are not comparable. Request shift-level records, exclude no losses without explanation, and inspect the assumptions behind planned production time. Small gaps matter. Price the full system: integration, training, spare parts, software support, and ramp-up scrap. I would challenge a perfect OEE projection; real lines have awkward stops, and early data can be messy. Approve total cost only after a witnessed trial shows the line can meet takt while preserving traceability and reliable output.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.
