How to Choose a Hot Extrusion Hydraulic Press Line
Choosing a Hot Extrusion Hydraulic Press Line is a production decision, not a simple equipment purchase. The right system must match alloy behavior, billet size, profile geometry, output targets, and available floor space. Aluminum, copper, and harder alloys demand different pressure, temperature, and tooling strategies. A line that looks powerful on paper may still deliver unstable profiles, excessive scrap, or slow cycle times. Real performance matters.
Begin with measurable requirements. Record billet diameter, maximum extrusion force, ram stroke, working speed, container dimensions, heating range, and expected annual tonnage. Check how the press handles temperature variation, because a small thermal drift can change surface quality and dimensional accuracy. Inspect the loading table, die-change method, cooling system, puller, saw, and handling equipment as one connected process. Safety guarding, emergency stops, hydraulic filtration, and noise control deserve equal attention. They are not optional details. Ask suppliers for tested references, commissioning records, component brands, maintenance intervals, and energy data from comparable lines. Factory demonstrations can reveal vibration, oil leakage, control delays, and awkward operator access. Photos cannot.
Cost should include tooling, utilities, training, spare parts, downtime, and future upgrades. A cheaper press may become expensive when seals fail repeatedly or automation cannot expand. Still, no checklist is perfect. Experienced engineers should validate calculations with actual billets and trial runs. Review the evidence carefully. This approach supports a safer, more reliable investment and helps buyers choose a Hot Extrusion Hydraulic Press Line that fits production today and remains practical tomorrow.
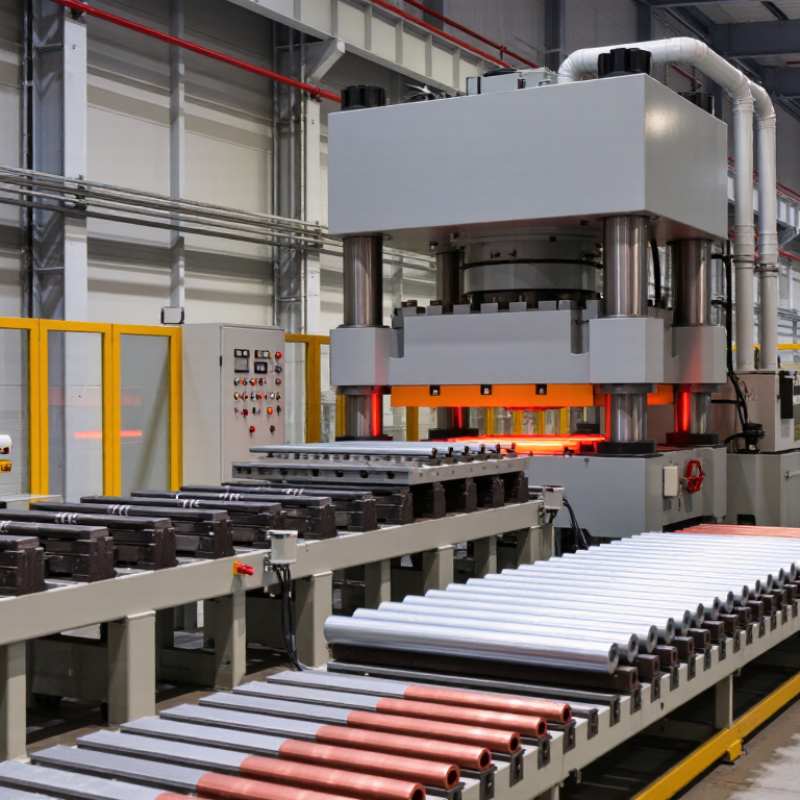
Define Product Requirements: Alloys, Profiles, 350–500°C Billet Heating
Choosing a hot extrusion hydraulic press line starts with the product, not the press. Define alloy grades, billet diameter, profile shape, wall thickness, extrusion ratio, and target output. Aluminum alloys may require billet heating near 350–500°C, but the correct setting depends on chemistry and profile difficulty. A thick, simple section may tolerate a different temperature than a thin, intricate one. Record a temperature window, not one fixed number. Small differences matter.
Heating must be uniform through the billet, including its core. Specify furnace capacity, heating rate, temperature sensors, transfer time, and allowable temperature variation. Measure the core. A surface reading can look correct while the center remains cold. This condition may cause unstable flow, higher press loads, or surface tearing. Ask for trial data from representative billets. Include measurements after heating, not only furnace display values. The first estimate is rarely perfect.
Match press force and ram speed to the alloy, profile, billet size, and extrusion ratio. Confirm container dimensions, die support, lubrication method, cooling, puller, runout table, and cutting accuracy. Complex profiles need stable speed control, not simply greater tonnage. Test, then revise. A line designed only for today’s profile can become expensive quickly. Yet oversizing wastes energy and reduces sensitivity at low loads. Review the design with production and maintenance teams. Their objections may reveal missing requirements.
Calculate Press Capacity Using 10–100 MN Force and Extrusion Ratios
How to Choose a Hot Extrusion Hydraulic Press Line
Choosing a hot extrusion hydraulic press line starts with required force, not advertised output. Available systems commonly range from 10 to 100 MN. Capacity depends on billet diameter, alloy, temperature, die geometry, friction, and extrusion ratio. Extrusion ratio equals billet cross-sectional area divided by finished profile area. A 20:1 ratio creates much higher resistance than a 5:1 ratio.
Consider a 150 mm billet with an area of approximately 17,700 mm². At a 20:1 ratio, the profile area is about 885 mm². A simplified estimate uses F = A0 × flow stress × deformation factor. With 90 MPa flow stress and a factor of 1.8, the calculated force reaches roughly 2.9 MN. This is only a starting estimate. Container friction, billet temperature loss, and die resistance can raise the actual load significantly. The first calculation is often wrong.
For a production line, engineers should compare peak force with continuous working force. A calculated requirement of 18 MN may justify a 25 MN press, depending on operating conditions and safety margins. Smaller aluminum profiles may suit 10–20 MN equipment, while larger copper or steel sections can require 40–100 MN. Verify stroke length, extrusion speed, container diameter, billet length, and control response. Do not size the press from ratio alone. Test data may reveal an uncomfortable correction.
Select Tooling and Hydraulic Systems for 5–50 mm/s Ram Speeds
How to Choose a Hot Extrusion Hydraulic Press Line
For hot extrusion, ram speed must match billet temperature, alloy behavior, and die resistance. A 5–50 mm/s range gives useful flexibility, but maximum speed is not always productive. Lower speeds can reduce surface tearing and stabilize metal flow through complex dies. Higher speeds may improve output when the billet remains thermally consistent. The first calculation is rarely perfect. Confirm it with controlled trials.
Choose tooling that tolerates repeated thermal cycling and supports accurate alignment. Die land length, container clearance, and lubrication strongly affect required force. The hydraulic system should provide steady motion at low speed and responsive acceleration when demand changes. Size pump flow from ram area and target velocity, then verify pressure capacity under peak load. Servo control, pressure sensors, and temperature monitoring can reveal unstable flow before defects become visible. Oil cooling also matters during long production runs.
Tips: Test three speed points: 5, 25, and 50 mm/s. Record force, exit temperature, surface quality, and cycle time. A modest speed often wins. Inspect die wear after each trial, because a speed setting that works today may become unsuitable later. Keep acceleration gradual near billet breakthrough. Operators should review the data, not rely only on the machine display.
How to Choose a Hot Extrusion Hydraulic Press Line
Hydraulic flow and power requirements for a 500 mm bore cylinder across 5–50 mm/s ram speeds
Selection guidance: As ram speed increases, the required hydraulic flow rises proportionally. At 50 mm/s, a 500 mm bore cylinder requires approximately 589 L/min of ideal flow and about 196 kW of hydraulic power at 20 MPa. Actual system sizing should allow for efficiency losses, acceleration, pressure peaks, cooling capacity, and the selected tooling load.
Tooling consideration: Use rigid, well-supported dies and guided tooling for higher-speed operation. Lower speeds are generally preferable during billet breakthrough and high-load forming, while higher speeds can be used during steady-state extrusion when temperature, lubrication, die strength, and product quality remain within process limits.
Verify Safety, Energy Use, Automation, and ISO 12100 Compliance
Choosing a hot extrusion hydraulic press line starts with risk, not tonnage. ISO 12100:2010 requires hazard identification, risk estimation, and risk reduction throughout the machine lifecycle. It is not a decorative certificate. Ask for documented guarding, emergency stops, two-hand controls, and safe maintenance access. During a plant review, check whether an operator can reach the die area while pressure remains stored. Small gaps matter.
Energy use deserves measured evidence. The U.S. Department of Energy reports that motor-driven systems consume more than half of industrial electricity in the United States. Request motor efficiency data, idle-load readings, and pump performance at typical cycles. Variable-speed control can reduce wasted flow, but only when properly tuned. Watch the pressure gauge during standby. A silent pump may still consume power.
Automation should improve consistency without hiding hazards. The International Federation of Robotics recorded 541,302 industrial robot installations worldwide in 2023. That figure shows automation is expanding, but integration quality varies. Require interlocked doors, validated safety functions, clear fault messages, and manual recovery procedures. ISO 13849-1 can support safety-related control design alongside ISO 12100. Review the safety validation file, not only the sales specification. Machines are rarely perfect. Allow time for operator feedback, repeat risk assessment, and corrective changes before production approval.





