


Choosing a 100% Eptfe Membrane in 2026 requires more than comparing prices or reading impressive product claims. The right choice depends on application conditions, verified material composition, and long-term performance. A membrane may look identical on a datasheet, yet behave differently under heat, pressure, humidity, or repeated cleaning.
Start with the operating environment. Check temperature limits, chemical exposure, pore structure, air permeability, water entry pressure, and mechanical strength. For outdoor equipment, ultraviolet resistance and seam durability matter. For filtration systems, particle retention and pressure drop deserve careful testing. For breathable protective products, comfort and moisture vapor transmission cannot be ignored. Small details often become expensive problems.
Ask the supplier for traceable batch records, technical data, test methods, and independent certifications. Reliable manufacturers should explain how they control PTFE purity and membrane thickness. They should also provide samples for practical evaluation, not only polished brochures. Test the material in conditions that resemble actual use. A laboratory result may not predict field performance perfectly.
Look beyond the headline number.
A true 100% Eptfe Membrane should be assessed against the complete assembly, including backing fabric, adhesive, coating, and sealing process. These supporting layers can change breathability and durability. It is easy to focus on purity and overlook installation quality. That would be a mistake.
Some recommendations remain uncertain. Newer production methods may improve consistency, but their service history can be limited. Therefore, document assumptions, compare evidence, and challenge every unsupported promise. The best decision is not always the cheapest or most advanced option. It is the option supported by relevant testing, transparent documentation, and realistic experience.
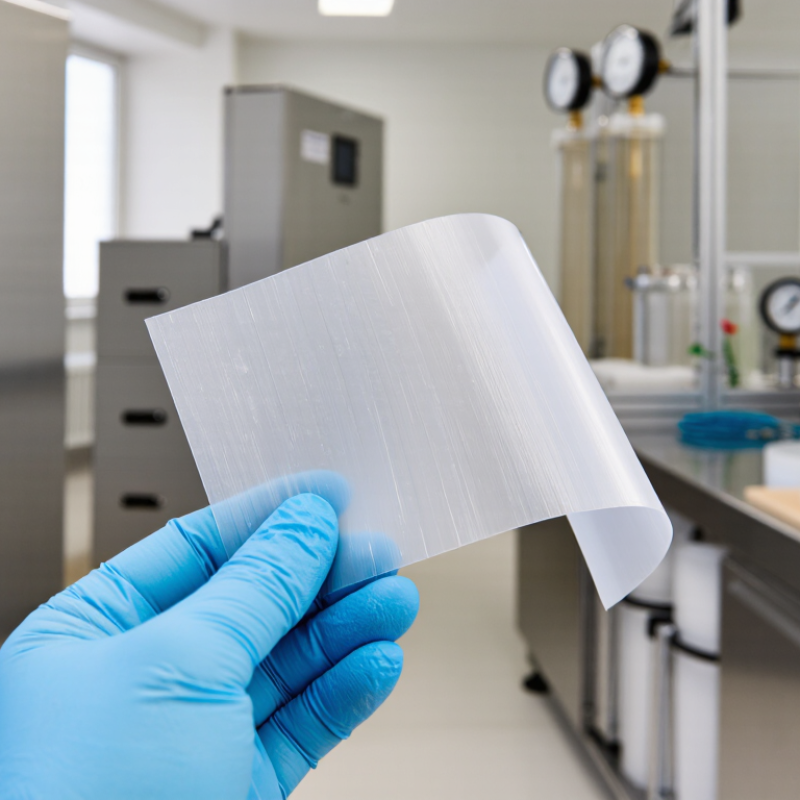
A 100% ePTFE membrane is made from expanded polytetrafluoroethylene, without adding another polymer to its functional layer. Expansion creates a network of microscopic pores. These pores block liquid water while allowing vapor and air to pass. The effect resembles a rain jacket with invisible ventilation windows. Typical ePTFE pores are much smaller than water droplets but larger than water vapor molecules. This explanation is useful, though real performance depends on pressure, temperature, and contamination.
The membrane’s low surface energy supports strong water repellency. Its chemical resistance also suits filtration, protective garments, and equipment venting. According to MarketsandMarkets, the global membrane filtration market was valued at about 26.3 billion dollars in 2023 and may reach 38.7 billion dollars by 2028. That growth does not represent ePTFE alone. It still shows rising demand for controlled separation technologies. Grand View Research also identifies filtration and breathable materials as active membrane applications. Data can guide selection, but it cannot replace testing. A specification sheet may look perfect. Field conditions may disagree.
Tips: Check whether “100% ePTFE” describes the membrane layer or the whole laminate. Ask for pore size, air permeability, hydrostatic pressure, thickness, and thermal limits. Test samples under realistic humidity and pressure. Inspect seams too. Weak seams can defeat a strong membrane. I would also question unusually high ratings without test standards, sample conditions, or revision dates. Small details matter.

How to Choose 100% ePTFE Membrane in 2026?
Which Performance Properties Matter for Your Application?
Choosing a 100% ePTFE membrane starts with the working environment, not the product label. Confirm the material is truly expanded PTFE, without unwanted backing layers or additives. Then define the application’s pressure, temperature, chemicals, and moisture exposure. A membrane protecting outdoor electronics may need different performance than one used in laboratory filtration.
Pore size controls particle retention, while air permeability affects pressure equalization and ventilation speed. Water entry pressure matters when rain, spray, or condensation is expected. Check both values together. High airflow alone can create weak moisture resistance. That detail is easy to miss. For moving equipment, examine tensile strength, elongation, tear resistance, and sealing performance. A membrane may perform well in a test fixture but fail around a sharp housing edge.
Chemical compatibility requires practical testing with the actual oils, solvents, cleaning agents, and vapors. Temperature ratings should include short-term peaks, not only continuous operation. Ask for test methods, sample conditioning, and lot-to-lot variation. Results without test conditions are difficult to trust. I would also inspect aging data under heat, humidity, pressure cycling, and ultraviolet exposure. Some specifications look excellent initially, yet change after months of use. Build a small prototype and measure airflow, leakage, and mechanical damage before approving full production. That extra step may reveal an inconvenient weakness.
The chart shows a practical selection priority for common ePTFE membrane applications. Pore size and porosity strongly influence filtration efficiency and flow rate, air permeability affects pressure drop, hydrostatic pressure resistance supports liquid-blocking applications, and tensile strength improves handling and installation reliability. The scores are engineering guidance on a 1–5 scale rather than a universal test specification; actual requirements depend on membrane construction, thickness, support layers, test method, and operating conditions.
Typical evaluation methods include ASTM F316 for pore-size characterization, ASTM D737 for air permeability, ASTM D751 for hydrostatic resistance, and ASTM D882 for tensile properties. Always compare values measured using the same test conditions.
Choosing a 100% ePTFE membrane in 2026 starts with pore structure, not a catalog label. The membrane should match the contaminant, fluid, pressure, and expected service life. For fine particles, a smaller mean pore size can improve capture. However, it usually increases pressure drop. A narrow pore distribution gives more predictable retention. A wider distribution may improve flow, but it can allow early breakthrough. That trade-off is easy to underestimate.
For gas filtration, compare pore size with particle diameter and measure air permeability at the actual operating pressure. For liquids, check bubble point, wetting behavior, and liquid breakthrough. Hydrophobic ePTFE can repel water, yet surfactants or low-surface-tension fluids may overcome that protection. Temperature and chemical exposure can also change performance. Do not rely on one headline efficiency number. Ask for test conditions, sample thickness, effective area, and the testing method.
During pilot testing, run clean and loaded pressure-drop curves. Also inspect the membrane after cycling, vibration, and cleaning. A membrane that performs well on day one may age differently in service. Smaller pores are not automatically better. In some systems, a slightly larger pore structure delivers steadier flow and lower energy use. I have seen test plans fail because humidity was ignored. That was avoidable. Use measured data. Verify the weakest operating condition before scale-up.
Choosing 100% ePTFE in 2026 requires more than reading a product label. The phrase “100%” should be defined clearly: no support fabric, coating, filler, or blended polymer. Request the technical data sheet, batch certificate, and full material declaration. A certificate helps, but it is not proof by itself.
Experienced buyers should verify each lot, not only the first sample. Fourier-transform infrared spectroscopy can confirm the PTFE chemistry, while thermal analysis may reveal unexpected residues. Microscopy can show the expanded node-and-fibril structure. Check thickness, pore-size distribution, air permeability, bubble point, tensile strength, and water-entry pressure. These values must match agreed tolerances. Small differences matter. I have seen visually identical membranes perform differently after humidity exposure.
Tips: Ask for sealed lot samples and independent laboratory testing. Compare test methods, not just numbers. Confirm traceability from raw resin to finished roll. Review storage conditions, because heat, compression, and contamination can change performance. A supplier who explains failed tests honestly is often more reliable than one promising perfect results. Still, supplier interviews can be subjective. Use written acceptance criteria and retain reference samples for future comparison.
When comparing 100% ePTFE membranes, do not judge cost by square-meter price alone. A lower quote may exclude seam treatment, edge details, transport, testing, or replacement access. Ask for a complete installation estimate. It should show membrane quantity, labor hours, lifting equipment, surface preparation, and expected downtime. In real projects, these hidden items can change the budget significantly. Request technical data, batch traceability, and independent test results. Documents matter.
Installation quality strongly affects performance. The substrate must be clean, stable, and properly drained before placement. Installers should control tension, overlaps, and penetrations around pipes or supports. Poor alignment can create wrinkles that collect water and dirt. Weather also matters. Windy conditions make handling difficult, while moisture can weaken bonding or sealing work. A site inspection before delivery is worth the time. I have seen small preparation errors cause expensive adjustments later.
Long-term performance requires more than initial strength. Compare chemical resistance, ultraviolet stability, temperature limits, permeability, cleaning needs, and repair methods. Check how the membrane behaves after repeated exposure, not only in new-condition testing. Ask for maintenance intervals and realistic service-life evidence. A perfect spreadsheet does not exist. Actual life depends on design, climate, traffic, and workmanship. Leave room for uncertainty. The best choice is often the membrane with clear evidence, practical installation support, and predictable maintenance costs.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

