Choosing an Arm Ball Joint supplier in China involves more than comparing prices or browsing polished product photos. This guide examines manufacturers through practical criteria: engineering capability, material control, production consistency, and communication during sampling. These details affect how a joint performs under steering loads, road vibration, and repeated movement.
A reliable supplier should explain its manufacturing process clearly. Ask how it controls forging or casting quality, heat treatment, machining tolerances, and surface protection. Review drawings, inspection records, and test procedures where available. Check how the supplier manages ball-stud hardness, socket fit, grease retention, and dust-boot sealing. Small differences can matter. A neat sample is useful, but it cannot prove that every production batch will match it. Requesting batch traceability and clear acceptance criteria helps reduce uncertainty.
Global buyers also need to consider application fit, not just factory capacity. Confirm vehicle coverage, mounting dimensions, load requirements, packaging, and export experience before placing an order. Ask how the manufacturer handles design changes, nonconforming parts, and after-sales questions. Details matter. A supplier may be strong in volume production yet less suited to custom development, and that distinction is easy to miss. The manufacturers discussed here are presented as candidates for evaluation, not as a universal ranking. Buyers should verify current certifications, references, and technical documentation independently. No supplier is perfect. Careful comparison helps identify a partner whose capabilities, quality controls, and service match the needs of a specific market.
OICA’s 2024 production statistics put worldwide motor-vehicle output at 93.5 million units in 2023, roughly 10% above 2022. That is substantial. For buyers evaluating Chinese upper arm ball joint manufacturers, this scale matters: small design differences can affect high-volume vehicle programs. Yet production volume is not a quality certificate. Fit depends on dimensions, taper, articulation angle, boot sealing, and verified fatigue performance.
The International Energy Agency’s Global EV Outlook 2024 reports nearly 14 million electric cars sold in 2023, close to 18% of global car sales. Electrification does not remove suspension joints; varying vehicle mass and packaging make careful load and durability checks important. Ask suppliers for material traceability, heat-treatment records, corrosion-test results, and endurance data linked to the exact part number. Compare sample measurements with your drawing, not just a general certificate. A spreadsheet can look tidy; factory variation is less tidy. OICA counts vehicles, not individual components, so its figure indicates market scale, not direct ball joint demand. Keep that distinction visible when reviewing quotations and capacity claims.
A ball joint is a compact spherical bearing that lets a steering knuckle pivot while the suspension moves vertically. In a double-wishbone layout, upper and lower joints connect the knuckle to separate control arms. MacPherson designs commonly use a lower joint, with the strut guiding the upper end. Load-carrying joints support spring forces; follower joints mainly locate the knuckle and transmit steering or braking forces. Actual load paths depend on geometry.
Studs and housings are commonly steel; bearing liners may be polymer or metal, depending on design. Buyers should check load direction, articulation angle, corrosion protection, boot sealing, and grease retention—not just dimensions. Ask suppliers for material specifications and validation details tied to the intended suspension geometry. A drawing alone can look convincing. It may still miss real-world impacts.
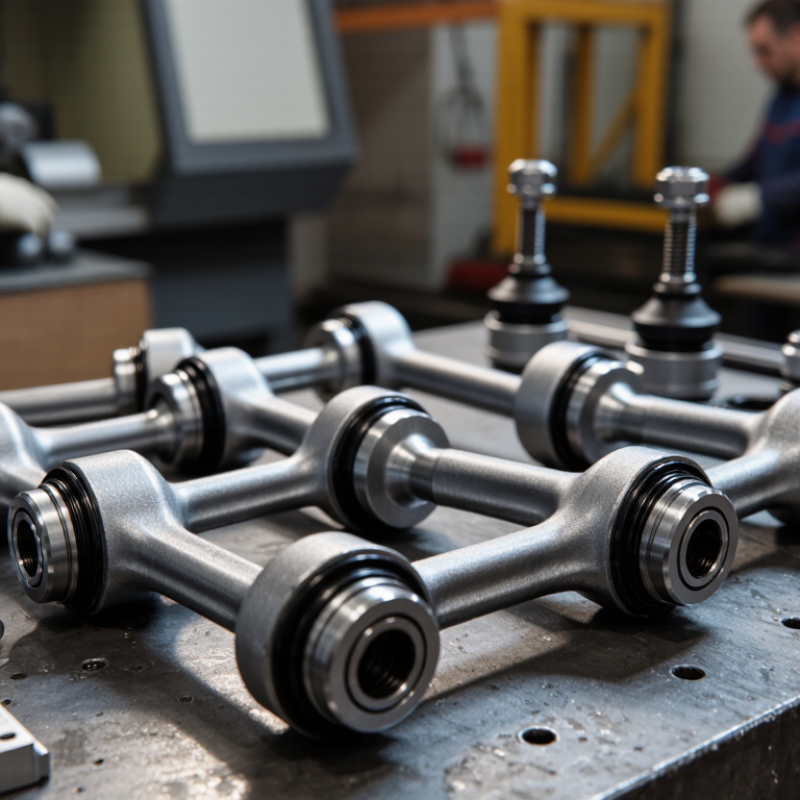
China’s leading ball joint manufacturers supply parts for steering and suspension systems to aftermarket and vehicle-production buyers. Product ranges may include upper and lower arm ball joints, complete control arms, and repair kits. Designs differ across vehicle platforms, so matching a part by appearance alone can cause fitment problems. Check dimensions, thread size, taper, and mounting points against an approved drawing or sample.
Production may involve forging or casting, precision machining, heat treatment, and final assembly. Ask suppliers how they control ball-stud hardness, housing dimensions, grease retention, and dust-boot sealing. Useful evidence includes material specifications, inspection records, and repeatable test results for load, articulation, and corrosion resistance. A polished brochure is not enough. Request the test method and acceptance limits.
Export capabilities can cover sample coordination, carton labeling, pallet preparation, and shipment documentation. Confirm lead times, minimum order quantities, packaging details, and procedures for handling nonconforming parts before placing a large order. Communication may be quick, while technical replies remain vague. Ask again. Compare traceability and consistent quality alongside price; a low quotation alone cannot show how a joint performs after months of road use.

For global buyers, an arm ball joint supplier’s quality system deserves more than a certificate check. IATF 16949:2016 certification can indicate a structured automotive quality system, but verify its scope, site, and current validity. Then compare documented procedures with the work actually happening on the production floor. Look closely.
PPAP 4th Edition records help buyers assess whether a part and its manufacturing process are understood before approval. Review the control plan, process flow, risk analysis, dimensional results, and material evidence together. For a ball joint, measurements should relate to real features, such as stud diameter, housing fit, and articulation torque. A tidy submission is useful, but it cannot prove that every shift follows the same controls.
Traceability should connect each finished lot to its material batch and key operations, including machining and heat treatment where applicable. Ask the supplier to retrieve one lot’s records during a live review; note how quickly the links are found and whether quantities reconcile. Paper trails can still hide gaps. That is worth admitting. Buyers should also check how nonconforming parts are identified, contained, and prevented from re-entering production. A brief audit of records and shop-floor practice often reveals more than a checklist alone.
A polished sample is not proof of production control. Request dated test reports for articulation torque, axial play, pull-out strength, fatigue cycles, and corrosion resistance. Check part numbers, test conditions, sample sizes, and acceptance limits. A result without its method is difficult to compare. Ask whether the tested joint matches the material, boot, grease, and heat-treatment specification you plan to order.
Capacity needs evidence, too. OICA reported that China produced about 30.2 million motor vehicles in 2023, but national output does not reveal one factory’s ball-joint capacity. Request monthly output by process, shift records, equipment lists, and recent delivery performance. Compare these against your forecast and ask which component could become a bottleneck. Numbers matter. A spreadsheet can still overstate usable capacity.
Treat lead times as separate stages: tooling, samples, validation, production, and shipment. The World Bank’s 2023 Logistics Performance Index scored China 3.7 out of 5; use this context, not a promise of transit time. Confirm the shipping route and build in buffer days. Verify quality certificates with their issuing bodies, and map material declarations to your destination-market requirements. Even a thorough audit can miss a weak traceability link, so request a batch record and follow one lot from incoming steel to packed shipment.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.




