


China has become a significant sourcing base for laboratory chemicals, analytical standards, and research-grade materials. UN Comtrade trade data shows China remains a major global exporter of chemical products. This scale gives international buyers broader access to solvents, acids, buffers, reagents, and customized formulations. Yet volume alone does not prove quality.
A dependable Chemical Reagent Supplier should support each shipment with a clear certificate of analysis, safety data sheet, batch number, purity method, and production date. These details matter when a small impurity can distort chromatography results or change a reaction’s color. ISO 9001-based quality systems can strengthen consistency, while ISO/IEC 17025-accredited testing provides stronger evidence for measured results. Buyers should still verify the actual scope and validity of every certificate.
Industry reports also underline the market’s steady expansion. Grand View Research identifies laboratory chemicals as a growing global market, driven by pharmaceutical research, biotechnology, environmental testing, and academic laboratories. Its analysis highlights rising demand for high-purity and application-specific products. That trend sounds positive, but it creates a practical concern: faster purchasing can encourage weak supplier checks.
Reliable sourcing requires more than a competitive quotation. It requires technical communication, stable packaging, traceable raw materials, and export documentation aligned with GHS, REACH, and destination-country requirements. The OECD’s chemical safety guidance supports stronger information sharing across the supply chain. Packaging should arrive sealed, labeled, and dry, with no unexplained residue around the cap. China offers real manufacturing depth. However, buyers must evaluate evidence, not marketing language. That is where supplier selection becomes a technical decision.
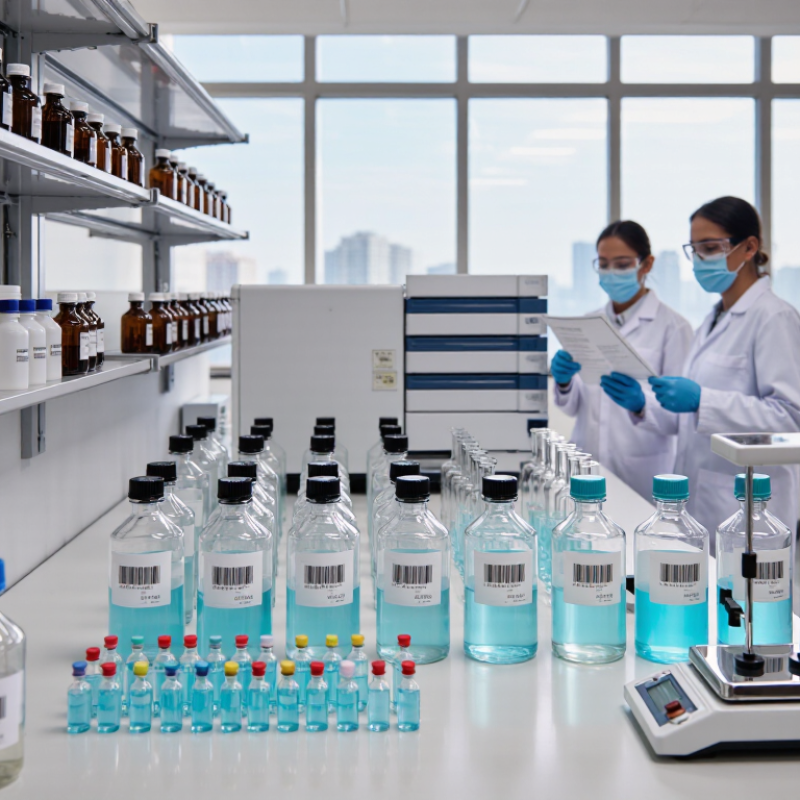
China’s chemical reagent supplier landscape is broad, specialized, and uneven. Manufacturers serve universities, diagnostic laboratories, industrial testing centers, and research facilities. Major production clusters often combine technical staff, logistics providers, and packaging services. This structure can shorten delivery times for international buyers.
Reliable suppliers usually provide certificates of analysis, batch numbers, safety data sheets, and traceable production records. Their websites may show strong technical language, but documents matter more than polished claims. Buyers should request current samples and compare purity, packaging, labeling, and test methods. Details matter.
Factory audits can reveal storage conditions, calibration practices, and moisture control procedures. Some suppliers offer flexible packaging for small laboratories, while others focus on bulk industrial orders. Communication quality is also important. Clear answers about lead times and quality limits often indicate practical experience. The market is not perfectly uniform. A supplier may perform well on routine reagents but struggle with unusual specifications. That weakness should be discussed early, not hidden behind sales promises. Careful verification remains essential because one inconsistent batch can disrupt an entire experiment.

A capable chemical reagent supplier should offer clear, practical product categories. Common groups include analytical reagents, laboratory solvents, buffer salts, indicators, and high-purity inorganic compounds. Organic reagents support synthesis, testing, and routine laboratory preparation. Different grades serve different purposes. Analytical-grade materials require tighter impurity control than general laboratory grades.
Quality begins with measurable evidence. Each batch should have a certificate of analysis showing identity, assay, moisture, and key impurity results. Lot numbers must connect the product to production and testing records. Reliable suppliers also provide safety data sheets, compliant labels, and suitable packaging. Light-sensitive materials may need amber containers. Moisture-sensitive powders need sealed inner protection.
Details matter. A small labeling error can delay an international shipment or compromise a test. Experienced suppliers inspect seals, appearance, and documents before dispatch. They also confirm storage temperatures and transport conditions with buyers. Independent testing can strengthen confidence when a result is critical. Still, no supplier should pretend that every batch is perfect. Testing methods have limits, and specifications sometimes need review. Open communication about deviations is more reliable than polished promises. Quality standards should support safe use, repeatable results, and informed purchasing across different laboratory environments.
China Top Chemical Reagent Supplier for Global Buyers
Reliable chemical reagent supply depends on more than competitive pricing. Manufacturing controls must remain consistent from raw material selection to final packaging. Skilled technicians record batch numbers, production dates, purity results, and storage conditions. Small details matter. A cloudy solution or damaged seal can signal deeper handling problems.
Testing should match the reagent’s intended use. Laboratories may review identity, assay, moisture, residue, and impurity data. Independent verification can strengthen confidence when the application is sensitive. Each shipment should include a clear certificate of analysis and safety data sheet. However, paperwork is not proof by itself. Buyers should compare test methods, acceptance limits, and sample results before approval.
Regulatory compliance requires practical attention. Labels should show hazard information, concentration, lot identification, and recommended storage temperatures. Documentation must support applicable transport and chemical-control requirements in the destination market. Requirements can change, and suppliers may miss updates. That weakness deserves honest review. Regular internal audits, traceable records, and trained staff reduce avoidable risks.
Tips: Request a recent batch sample. Check the seal, label, and appearance on arrival. Confirm that the certificate matches the lot number. Store reagents in a monitored area, not beside incompatible materials. Keep purchase and testing records together.
| Business Dimension | Common Industry Data | Relevant Standard, Test, or Document | Global Buyer Consideration |
|---|---|---|---|
| Reagent Grade Classification | Common grades include laboratory, analytical, molecular biology, HPLC, and trace-metal grades. Required purity depends on the intended application. | Product specification, certificate of analysis, pharmacopeial or analytical-grade requirements where applicable. | Confirm assay, impurity limits, water content, residue on ignition, and application-specific acceptance criteria before purchase. |
| Identity and Assay Testing | Typical analytical techniques include titration, gravimetric analysis, UV-Vis spectroscopy, infrared spectroscopy, and chromatography. | Validated or documented test methods; method selection varies according to the chemical and specification. | Request the test method, result, specification limit, and unit for every critical quality attribute. |
| Trace-Metal and Elemental Impurities | Elemental impurity testing commonly uses ICP-OES or ICP-MS, depending on detection limits and the required application. | Instrument calibration records, detection limits, and a test report listing measured elements. | Specify target elements and maximum limits, especially for pharmaceutical, semiconductor, environmental, and analytical applications. |
| Water and Moisture Control | Moisture may be measured by Karl Fischer titration, loss on drying, or another method appropriate to the material. | Specified moisture limit and documented test procedure. | Moisture-sensitive reagents require suitable seals, desiccant protection where applicable, and controlled storage conditions. |
| Chromatographic Purity | HPLC, GC, and ion chromatography are commonly used to measure organic impurities, residual solvents, or ionic components. | Chromatogram or test report, system suitability information, and defined impurity limits. | Confirm column type, detector, retention-time criteria, and whether the reported value is area percentage or a calibrated concentration. |
| Batch Traceability | A traceable batch record normally links raw materials, production date, lot number, test results, packaging, and release approval. | Batch number, manufacturing date, retest or expiry information where applicable, and certificate of analysis. | The lot number on the container should match the certificate and shipping documents. |
| Quality Management | A documented quality system may include supplier qualification, change control, deviation handling, corrective actions, and complaint management. | ISO 9001 describes quality-management-system requirements; ISO/IEC 17025 covers competence requirements for testing and calibration laboratories. | Ask whether testing is performed internally or by an external laboratory and verify the scope of any laboratory accreditation. |
| Safety Data and Hazard Communication | Safety information normally covers classification, hazards, composition, first aid, firefighting, accidental release, handling, storage, exposure controls, and disposal. | Globally Harmonized System of Classification and Labelling of Chemicals (GHS) and a 16-section Safety Data Sheet. | Use the SDS version required by the destination market and confirm that labels, pictograms, signal words, and hazard statements are consistent. |
| European Union Compliance | Chemical substances placed on the European Union market may require assessment under REACH and classification, labelling, and packaging under CLP. | REACH Regulation (EC) No 1907/2006 and CLP Regulation (EC) No 1272/2008. | Determine whether registration, exemption, importer obligations, or downstream-user communication applies to the specific substance and volume. |
| United States Compliance | Chemical substances may be subject to inventory, reporting, notification, and restriction requirements in the destination jurisdiction. | The Toxic Substances Control Act, OSHA Hazard Communication Standard, and applicable transport regulations. | Check inventory status, intended use, hazard classification, import responsibilities, and state-level requirements before shipment. |
| Packaging and Labelling | Packaging may include glass bottles, plastic containers, metal cans, lined bags, or other compatible formats selected according to chemical properties. | Container compatibility assessment, tamper evidence where required, GHS label elements, lot identification, and net quantity. | Verify compatibility with corrosive, oxidizing, volatile, light-sensitive, hygroscopic, or moisture-sensitive materials. |
| International Transport | Transport classification can include UN number, proper shipping name, hazard class, packing group, and marine-pollutant status. | UN Model Regulations, International Maritime Dangerous Goods Code, and applicable air-transport dangerous-goods rules. | Confirm the correct transport classification and documentation before booking air, sea, road, or multimodal freight. |
| Buyer Documentation Package | A standard package may include quotation, product specification, certificate of analysis, SDS, packing list, commercial invoice, and transport documents. | Additional documents may include origin statements, non-animal-origin declarations, allergen statements, residual-solvent data, or compliance declarations when relevant. | Agree on document language, revision date, signature requirements, electronic format, and document delivery timing before order confirmation. |
Note: Specifications, regulatory obligations, packaging requirements, and test methods vary by chemical substance, grade, application, destination market, and shipment quantity.
China Top Chemical Reagent Supplier for Global Buyers
Packaging, Documentation, and Global Shipping
Reliable chemical reagent exports begin with packaging that matches the product, route, and destination. Inner containers should resist leakage, pressure changes, and moisture. Many shipments use sealed bottles, cushioning material, and strong outer cartons. Sensitive reagents may need light protection or controlled temperatures. Small details matter. A damaged label can delay clearance.
Professional suppliers prepare complete documentation before collection. Typical files include the commercial invoice, packing list, certificate of analysis, safety data sheet, and certificate of origin when required. Product names, concentrations, batch numbers, and net weights must match across every document. Importers should also confirm tariff codes and local registration rules. Guessing creates expensive problems.
Global shipping requires careful coordination with carriers and customs brokers. The supplier should verify destination restrictions, transport conditions, and delivery terms before dispatch. Tracking information should be shared promptly, with updates when delays occur. Some packaging choices can increase freight costs, but weak packaging creates greater risk. No process is perfect. A final document review still deserves human attention, even after automated checks. Clear communication builds trust between the supplier, logistics team, and buyer.
China accounted for about 41% of global chemical sales in 2023, according to Cefic’s 2024 Facts and Figures report. This scale attracts international reagent buyers. Yet production volume does not prove supplier reliability. Buyers examine purity data, batch consistency, traceability, and technical support before discussing price. A clear certificate of analysis should show test methods, detection limits, lot numbers, and release dates.
Quality systems also matter. The ISO Survey 2022 recorded more than 1.2 million ISO 9001 certificates worldwide, with China among the largest national contributors. However, certification is only a starting signal. During supplier audits, experienced purchasers often compare sample results with independent laboratory tests. They also review packaging photographs, storage conditions, shipment records, and responses to technical questions. Safety Data Sheets should match the supplied material and follow the destination market’s requirements. Regulatory assumptions can become expensive mistakes.
Tips: Request two recent batches. Check whether results remain stable. Ask for an electronic traceability sample. Confirm export documents before payment. Do not accept vague answers about uncertainty or shelf life. A low quotation may hide weak testing capacity. I have seen supplier evaluations focus too heavily on price, while overlooked details later caused delays. Some buyers also expect instant answers across time zones, which is not always realistic. Set response times in writing, and verify them with a small technical trial.
Sources: Cefic, Facts and Figures 2024; ISO, The ISO Survey of Management System Standard Certifications 2022.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

