


A Carding Machine is one of the most important machines in modern textile production. It opens, cleans, and aligns loose fibers before spinning begins. Inside the machine, fast-moving cylinders carry fibers across fine metallic wire clothing. Smaller rollers remove unwanted particles, while the doffer gathers the processed fibers into a soft, continuous web. That web later becomes a sliver for drawing and spinning.
Dr. William Oxenham, a respected textile engineering researcher, has emphasized the familiar industry view: “Carding is the heart of spinning.” The phrase is simple, but it reflects the machine’s influence on yarn quality. Poor carding can create neps, uneven fiber distribution, and weak sections in the final yarn. Careful carding improves consistency.
The details matter. Operators monitor cylinder speed, feed rate, flat settings, and waste levels. They also inspect wire clothing for wear. A damaged surface may leave visible defects, even when the machine appears to run normally. It is not magic.
Different fibers demand different settings. Cotton, wool, and synthetic fibers do not respond identically. Moisture, staple length, and fiber cleanliness also change performance. Modern systems use sensors and automated controls, yet human judgment remains important. A machine can report stable numbers while producing material that feels wrong.
This guide explains what a Carding Machine does, how its main parts interact, and why operating conditions affect textile quality. It also considers practical limitations, because no carding system performs perfectly without maintenance, adjustment, and informed supervision.
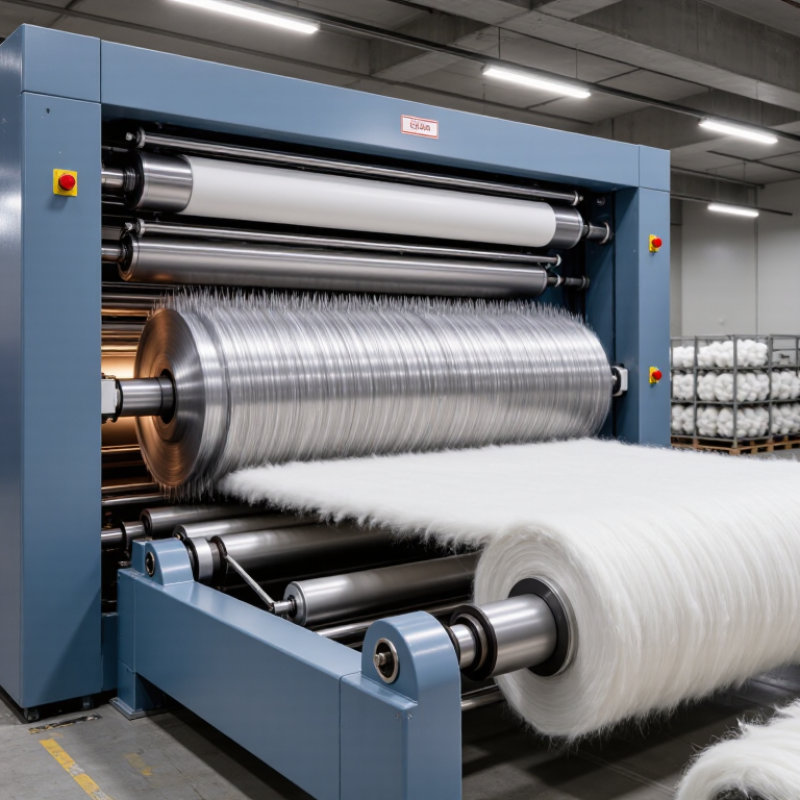
A carding machine is a textile machine that prepares loose fibers for spinning. It opens compacted material, separates tangled strands, and arranges them into a more even layer. Raw fiber enters through a controlled feed system. Inside, a large rotating cylinder carries the fibers across fine metallic surfaces. Smaller rollers, called flats or workers, guide this movement. Their teeth separate clumps without cutting the fibers when settings are correct. The machine can also remove dust, short fibers, and small impurities. The cleaned fibers form a thin, continuous web. That web looks fragile.
A doffer collects the web and condenses it into a soft strand called sliver. The sliver then moves toward later drafting and spinning processes. Operators adjust feed speed, roller spacing, cylinder speed, and wire condition. These settings depend on fiber length, moisture, and the required yarn quality. In practical mill work, small changes can affect evenness and waste. Excessive speed may create broken fibers or irregular sliver. Insufficient cleaning can leave neps and unopened bundles. Regular inspection matters, especially around wire clothing and suction points. Experienced technicians still review samples because machine readings do not reveal everything. A carding machine is highly precise, but it is not self-correcting. Some fiber blends behave unpredictably. Careful testing remains necessary.

A carding machine separates, opens, and aligns textile fibers before spinning. The licker-in opens compressed fiber tufts, the cylinder carries fibers through the carding zone where they are disentangled and aligned, and the doffer gently removes the formed fiber web. The chart shows representative operating-speed ranges commonly used for these main components; exact settings vary according to fiber type, machine design, and production requirements.
A carding machine turns a compressed mat of fibers into a more uniform web or sliver. Its work depends on controlled opening, cleaning, alignment, and blending. The feed roller presents fibers at a steady rate. A taker-in opens the material and removes larger impurities. The main cylinder carries fibers across its surface at high speed. Flat bars help separate tangled fibers and improve alignment. The doffer then collects the prepared fiber layer. A stripping roller transfers it toward the delivery system.
Several supporting parts keep this sequence stable. Airflow removes loose dust and helps control fiber movement. Sensors monitor feed pressure, speed, and web thickness. The coiler guides the sliver into a can with regular coils.
Small changes matter. Excessive cylinder speed can damage delicate fibers. Too much suction may disturb the web. Insufficient cleaning can leave visible neps or uneven patches.
Experienced operators adjust settings according to fiber length, moisture, and contamination level. A setting that works for cotton may perform poorly with synthetic fibers. No adjustment is universally correct, and this is where simple explanations become misleading. Operators inspect the web, listen for unusual vibration, and compare output thickness during production. These practical checks often reveal problems before instruments show a clear warning. Even then, judgment is imperfect and should be supported by maintenance records and measured test results.
A carding machine begins with a controlled fiber feed. A feed chute delivers small tufts onto a moving apron. The apron keeps the material level and prevents sudden loading. This matters because uneven feeding creates thick places in the final sliver.
Inside the machine, a large cylinder carries fine metallic wire points. Smaller rollers open compressed tufts as their surfaces move at different speeds. The wire points separate fibers, remove some trash, and improve fiber alignment. A slow, steady transfer is essential. Too much pressure can damage fragile fibers.
The cylinder then presents the fibers to worker rollers and stationary flats. These surfaces gently comb the mass. They do not make every fiber perfectly parallel. That is an important limitation. The doffer removes the organized fiber web and forms it into a continuous sliver.
Textile Exchange reported global fiber production at about 124 million tonnes in 2023. Its 2024 Materials Market Report projects roughly 160 million tonnes by 2030. Such growth increases the need for stable preparation equipment and measurable process control. Yet production volume alone does not prove quality.
Experienced operators still inspect the feed surface, wire condition, waste level, and sliver evenness. Small changes in moisture or fiber length can alter the opening action. The machine may look clean and balanced, but hidden wear can remain. That is where routine testing becomes more reliable than visual judgment.
What Is a Carding Machine and How Does It Work?
How Carding Aligns, Cleans, and Separates Fibers
A carding machine prepares loose textile fibers for spinning. Its main task is controlled disentangling. Feed rollers deliver a thin, even layer to a rapidly rotating cylinder covered with fine wire points. These points open fiber tufts and spread them across the working surface. Smaller rollers and stationary flats help remove knots, dust, and short fiber fragments. The process looks simple, but precise adjustment matters.
Carding also improves fiber alignment. As the cylinder carries the fibers forward, the doffer gently collects them into a soft, continuous web. This web becomes a sliver after passing through a condenser and guiding system. Longer fibers tend to remain in the main flow, while heavier impurities and loose fragments separate through carefully designed clearances. Air movement assists cleaning, but excessive airflow can disturb the web.
The result is cleaner, more parallel material for later drafting and spinning. Operators usually check sliver thickness, fiber uniformity, waste levels, and surface appearance. They may adjust cylinder speed, feed rate, moisture, or the distance between wire surfaces. Small changes can affect strength and evenness. Not perfectly uniform.
In practice, carding is a balance rather than a single ideal setting. Fibers with different lengths, fineness, or moisture levels respond differently. A setting that works well for one batch may create too much waste in another. Regular inspection remains essential. Experience helps, but measured testing should guide final decisions.
Key operating stages, machine sections, fiber actions, and typical process parameters
| Process Area | Main Machine Element | Primary Fiber Action | Typical Operating Information | Result |
|---|---|---|---|---|
| 1. Fiber Feeding | Feed lattice and feed roller | Meters the fiber tufts into the carding zone at a controlled rate. | Feed rate is adjusted according to fiber type, required production, and web quality. | A consistent, manageable fiber batt enters the machine. |
| 2. Opening and Transfer | Licker-in, taker-in, or opening roller | Opens tufts and transfers fibers from the feed section to the main cylinder. | Roller surfaces are fitted with metallic wire clothing; higher surface speeds increase opening intensity. | Large tufts are reduced and fibers are more evenly distributed. |
| 3. Intensive Carding | Main cylinder and carding flats | Separates, straightens, and partially aligns individual fibers through opposing wire points. | Cylinder speed, flat setting, wire angle, and cylinder-to-flat spacing strongly affect fiber quality. | Fibers become more individualized, parallel, and evenly dispersed. |
| 4. Trash and Neps Removal | Cylinder, flats, mote knives, and suction system | Removes seed fragments, leaf particles, dust, short fiber clusters, and some neps. | Cleaning efficiency depends on fiber preparation, wire condition, airflow, and machine settings. | Cleaner fiber with fewer visible impurities and fiber clusters. |
| 5. Fiber Alignment | Cylinder-to-doffer transfer zone | Transfers fibers from the fast-moving cylinder to the slower doffer while preserving a predominantly longitudinal orientation. | The relative speeds and surface clothing of the cylinder and doffer influence web formation. | A thin, continuous web of partially aligned fibers is formed. |
| 6. Web Formation | Doffer and doffer comb | Strips the fiber web from the doffer surface. | Doffer speed and stripping action affect web uniformity and fiber transfer. | A uniform web is delivered for condensation or further drafting. |
| 7. Condensation and Delivery | Web condenser, trumpet, or sliver-forming unit | Gathers the web into a narrow strand without substantially changing its mass. | The delivered product is commonly called card sliver in staple-spinning processes. | A continuous sliver is deposited into a can for subsequent processing. |
| 8. Waste and Air Management | Waste knives, filters, ducts, and suction fans | Separates waste and airborne dust from useful fibers and transports it to collection points. | Airflow must be balanced to avoid excessive fiber loss or inadequate cleaning. | Controlled waste removal and a cleaner operating environment. |
| Indicator | Common Reference Range or Description | Why It Matters |
|---|---|---|
| Card sliver linear density | Often approximately 3–6 ktex in conventional staple-spinning preparation; the selected value depends on the process and fiber material. | Determines the mass delivered to the next drafting stage. |
| Production rate | Varies widely by machine design, fiber, product quality, and settings; modern high-capacity cards may process several hundred kilograms per hour. | Higher output can increase productivity but may require tighter control of cleaning and uniformity. |
| Fiber individualization | Assessed by the reduction of unopened tufts and the uniformity of the resulting web or sliver. | Good individualization supports even drafting and more consistent yarn formation. |
| Cleaning efficiency | Depends on the incoming bale preparation, fiber contamination, wire clothing, airflow, and waste settings; it is not a fixed universal percentage. | Excessive cleaning may remove useful fibers, while insufficient cleaning leaves impurities in the product. |
| Sliver evenness | Typically monitored with mass-variation testing, including short-, medium-, and long-term unevenness. | Uneven sliver can create yarn count variation and visible fabric defects. |
| Fiber damage and short-fiber generation | Controlled by minimizing excessive mechanical action, incorrect settings, worn clothing, and unsuitable feed conditions. | Lower fiber damage generally improves spinning efficiency and yarn strength. |
A carding machine opens, cleans, and aligns textile fibers before producing a thin web or a continuous sliver. The collection stage determines whether this material remains even, stable, and ready for later processing. Small changes in feed rate, moisture, or cylinder settings can affect the final quality.
For sliver production, the doffer removes the fiber web from the main cylinder. A stripping roller guides the web toward a condenser, where the fibers gather into a soft, rope-like strand. The strand then passes through a trumpet and enters a rotating can. The coiler places it in smooth, overlapping coils, preventing sharp bends and unnecessary stretching. The can should fill evenly. It should not form high ridges or loose nests.
For a finished web, the doffer may transfer the web onto a moving conveyor instead. Air movement and surface speed must remain steady. The web can then be cross-lapped, layered, or bonded, depending on its intended use. Operators usually check web width, visual uniformity, fiber clumps, and edge stability during collection. Uneven edges often reveal problems earlier than the center.
In practice, settings are rarely perfect. Even experienced operators need to adjust them. Static electricity can disturb a delicate web, while excessive tension can thin the sliver. Regular inspection, clean collection surfaces, and careful handling improve consistency. The material should feel cohesive, but not compressed. That balance takes attention.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

