


Choosing the best rotorcomp air ends from China requires more than comparing catalog prices. The right choice depends on compressor design, operating pressure, airflow demand, and maintenance expectations. A workshop may need a compact oil-injected air end for general manufacturing. A chemical plant may require stronger sealing, stable discharge temperatures, and documented material control. These applications are not interchangeable.
Experienced buyers usually examine the rotor profile, bearing arrangement, oil injection system, and rated speed. They also check performance data under defined test conditions. Look for airflow, pressure, power consumption, noise, vibration, and temperature figures. Clear documentation matters. So does traceability.
Ask the supplier for serial-number records, dimensional drawings, factory test reports, and compatibility details. Confirm whether the unit is genuinely manufactured in China or supplied by a trading company. A reliable producer should explain service intervals, lubricant requirements, shaft rotation, and installation limits without avoiding technical questions. Factory audits, sample testing, and independent inspection can strengthen confidence. They cannot remove every risk.
The best rotorcomp air ends are not always the cheapest models. They should deliver consistent compression, practical efficiency, and dependable support after delivery. Warranty terms deserve careful review. Spare bearings and seals should be available locally or within a realistic shipping period. A polished brochure is not proof of performance. No shortlist is perfect. Specifications may also change between production batches, so buyers should verify the final unit before purchase. This guide compares important technical and commercial factors, helping engineers make a more informed decision when sourcing rotorcomp air ends from China.
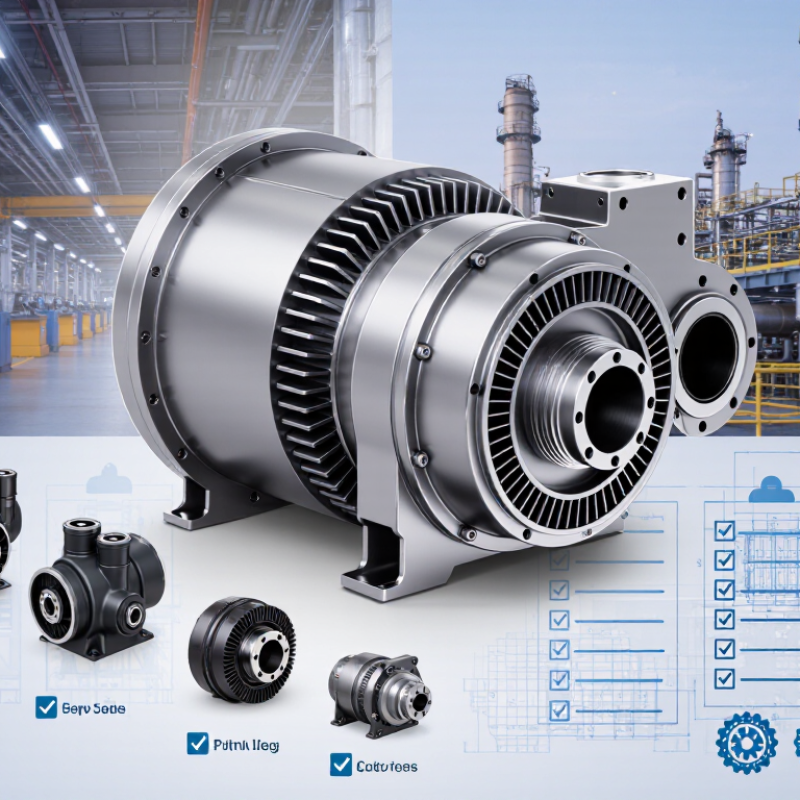
A rotorcomp air end is the compression core of a rotary screw compressor. It contains matched male and female rotors inside a sealed housing. Unlike a complete compressor, it has no motor, receiver, or control cabinet. Its job is direct: draw in air, compress it, and deliver a steady flow. In practical maintenance, technicians judge it by stable pressure, low vibration, and limited oil carryover. Small details matter.
The core design normally uses twin helical rotors inside a precisely machined housing. As the rotors turn, air fills the grooves between their teeth. The trapped volume then shrinks along the rotor length, raising pressure. Timing, sealing clearances, bearing support, and surface finish all affect efficiency. Too much clearance wastes energy. Too little clearance can create heat or contact damage. Oil-injected designs use oil for sealing and cooling. Oil also reduces wear. The separation system must remove oil before discharge.
When comparing air ends made in China, buyers should inspect rotor profile data, material reports, dimensional tolerances, and test records. A test sheet is useful, but it is not complete proof. Witnessing a running test can reveal abnormal noise, unstable temperature, or excessive vibration. Check sound during startup and after reaching working pressure. A real weakness is often hidden there. I would not select an air end solely because its price is attractive. Service access, replacement bearing quality, machining consistency, and technical support can matter more over several years. Sometimes a cheaper unit creates a larger maintenance bill. That tradeoff deserves careful review.

Rotorcomp air ends are compressor core assemblies that compress air through precisely matched rotors, bearings, seals, and a housing. The chart shows representative working-pressure ranges for common rotary air-end designs.
Oil-injected twin-screw air ends are widely used for general industrial compressed air because they offer a broad pressure range and continuous operation. Oil-free twin-screw designs reduce oil contamination but usually require more advanced sealing and cooling systems. Single-screw air ends can provide stable compression with a compact structure. Actual pressure ratings depend on rotor profile, speed, cooling method, materials, and the complete compressor package.
What Are the Best Rotorcomp Air Ends from China?
Key Factors for Evaluating Rotorcomp Air Ends from China
Choosing a Chinese-made air end requires more than comparing catalog prices. Start with the operating profile: required pressure, airflow, speed, oil temperature, and annual running hours. A unit rated for 7 bar may perform poorly when operated near its limit continuously.
Inspect the rotor design and machining quality closely. Accurate rotor profiles, stable clearances, and balanced shafts directly affect efficiency and vibration. Ask for factory test data, including specific power, discharge temperature, noise, and leakage results. ISO-based quality procedures are useful, but actual test records matter more. A clean report with serial traceability is reassuring.
Material selection deserves attention. Check bearing specifications, seal construction, housing strength, and oil compatibility. Request inspection records for critical components. Experienced suppliers should explain maintenance intervals without avoiding difficult questions. They should also provide installation guidance, spare-part lists, and a realistic warranty process.
Do not trust appearance alone. A polished datasheet can hide inconsistent production. I would compare several samples under similar loads, then review vibration readings after extended operation. This takes more time, but short testing can miss thermal drift or unusual noise. Some evaluations also overlook local service capability, which may become expensive later. The best choice is not always the cheapest unit; it is the air end with verified performance, dependable documentation, and support that remains responsive after delivery.
| Evaluation Dimension | Recommended Benchmark or Data Point | Why It Matters | How to Verify | Suggested Weight |
|---|---|---|---|---|
| Rated discharge pressure | Select an air end whose continuous operating range covers the required system pressure, commonly 7.5, 8, 10, or 13 bar(g) in general industrial applications. | Operating outside the intended pressure range can increase power consumption, temperature, leakage, and mechanical stress. | Review the performance map, pressure ratio, maximum continuous pressure, and test conditions. | 15% |
| Free air delivery | Compare capacity at the same inlet temperature, inlet pressure, discharge pressure, rotational speed, and measurement standard. Do not compare nominal displacement alone. | Actual delivered air depends on internal leakage, clearances, speed, pressure ratio, and test conditions. | Request a test report or performance curve based on ISO 1217 or an equivalent recognized acceptance-test method. | 15% |
| Specific power | Use the complete compressor package value in kW per m³/min or kW per 100 cfm at the required pressure; a lower value is preferable when measured under identical conditions. | Energy normally represents the largest portion of lifetime compressor cost. | Check whether the quoted power includes the motor, oil pump, cooling fan, separator losses, and transmission losses. | 18% |
| Rotor profile and efficiency | Prioritize a modern asymmetric twin-screw profile with controlled clearances and documented volumetric and adiabatic efficiency data. | Rotor geometry influences leakage, compression efficiency, noise, discharge temperature, and service life. | Ask for rotor drawings, efficiency curves, machining tolerances, and inspection records without relying only on marketing descriptions. | 10% |
| Bearing arrangement and service life | Verify bearing type, rated load, lubrication method, design life, and replacement procedure. The specification should identify bearings by standardized technical designation. | Bearing condition directly affects vibration, rotor alignment, efficiency, and the risk of catastrophic failure. | Request bearing calculations, vibration limits, oil-quality requirements, and documented failure-analysis procedures. | 10% |
| Oil-injected or oil-free design | Match the air-end design to the required air purity. Oil-injected elements require an oil separator and downstream filtration; oil-free designs require stricter coating, sealing, and temperature control. | The wrong technology can cause product contamination, unsuitable maintenance costs, or inadequate air quality. | Define the required ISO 8573-1 air-quality class and review oil carryover or certification test results. | 8% |
| Discharge temperature | Confirm the maximum continuous discharge temperature at the specified pressure ratio, ambient temperature, oil type, and cooling arrangement. | Excessive temperature accelerates oil oxidation, damages seals, reduces lubricant life, and increases the risk of shutdowns. | Review thermal test data, temperature alarm settings, cooling requirements, and recommended oil-change intervals. | 8% |
| Noise and vibration | Use measured sound-pressure or sound-power data and vibration limits rather than a general statement such as “low noise.” | Noise and vibration affect operator safety, installation requirements, bearing life, and the reliability of connected equipment. | Request test conditions, microphone distance, acoustic weighting, rotational speed, and vibration measurement locations. | 6% |
| Material and surface treatment | Check rotor, housing, shaft, seal, and coating materials for compatibility with the lubricant, humidity, temperature, and duty cycle. | Material selection affects corrosion resistance, wear, dimensional stability, and long-term clearances. | Request material certificates, hardness data, coating specifications, and corrosion or wear-control procedures. | 5% |
| Manufacturing and quality control | Prefer suppliers with documented dimensional inspection, rotor balancing, cleanliness control, traceability, and final pressure or performance testing. | Consistent manufacturing reduces variations in efficiency, noise, leakage, and operating life between batches. | Audit quality records and request sample inspection reports, calibration records, and nonconformance procedures. | 7% |
| Maintenance and spare parts | Confirm availability of bearings, seals, gaskets, oil-separator components, service kits, technical manuals, and recommended torque values. | Shorter parts lead times can reduce downtime and make lifecycle cost more predictable. | Obtain a written parts list, normal lead times, warranty terms, service intervals, and local technical-support details. | 10% |
| Documentation and compliance | The technical file should include datasheets, drawings, operating limits, installation instructions, test results, and applicable conformity documents. | Clear documentation supports safe integration, acceptance testing, maintenance, and regulatory review. | Check consistency between the quotation, nameplate, drawings, test report, and delivered unit. | 6% |
| Total Evaluation Weight | 100% | |||
Note: Performance values should only be compared when the inlet conditions, discharge pressure, rotational speed, lubricant, cooling method, and measurement standard are identical.
China’s leading rotary-screw air-end manufacturers generally fall into three groups: integrated compressor factories, precision machining specialists, and export-focused OEM suppliers. Their product ranges often include oil-injected twin-screw air ends, oil-free designs, compact low-pressure units, and high-pressure models. Oil-injected types remain popular because they offer strong efficiency and simpler maintenance. Oil-free air ends suit food, pharmaceutical, and electronics production, where lubricant carryover creates serious quality concerns.
The U.S. Department of Energy reports that compressed-air systems may consume around 10% of industrial electricity. Its guidance also notes that leaks can waste 20–30% of compressor output. These figures make air-end efficiency more important than a low purchase price. When evaluating Chinese manufacturers, request measured flow, shaft power, pressure ratio, rotor profile, bearing specifications, and test conditions. ISO 1217 performance testing adds useful credibility. However, factory claims are not always perfectly comparable. I would still verify results through independent testing.
Tips: Check machining tolerances, coating quality, lubrication channels, spare-part availability, and warranty response times. Ask for a complete performance curve, not one attractive efficiency figure. A reliable supplier should explain noise, vibration, oil separation, and service intervals clearly. If documentation feels incomplete, pause before ordering. Small gaps often become expensive problems after installation.
Chinese rotary-screw air ends should be judged by measured performance, compatibility, and quality control—not price alone. The U.S. Department of Energy’s Improving Compressed Air System Performance sourcebook reports that leaks can waste 20–30% of compressed air output. That makes real-world efficiency more important than attractive catalog claims. Ask for ISO 1217 test results, including free air delivery, shaft power, discharge pressure, and operating temperature.
Compatibility requires careful field checking. Confirm the rotor speed, shaft dimensions, rotation direction, oil type, inlet valve, discharge port, coupling, and controller signals. A small mismatch can create vibration, poor loading, or premature bearing wear. ISO 8573-1 classifications also matter when the air serves food, electronics, or clean manufacturing. The air end alone cannot guarantee the required air purity.
Quality is visible in details. Check rotor machining records, bearing origin, balancing reports, serial traceability, and pressure-test documentation. In my experience, suppliers with clear inspection records are easier to evaluate after installation. However, documentation can still be incomplete or overly polished. I would request a witnessed performance test.
Listen for uneven noise.
A practical comparison should include energy use after warm-up, oil carryover, temperature stability, and service access. The U.S. Department of Energy recommends leak management and system measurement because operating conditions often differ from factory testing. A lower-priced unit may perform well, but only if its tolerances, lubrication system, and replacement parts match the existing package. That uncertainty deserves honest review.
Selecting and sourcing a quality air end in China starts with your compressor’s working conditions.
Confirm air delivery, operating pressure, speed range, cooling method, and oil-injection requirements. A mismatch may cause overheating, unstable output, or premature bearing wear. Ask suppliers for dimensional drawings, material specifications, and performance data tested at your required conditions.
Practical experience shows Samples reveal more than polished catalog pages. Request one sample and inspect machining, shaft rotation, sealing surfaces, and mounting accuracy. Review test records, inspection procedures, and traceability for critical components. A reliable manufacturer should explain bearing selection, rotor balancing, lubrication paths, and expected service intervals clearly. Factory video calls help, but an independent inspection is stronger evidence.
Compare suppliers by total risk, not only unit price. Check production capacity, export experience, packaging protection, replacement procedures, and communication speed. Clarify delivery terms and confirm every tolerance in writing. Some suppliers may promise impressive efficiency without stating test temperature or pressure. That deserves a second question. I would also allow extra time for sample revisions, because the first design is rarely perfect. A small mismatch in a coupling or flange can delay an entire assembly. Keep approved drawings, test results, and inspection photos in one controlled file before placing a larger order.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

