Who Is the Best Hydrogenated Resin Supplier in China?
Choosing the best Hydrogenated Resin supplier in China requires more than comparing price lists. A clear melt can look impressive in a sample jar. Performance still depends on resin chemistry, compatibility, softening point, color stability, and consistency between batches. Small differences matter.
Industry reports help explain the market, but they do not crown a single supplier. Grand View Research’s Adhesives and Sealants Market analysis and MarketsandMarkets’ Tackifier Market report examine demand across applications and regions. Their market context is useful; neither should replace product testing or supplier audits. For buyers, technical data sheets, representative samples, and documented quality controls provide more relevant evidence.
Adhesive-technology author D. Satas offers a useful framework in Handbook of Pressure Sensitive Adhesive Technology. Paraphrasing his formulation-focused approach: “Compatibility must be verified in the finished system, not assumed from a datasheet.” That is a practical warning, not a supplier endorsement. A resin that works well in one adhesive may perform differently in another. Ask for batch records, test the material under your processing conditions, and compare aging results. A low quote can be tempting. It may also leave unanswered questions about consistency, support, and delivery. This guide evaluates Chinese suppliers through those measurable criteria, while recognizing that the right choice depends on your application. No universal winner exists.
What Is Hydrogenated Resin? Types, Feedstocks, and Industrial Uses
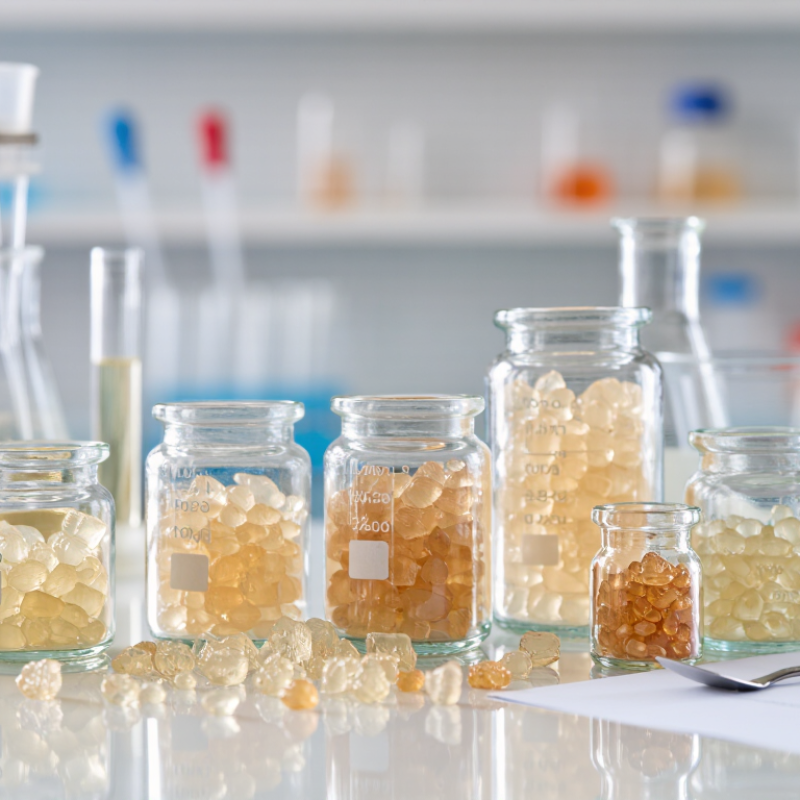
Hydrogenated resin is a tackifier used to help adhesives grip surfaces. It is made by hydrogenating Hydrocarbon Resin, reducing unsaturation in the material. This treatment generally improves color stability and resistance to heat and oxidation. That matters. Pale appearance alone, however, does not prove consistent performance.
Feedstock shapes the resin’s properties. C5-rich streams commonly produce aliphatic resins with good compatibility in many hot-melt adhesive systems. C9-rich streams can offer stronger compatibility with certain aromatic polymers. Dicyclopentadiene-based resins provide another option, often selected for their balance of tack and softening point. These categories are useful guides, not guarantees. Not quite.
In hot-melt adhesives, resin can help bond packaging seams and labels at practical application temperatures. Pressure-sensitive tapes and labels use it to balance initial tack with clean removal. Some coatings and printing inks also use hydrogenated resins to improve adhesion or gloss. Small formulation changes can alter results, so trial data matters. When assessing a supplier, request batch specifications, softening-point data, color values, and application testing. I would not treat a single sample as proof of long-term consistency; production lots can vary.
Hydrogenated Resin: Typical Softening-Point Ranges by Resin Family
Representative commercial-grade ranges in °C. Hydrogenated C5 and C9 resins are made from petroleum-derived feedstocks; DCPD resins use dicyclopentadiene. These resin families are used in applications such as hot-melt adhesives, pressure-sensitive adhesives, and sealants.
Ranges are indicative, not universal specifications. Actual properties vary by grade and manufacturer; this chart compares resin types, not suppliers.
Which Specifications Matter? 90–140 °C Softening Points and Gardner Color
A 90–140 °C softening-point range covers many hydrogenated resin grades, but it does not identify the right one by itself. The lower end may suit formulations needing easier flow or lower processing temperatures. Higher points can help retain firmness in warmer conditions. Check the intended use before comparing supplier data. A number without context is thin evidence.
Gardner color helps assess resin appearance, especially in light-colored adhesives and coatings. Lower Gardner readings generally indicate a lighter resin, but comparisons only work when the test method and sample preparation match. Ask for recent batch results, not just a typical value. That distinction matters. A pale sample can still perform poorly if it is incompatible with the base polymer.
Review the certificate of analysis for softening point, Gardner color, and batch variation. Also ask how each value is measured, and whether the supplied sample represents routine production. Small differences add up. It is easy to focus too much on one attractive specification; I would reconsider that approach when odor, compatibility, or color stability also affects the finished product. A trial batch can reveal issues a data sheet cannot.
How Are Chinese Suppliers Compared? ASTM E28 Testing and Quality Consistency
Comparing Chinese hydrogenated resin suppliers requires more than checking a softening-point number. Ask whether ASTM E28 is suitable for the specific resin grade. Then confirm the supplier uses a consistent ring-and-ball procedure, calibrated equipment, and documented sample conditioning.
Small details matter. A thermometer offset or uneven heating can shift results and complicate comparisons between batches.
Request certificates of analysis from several production lots, not just one polished sample. Compare softening point alongside color, melt viscosity, and agreed specification limits. Look for repeatability across batches, clear test dates, and traceable records.
If possible, review how the supplier handles an out-of-range result and whether a retained sample can be retested. These checks reveal more than a single pass-or-fail figure. Be cautious with unusually narrow claims unless the testing conditions are stated.
One limitation: ASTM E28 results alone cannot prove performance in every adhesive or coating formulation. A practical evaluation may still require application-specific trials. Good documentation helps, but it does not replace them.
How Should Buyers Verify a Supplier? Samples, Batch Data, and Compliance Records
Who Is the Best Hydrogenated Resin Supplier in China?
When evaluating a hydrogenated resin supplier in China, treat verification as a documented process, not a polished sales call. Ask for a sample from a clearly identified production batch. Request its certificate of analysis, including the tested values and methods for softening point, color, and melt viscosity. Small variations can affect coating flow or adhesive performance. Keep the record.
Compare the sample with the technical limits your process actually needs. Check that the batch number on the label matches the accompanying data. A certificate with no test date or method leaves important questions open. Ask for retained-sample or retesting procedures, too. A tidy spreadsheet can still miss a mismatch between sample and shipment; it is worth checking.
Review the safety data sheet and other compliance documents relevant to your destination market and application. Confirm revision dates, product identifiers, and the supplier’s traceability process. Match the documents to the exact resin grade, not just a product family. If a supplier cannot explain an unusual result or provide a clear correction, pause before approving a larger order. Independent testing may help when specifications are critical. Lab results can differ, so record the test conditions alongside them.





