


Choosing the right Hardening Oven is rarely a simple temperature comparison. Global buyers must examine heating uniformity, atmosphere control, workload size, quench integration, energy use, and after-sales support. A bright steel fixture may look ready outside while its core remains under-hardened. That hidden variation can increase rejects, distortion, and warranty risk.
Industry data explains why efficiency matters. The International Energy Agency reports that industry consumes about 37% of global final energy. Heat-treatment equipment therefore deserves close energy analysis, not only purchase-price evaluation. MarketsandMarkets also identifies automation, process monitoring, and energy efficiency as important directions across the industrial furnace market. These trends affect oven selection, especially for manufacturers operating several shifts or multiple sites.
This guide reviews seven Hardening Oven options for international buyers. It considers operating temperature, usable chamber volume, temperature uniformity, control systems, atmosphere safety, maintenance access, and documented test results. ISO 13577 provides a useful reference for industrial furnace safety, while AMS2750 remains influential in aerospace heat-treatment quality systems. Local electrical, emissions, and workplace requirements still require verification.
No ranking is universal. A compact batch oven may suit toolmakers, yet fail a high-throughput automotive line. A premium model may offer better controls, but its spare parts network could be weak in a distant market. That point is easy to overlook. Specifications also need independent confirmation, because published efficiency figures may reflect ideal laboratory conditions rather than a loaded production cycle. The comparisons below aim to support practical, evidence-based decisions, while acknowledging that installation quality and operator discipline can change real-world results.
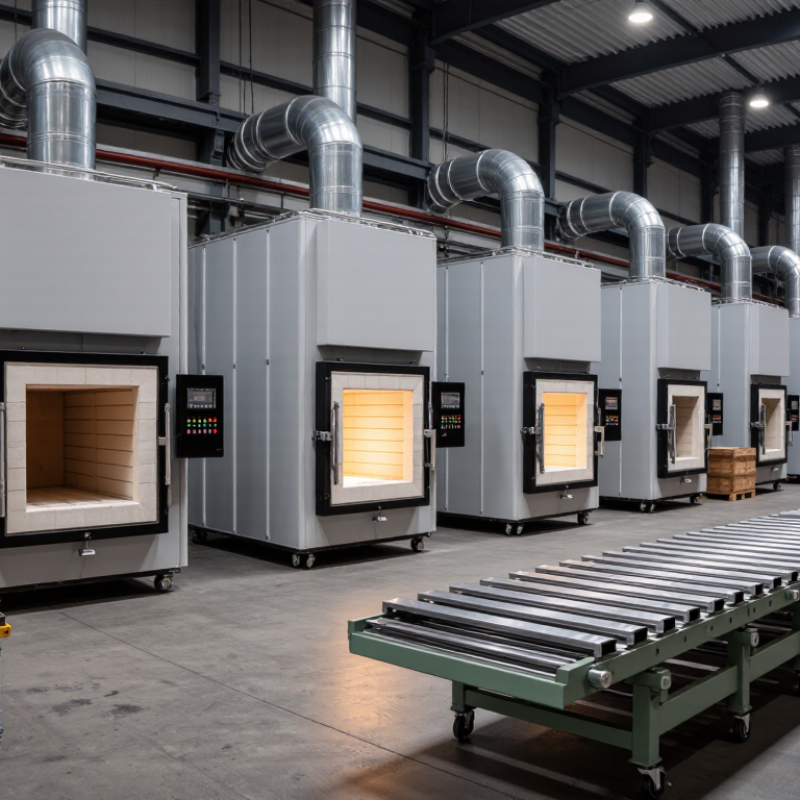
A hardening oven heats steel parts to a controlled austenitizing temperature before quenching. This changes the metal’s internal structure and improves hardness, strength, and wear resistance. Many systems also support tempering, which reduces brittleness after hardening. The process sounds simple. It is not.
In industrial production, hardening ovens treat gears, shafts, springs, cutting tools, fasteners, and machine components. A typical cycle may require temperatures near 800–950°C, depending on the alloy and required properties. Uniform heat matters. A cold corner can create uneven hardness across a batch. Practical buyers should request temperature mapping, load data, chamber dimensions, and recorded cycle results.
Global buyers should examine insulation quality, heating-element access, atmosphere control, cooling arrangements, and electrical compatibility. Local voltage and safety requirements can affect installation more than expected. Clear manuals, spare-part availability, operator training, and service response also show supplier reliability. Do not judge an oven only by its maximum temperature.
A sound inspection includes empty-chamber testing and loaded trials. Place sensors near the door, center, and rear wall. Compare the readings carefully. One overlooked detail is door sealing; small leaks may waste energy and disturb the process atmosphere. Even experienced teams can accept impressive specifications too quickly. A perfect display reading may still hide poor uniformity, slow recovery, or inconsistent results between batches.

Choosing among the seven best hardening ovens requires more than comparing advertised temperatures. Temperature uniformity is often the decisive measure. A chamber rated at 1,000°C may still create uneven results across a large load. Ask for independent temperature surveys using calibrated, traceable instruments. Check the working zone, not only the maximum rating.
Control quality matters every day. A reliable oven should record heating curves, hold times, alarms, and batch data. Recipe protection can reduce operator mistakes. Atmosphere control is equally important when oxidation affects surface hardness. Review gas flow stability, door sealing, exhaust design, and sensor placement. Small leaks become costly over many cycles.
Global buyers should compare electrical compatibility, insulation performance, maintenance access, and local technical support. Energy use per batch gives a clearer comparison than heater wattage alone. Safety systems should include over-temperature protection, emergency shutdowns, and clear operating procedures. Confirm conformity with applicable regional requirements before purchase. A practical factory acceptance test can expose weak airflow or slow recovery. Yet no test predicts every production condition. Load shape, spacing, and operator habits can change results. That uncertainty deserves attention. The best choice balances validated performance, serviceability, total ownership cost, and documented reliability, rather than selecting the lowest initial price.
Seven Leading Hardening Oven Options for Global Buyers
Global buyers can compare seven practical hardening oven options for different production needs. Electric box ovens suit small batches and provide clean, stable heating. Gas-fired chamber ovens often reduce operating costs where fuel is accessible. Continuous conveyor ovens support high-volume parts with repeatable cycle times. Pit ovens handle long components, heavy loads, and vertical loading. Vacuum hardening ovens limit oxidation and help protect precise surfaces. Atmosphere-controlled batch ovens use protective gases during heating. Modular heat-treatment lines combine heating, quenching, washing, and tempering in one workflow.
Each option requires careful technical review. Check temperature uniformity across the working zone, not only the controller display. Ask for documented test results at the intended operating temperature. Door seals, insulation thickness, and cooling performance affect daily energy use. A reliable supplier should provide manuals, spare-parts guidance, safety controls, and operator training. Local service coverage matters when a heating element fails during a production shift.
I would not select an oven from capacity alone. A compact chamber may outperform a larger unit when loading is uneven. It is also important to confirm electrical standards, gas requirements, ventilation rules, and conformity documents for the destination country. Some quotations appear attractive but exclude installation, calibration, or quench equipment. That creates budget surprises. Review sample parts, expected hardness, cycle records, and maintenance access before signing. Real production trials are still the strongest evidence. Forecasts can be wrong.
| Rank | Hardening Oven Option | Typical Operating Temperature | Typical Chamber Capacity | Atmosphere / Airflow | Heating Configuration | Recommended Applications | Global-Buyer Advantages |
|---|---|---|---|---|---|---|---|
| 1 | High-Temperature Box Hardening Oven | Up to approximately 1,200°C | Small laboratory size to large production chamber | Forced air or controlled atmosphere, depending on process | Electric resistance elements with insulated steel casing | Tool steel, alloy steel, dies, punches, and general heat treatment | Versatile format, simple loading, broad international availability, and straightforward maintenance |
| 2 | Forced-Convection Circulation Oven | Approximately 150–750°C | Typically 100–2,000 litres | Recirculated hot air with adjustable airflow | Electric heaters, circulation fan, and temperature-control system | Small and medium metal parts requiring consistent temperature distribution | Good temperature uniformity, adaptable power supplies, and convenient batch processing |
| 3 | Atmosphere-Controlled Hardening Furnace | Approximately 800–1,100°C | Batch chambers from compact to industrial scale | Nitrogen, argon, endothermic gas, or other specified protective atmospheres | Electric or gas heating with sealed chamber and gas-control equipment | Carbon-steel, low-alloy steel, and parts where oxidation or decarburization must be reduced | Improved surface protection and better repeatability for controlled heat-treatment cycles |
| 4 | Vacuum Hardening Furnace | Approximately 600–1,300°C, depending on design | Laboratory, tool-room, and production batch sizes | Vacuum processing followed by inert-gas quenching | Vacuum chamber, resistance heating, pumping system, and controlled gas quench | High-speed steel tools, moulds, precision dies, and high-value components | Low oxidation, clean surfaces, reduced post-treatment cleaning, and controlled distortion |
| 5 | Continuous Mesh-Belt Hardening Oven | Approximately 500–1,050°C | Throughput-based; commonly used for high-volume production | Controlled atmosphere with continuous gas monitoring | Multiple heating zones, conveyor belt, cooling, and optional quench sections | Fasteners, bearings, automotive components, and repetitive small-part production | Consistent production flow, reduced manual handling, and suitability for automated lines |
| 6 | Carburizing and Hardening Furnace Line | Approximately 850–950°C for carburizing stages | Modular batch or continuous production systems | Carbon-controlled atmosphere followed by oil, gas, or polymer quenching | Multi-zone heating, carburizing chamber, transfer system, and quench tank | Gears, shafts, transmission parts, and components requiring a hard case with a tougher core | Suitable for high-volume case hardening and integration with washing, tempering, and testing equipment |
| 7 | Salt-Bath-Compatible Hardening System | Typically up to approximately 1,000°C, depending on salt chemistry | Small to medium batch volumes | Molten salt provides direct heat transfer; ventilation is essential | Electrically heated salt pot with temperature and bath-composition controls | Tool steels, small precision parts, and applications requiring rapid heating | Fast heat transfer and compact footprint, with strict requirements for safety, waste handling, and operator training |
Note: Temperature ranges, capacities, and configurations are typical engineering ranges for these oven categories. The final specification should be confirmed against the material grade, part geometry, required hardness, atmosphere, quenching method, local electrical supply, safety regulations, and applicable quality standards.
Choosing among seven hardening oven types starts with the material, not the catalog price. Air-circulation chamber ovens suit common steels and mixed batches. Vacuum ovens protect bright surfaces and reduce oxidation, but they need stronger pumps and careful loading. Inert-atmosphere ovens help control carbon loss on sensitive alloys. Small parts may fit compact batch units. Large components often require pit or front-loading designs, with reinforced floors and multiple temperature zones.
For high-volume production, continuous belt and mesh-belt ovens provide steady throughput. They work best when part sizes and cycle times stay predictable. Frequent changeovers can waste heated space and energy. In production evaluations, load density affected temperature recovery more than expected. A tightly packed basket delayed core heating, although the display looked stable. This is easy to miss. Ask for uniformity surveys under loaded conditions, not empty chambers. Check recorder accuracy, thermocouple placement, alarms, and calibration records.
Match the oven with the quench system, material certificates, operator skills, and local electrical requirements. Salt-bath processes can be effective, but chemical handling and environmental controls require careful review. For international projects, request manuals, spare-part lists, training plans, and service terms in writing. Energy data should include real production loads. A compact design may save floor space, yet maintenance access can become awkward. Inspect doors, seals, fans, sensors, and cleaning access before approval. Temperature rating alone proves little.
Typical industrial upper working temperatures are shown for seven widely used hardening oven categories. Actual limits depend on chamber design, atmosphere, heating elements, load geometry, and applicable safety standards.
Air-circulation ovens suit general tool steels and medium-volume batch work, while continuous mesh-belt ovens support high-throughput parts. Vacuum and controlled-atmosphere furnaces are preferred for low-oxidation processing of alloy steels and precision components. Salt-bath, fluidized-bed, and infrared systems can provide rapid heating, specialized temperature control, or shorter cycle times for compatible materials and workloads.
Safety must guide every hardening oven purchase. Check chamber insulation, door interlocks, over-temperature protection, and emergency shutdowns. NFPA 86 provides widely used guidance for industrial ovens and furnaces. Local requirements may differ, so confirm compliance before shipment. The IEA Energy Efficiency 2023 report states that industry uses about 37% of global final energy. Therefore, poor insulation becomes a direct operating cost. Ask for temperature-uniformity test results, not only the rated temperature.
Energy efficiency depends on production habits, not just oven design. Review heating power, recovery time, standby consumption, and batch loading. A 2023 U.S. Department of Energy assessment found that industrial facilities often have practical energy-saving opportunities through controls, insulation, and process optimization. Installation also needs floor-load data, ventilation plans, electrical capacity, and safe exhaust routing. Global buyers should request drawings in advance. A compact oven can still create expensive site changes.
Tips: Request a factory acceptance test with real load conditions. Verify calibration certificates and spare-parts availability. Ask who provides remote troubleshooting across time zones. Clarify response times in writing. Train operators before commissioning. Do not assume translation guarantees technical understanding. A cheaper quote may hide weak after-sales support. Recheck everything.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

