


Choosing the right China supplier for Galvalume Corrugated Sheet requires more than comparing online prices. Roofing performance depends on coating mass, base-steel strength, profile accuracy, and production control. The World Steel Association’s 2024 Short Range Outlook identifies construction as a major driver of global steel demand, keeping durable roofing materials commercially important. Yet market demand alone does not prove supplier reliability.
Galvalume coating usually contains approximately 55% aluminum, 43.4% zinc, and 1.6% silicon. This composition supports strong corrosion resistance and heat reflectivity. ASTM A792/A792M provides a recognized specification for aluminum-zinc alloy-coated steel sheet. Buyers should request mill certificates, coating-mass results, tensile data, thickness tolerances, and inspection records. ISO 9223 corrosion categories can also help match the sheet to coastal, industrial, or rural exposure. The details matter.
A dependable Chinese manufacturer should explain coil origin, forming equipment, testing frequency, packaging methods, and export experience. Samples should show clean corrugation peaks, consistent coating, and protected edges. Ask for evidence, not promises. Some suppliers quote attractive prices by reducing coating mass or using thinner steel. That weakness may remain invisible until the first harsh season. No supplier is perfect. Even experienced exporters can overlook packaging damage or color variation. Therefore, this guide compares China’s leading Galvalume Corrugated Sheet suppliers through measurable specifications, quality practices, certifications, delivery capability, and customer experience. The goal is practical selection, not promotional ranking. A careful buyer may still need independent inspection before shipment.
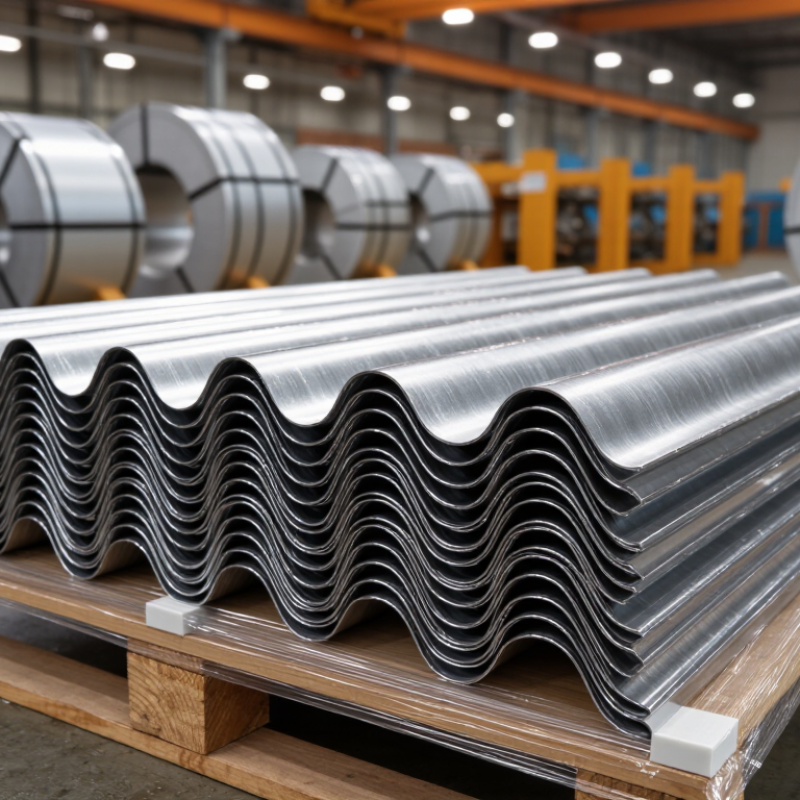
Galvalume corrugated sheet uses a metallic coating containing 55% aluminum, 43.4% zinc, and about 1.6% silicon by weight. This composition follows the coating principle specified in ASTM A792/A792M. Aluminum forms a stable barrier, while zinc offers sacrificial protection around minor scratches. The balance matters.
A common AZ150 designation means 150 g/m² of coating on both surfaces. That equals roughly 40 micrometres in total, depending on coating density. The corrugation increases bending stiffness without adding much steel weight.
However, it does not repair poor coating control. Inspectors should check coating mass, thickness, yield strength, and bend performance through mill certificates and sampling.
Industry demand remains substantial. The World Steel Association reported approximately 1.84 billion tonnes of crude steel production in 2023, supporting broad use of coated steel products. Market research reports also project steady growth for the global metal roofing sector through 2030, driven by industrial buildings and replacement construction. Figures vary between reports, so they should not replace project-specific testing.
Field experience shows that exposed cut edges often deserve more attention than the shiny surface. Drainage design, fastener compatibility, and condensation control can influence service life. Salt-spray results alone can mislead. I would also question any supplier promising identical performance without stating coating mass, steel grade, tolerance, and testing standards. The label sounds simple. The specification is not.

Choosing the best China galvalume corrugated sheet supplier starts with verified specifications, not attractive photographs. ASTM A792/A792M should define the steel substrate, coating quality, mechanical properties, and testing requirements. Ask for the exact grade, yield strength, tensile strength, and elongation before placing an order.
AZ50 to AZ150 coating ranges provide different levels of corrosion protection. Confirm whether the AZ value refers to total coating weight on both sides. This detail is often missed. A 0.13 mm sheet suits lightweight roofing and wall applications, while 1.50 mm material offers greater rigidity for demanding structures. Request thickness tolerances, effective cover width, corrugation depth, cut length, and forming direction. Samples should be checked for edge cracking, coating adhesion, surface scratches, and waviness. Inspection records are useful, but they are not perfect proof. Independent testing may still be sensible for large projects.
Tips: Match AZ50–AZ150 with the site environment, expected service life, and maintenance plan. Confirm the coating before forming, because tight bends can expose weak areas. Compare actual delivered weight with the purchase specification. Keep mill certificates, coating test results, and packing photographs. Small documentation gaps can become expensive later. In my experience, buyers sometimes focus too heavily on price and overlook profile accuracy. That decision deserves a second review.
| Specification Category | Parameter | Available / Standard Value | Technical Details | Typical Use |
|---|---|---|---|---|
| Product Standard | Applicable Standard | ASTM A792 / A792M | Steel sheet, 55% aluminum-zinc alloy-coated by the hot-dip process | Roofing, wall cladding and general construction |
| Base Steel | Steel Grade | Commercial quality, structural quality and forming grades | Grade selection should match the required forming, strength and service conditions | Panels, flashing, trim and profiled sheets |
| Thickness | Base Metal Thickness | 0.13–1.50 mm | Thickness should be confirmed as base metal thickness or total coated thickness before ordering | Light-duty roofing through heavier structural applications |
| Width | Width Before Corrugation | 762–1,250 mm typical | Custom widths may be produced subject to mill capability and minimum order requirements | Roll forming and custom panel production |
| Length | Cut-to-Length Sheet | 1,800–12,000 mm typical | Exact length depends on transport, panel profile and project requirements | Factory-cut roofing and wall panels |
| Coating | AZ50 | 150 g/m² minimum total both sides | Equivalent to approximately 0.50 oz/ft² total coating mass | Interior or lower-exposure applications where permitted |
| Coating | AZ55 | 165 g/m² minimum total both sides | Equivalent to approximately 0.55 oz/ft² total coating mass | General roofing and siding applications |
| Coating | AZ70 | 210 g/m² minimum total both sides | Equivalent to approximately 0.70 oz/ft² total coating mass | Common choice for exterior building envelopes |
| Coating | AZ90 | 275 g/m² minimum total both sides | Equivalent to approximately 0.90 oz/ft² total coating mass | Higher atmospheric exposure and longer service requirements |
| Coating | AZ100 | 305 g/m² minimum total both sides | Equivalent to approximately 1.00 oz/ft² total coating mass | Exterior roofing, cladding and industrial buildings |
| Coating | AZ150 | 458 g/m² minimum total both sides | Equivalent to approximately 1.50 oz/ft² total coating mass | Severe exposure conditions and extended durability requirements |
| Surface Finish | Surface Treatment | Regular spangle, minimized spangle or skin-passed finish | Surface appearance and roughness depend on the production route and finishing requirements | Architectural and functional panel surfaces |
| Surface Protection | Passivation / Chemical Treatment | Available by specification | Used to reduce wet-storage staining and improve handling performance; compatibility should be verified before painting | Coil storage, transport and further coating |
| Paintability | Pre-Painted Option | Available with compatible primer and topcoat systems | Coating system should be selected for UV exposure, humidity, chemical environment and forming requirements | Colored roofing and architectural cladding |
| Corrugation | Profile Options | Wave, trapezoidal and customized profiles | Effective cover width, pitch, crest height and overlap are determined by the roll-forming design | Roof panels, wall panels and agricultural buildings |
| Dimensional Control | Flatness and Shape | Controlled according to ASTM A792 requirements | Inspection may include thickness, width, length, camber, edge wave and surface condition | Consistent installation and panel alignment |
| Testing | Quality Inspection | Coating mass, thickness, tensile properties, bend performance and appearance | Inspection documents should identify the heat, coil or batch and the applicable specification | Project approval and incoming material verification |
| Packaging | Standard Export Packing | Waterproof paper, steel sheet protection and strapped bundles or coils | Packaging should prevent moisture ingress, edge damage and movement during transportation | Container and inland transport |
| Note: AZ coating designations indicate the approximate total coating mass on both surfaces in oz/ft². Metric values are approximate conversions; the exact purchase specification, tolerances and inspection requirements should be confirmed against ASTM A792/A792M and the project order. | ||||
A reliable China supplier should prove coil quality, not only quote a low price. ASTM A792/A792M commonly specifies a 55% aluminum-zinc coating for Galvalume steel. Ask for mill certificates showing yield strength, tensile strength, thickness tolerance, coating mass, and chemical composition. Independent testing can verify coating adhesion and corrosion resistance. The World Steel Association reported about 1.89 billion tonnes of crude steel production worldwide in 2023. China produced over 1 billion tonnes, showing strong capacity, but volume alone does not guarantee consistent corrugated sheets.
Certifications need careful checking. ISO 9001 supports documented quality systems, while product compliance should match the destination market. Request recent audit records, calibration reports, and sample inspection photographs. Confirm whether the supplier owns the production line or relies on outside processors. Capacity should include actual monthly output, forming-line speed, and peak-season availability. Lead time must separate coil purchasing, profiling, packing, and vessel scheduling. A written production plan is more useful than “fast delivery.” A larger mill is not automatically better. Some specifications still need clarification.
Tips: Order a small trial batch before signing a long contract. Measure sheet thickness at several points, inspect cut edges, and compare actual bundle weight with the packing list. Also check whether color, wave height, length, and packaging match the approved sample. The World Steel Association’s 2024 market data shows how large steel supply chains are, yet small documentation gaps can still create costly delays.
Galvalume corrugated sheets combine aluminum, zinc, and a small amount of silicon for balanced protection. In practical roof inspections, the coating often performs better than ordinary galvanized steel in humid conditions. Aluminum forms a stable barrier, while zinc helps protect exposed scratches. This protection is not unlimited. Cut edges, trapped moisture, and damaged fasteners can still create corrosion points. Coating thickness and drainage design matter greatly.
Bright Galvalume surfaces commonly show initial solar reflectance near 0.65–0.75, depending on finish, dust, and measurement method. Higher reflectivity can reduce roof heat absorption during strong sunlight. It may improve indoor comfort, but insulation and ventilation remain important. With suitable coating weight, correct installation, and regular maintenance, a service life of 20–30 years is achievable in many low-to-moderate exposure areas. Coastal or industrial environments may shorten that estimate. Real projects should use local exposure data, not optimistic catalog promises.
Tips:
Check coating mass, steel thickness, test reports, and warranty conditions before purchasing. Inspect overlaps and cut edges during installation. Keep leaves and standing water away from the roof. A small installation mistake can erase years of expected performance.
One point deserves reflection: “20–30 years” is a planning range, not a guarantee. Reliable suppliers should explain test methods, inspection limits, and environmental assumptions clearly.
China Best Galvalume Corrugated Sheet Supplier?
Choosing a supplier requires more than comparing one price. World Steel Association data recorded about 1.89 billion tonnes of crude steel production in 2023. That scale creates many options, but quality can vary sharply. A reliable quotation should state base steel grade, coating mass, thickness tolerance, width, profile, and packaging. Galvalume typically uses an aluminium-zinc coating, while ASTM A792/A792M provides a recognized specification for coated steel sheet. Start with comparable specifications. Not the lowest number.
Custom profiles deserve practical checks. Ask for roll-forming drawings, effective cover width, crest height, pitch, and minimum order quantity. Request a trial sample before approving a large batch. A small mismatch may cause leaks, wasted fasteners, or difficult installation. Pricing should include cut-to-length service, protective film, pallets, inland transport, and loading. Otherwise, the “cheap” offer may become costly.
Inspection evidence separates experienced suppliers from traders. Independent or buyer-appointed inspections can verify thickness, coating mass, dimensions, surface condition, and bending performance. Inspection records should identify coil numbers and test methods. Export support also matters: packing lists, commercial invoices, certificates of origin, fumigation documents, and shipment photos reduce avoidable delays. The International Trade Centre regularly highlights documentation and logistics as major factors in cross-border trade efficiency. Still, paperwork is not proof of production control. Review mill certificates, retain samples, and ask difficult questions. That part is often missed.
Coating mass is a practical starting point for comparing Galvalume corrugated sheet quotations. The chart shows common AZ coating designations used under EN 10346, expressed as total coating mass on both sides.
When selecting a supplier, compare the quoted price against the required coating class, steel thickness, yield strength, custom profile dimensions, color and cut-to-length accuracy. Request mill certificates, coating-thickness inspection records, dimensional reports, packaging specifications and export documents before placing an order.
Reference basis: Common AZ100, AZ150 and AZ185 coating-mass designations in EN 10346. Actual availability, tolerances, lead time and pricing depend on the agreed specification and order quantity.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

