


Choosing among die cutter manufacturers in China requires more than comparing catalog prices. A die-cutting machine may shape cartons, labels, foam, or protective inserts, yet its value depends on accuracy, uptime, and after-sales support. On a factory floor, a 0.1-millimeter registration error can create visible defects across thousands of sheets. Small details matter.
Industry demand supports careful supplier research. Smithers’ The Future of Global Packaging to 2028 values the worldwide packaging market at more than US$1 trillion and forecasts continued growth through 2028. Its analysis highlights e-commerce, food packaging, and sustainability as important demand drivers. These trends increase pressure on converters to process shorter runs, recyclable substrates, and more complex designs. China remains a major manufacturing base, supported by extensive machinery supply chains and export experience. However, production scale alone does not prove engineering quality.
This guide examines leading Chinese suppliers through practical purchasing criteria. These include cutting precision, maximum sheet size, production speed, tool compatibility, waste stripping, automation, and service response. We also consider ISO certification, CE-related export documentation, factory testing, spare-parts availability, and customer references. Reports from PMMI and other packaging-industry organizations consistently show that automation and operational efficiency are becoming stronger investment priorities. The evidence is useful, but not perfect. Published figures often combine different machine categories, making direct comparisons difficult. A low quotation can also hide training costs, tooling expenses, or delayed support. The best choice is rarely the cheapest one. It is the manufacturer that can demonstrate stable results on your actual materials, order volumes, and delivery conditions.
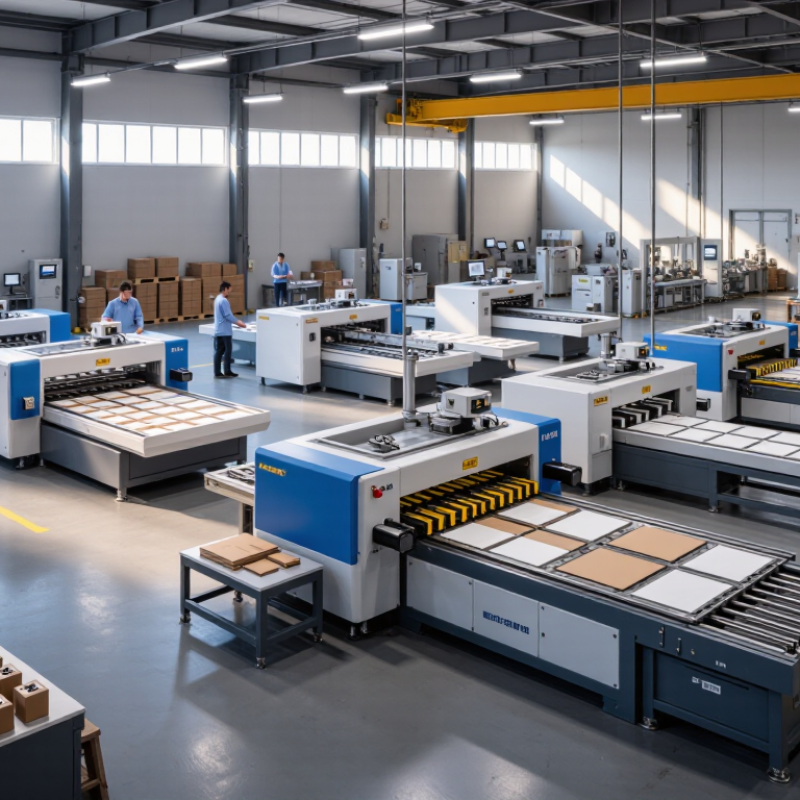
What Are the Best die cutter manufacturers in China?
China’s die-cutting industry is measured by accuracy, speed, and process control. Accuracy means more than a clean first sample. It includes repeatability across long production runs, stable dimensions, and consistent edge quality. For thin films, labels, foam, and insulating materials, buyers should check actual tolerances for each application. A cutting error of 0.2 millimeters can affect assembly. Small details matter.
Speed must be judged with quality. A machine may reach a high cycle rate, yet frequent adjustments can reduce real output. During a factory evaluation, review changeover time, waste levels, inspection records, and delivery performance. ISO 9001 certification shows that a documented quality management system exists. It does not automatically prove excellent cutting accuracy. That distinction is often overlooked. I have seen impressive samples fail during continuous testing. One test is never enough.
Tips: Request production samples made from your own material. Measure ten or more pieces, not just one. Ask for calibration records, in-process inspection steps, and corrective-action reports. Check whether operators record defects by cause. Also inspect storage conditions, because humidity can change paper, foam, and adhesive behavior. Be realistic about speed claims. The fastest setting may not be the most reliable setting.

Chinese die cutter manufacturers increasingly target production speeds above 6,000 sheets per hour. This figure usually applies to specific paper grades, sheet sizes, and repeat jobs. It is not a universal factory output. Experienced buyers should request test data, not rely on brochure claims. A machine may reach the headline rate with clean, uniform stock, yet slow sharply during creasing, stripping, or pile changes.
The strongest manufacturers support this speed with rigid frames, servo-driven feeding, accurate gripper chains, and automated register control. These details matter when sheets arrive at the feeder every fraction of a second. During a factory evaluation, request a live run using your own board. Check waste removal, die pressure stability, noise, and stoppage frequency. Record usable sheets per hour, not only the counter reading. Small errors become expensive.
Some Chinese suppliers provide remote diagnostics, operator training, and spare-parts planning, which can protect uptime after installation. Still, service quality differs between factories and regions. Ask for documented acceptance standards and references from comparable plants. I would also challenge the 6,000+ target. It may be realistic for one product, but not every order. A careful decision weighs sustained output, safety systems, setup time, and defect rates together.
What Are the Best Die Cutter Manufacturers in China?
Comparing Flatbed, Rotary, and Laser Cutters at ±0.1 mm Tolerance
Choosing a die cutter manufacturer in China requires more than checking machine speed. The real test is repeatable accuracy. A ±0.1 mm tolerance sounds precise, but material thickness, humidity, tool wear, and operator settings can change results. Experienced manufacturers should provide inspection records, calibration procedures, and sample-cutting evidence. Ask for actual results on your material, not only catalog specifications.
Flatbed cutters suit prototypes, short runs, and thick materials. They offer flexible tool changes and clear control over small batches. Rotary cutters perform better for high-volume labels, films, and flexible packaging. Their tooling can deliver stable output, although setup costs may be higher. Laser cutters handle detailed shapes without physical dies. However, heat can discolor edges or affect sensitive films. In my experience, laser accuracy is impressive on paper, yet production testing often reveals small thermal variations. No method is perfect.
Tips: Send the manufacturer your real material samples and target drawings. Request at least three repeated cuts, measured with calibrated instruments. Check corner details, waste levels, and edge quality. Also ask how the machine performs after several hours of continuous operation. A reliable supplier should explain limitations clearly, even when the answer is inconvenient. That honesty matters.
| Comparison Dimension | Flatbed Die Cutter | Rotary Die Cutter | Laser Die Cutter | Practical Evaluation for a ±0.1 mm Requirement |
|---|---|---|---|---|
| Cutting Method | Reciprocating steel-rule die cuts sheets or web-fed materials on a flat working surface. | Cylindrical magnetic or solid rotary tooling continuously cuts a moving web. | Focused laser energy cuts or marks material without physical tooling contact. | All three technologies can be suitable, but actual accuracy depends on machine construction, calibration, material stability, and operating conditions. |
| Typical Positioning Accuracy | Approximately ±0.05 to ±0.15 mm on suitable machines and stable substrates. | Approximately ±0.05 to ±0.15 mm, influenced by web tension, registration, and cylinder condition. | Approximately ±0.03 to ±0.10 mm with a calibrated motion system and suitable optics. | A verified ±0.1 mm result should be confirmed using production samples rather than catalog specifications alone. |
| Best-Suited Materials | Paperboard, corrugated board, foam, rubber, gasket materials, adhesive labels, and thin plastics. | Paper, labels, films, foil laminates, pressure-sensitive adhesive materials, and continuous web stock. | Paper, films, textiles, nonwoven materials, wood-based sheets, selected plastics, and thin composites. | Material composition, thickness, reflectivity, heat sensitivity, and adhesive behavior must be tested before final selection. |
| Typical Material Thickness | Commonly handles thin films through several millimeters, depending on cutting force and tooling. | Generally optimized for thin, continuous web materials and repeatable production thicknesses. | Commonly used for thin sheets and films; excessive thickness may require multiple passes or higher laser power. | For thick board, foam, or gaskets, verify maximum cutting force, die clearance, and edge-quality results. |
| Production Speed | Low to medium; frequently selected for short and medium production runs. | High; continuous web processing supports efficient long-run production. | Low to medium for intricate work; speed varies significantly with material, geometry, and required edge quality. | Rotary systems generally provide the highest sustained throughput when the design and material remain stable. |
| Changeover Time | Usually short for digital files, but physical die replacement may be required for each design. | Longer when rotary tooling, cylinders, or web setups must be changed. | Very short for design changes because cutting paths are controlled digitally and no steel rule die is required. | Laser technology is usually more flexible for frequent design changes and variable-data production. |
| Tooling Requirement | Requires a steel-rule die, often with creasing, perforating, or embossing features. | Requires rotary dies or engraved cylinders, with tooling cost depending on size and complexity. | No conventional cutting die; requires a laser source, focusing optics, extraction, and motion-control system. | Tooling cost and lead time are important when comparing total ownership cost rather than machine price alone. |
| Edge Quality | Clean mechanical edges with little thermal effect; quality depends on die sharpness and material compression. | Consistent mechanical edges during long runs when the rotary tooling is correctly maintained. | May produce a sealed, darkened, or heat-affected edge on some materials; edge appearance depends on power and speed settings. | For heat-sensitive films, foams, and adhesives, request cut-edge samples and inspect melting, residue, and delamination. |
| Registration Control | Uses printed-mark sensors, camera systems, or mechanical alignment references. | Uses web guides, tension control, encoder feedback, and printed-mark registration systems. | Uses vision registration, fiducial recognition, encoders, or pre-printed alignment marks. | For ±0.1 mm work, closed-loop registration and repeatable material feeding are more important than nominal machine speed. |
| Waste Management | May require matrix stripping, waste removal, or manual separation depending on the layout. | Efficient for repeat layouts but can generate setup waste during web alignment and tooling changes. | Can reduce tooling-related waste, but fumes, smoke, kerf width, and heat distortion must be controlled. | Compare usable yield, skeleton waste, setup waste, and extraction requirements for the complete process. |
| Maintenance Profile | Requires die sharpening or replacement, pressure adjustment, lubrication, and alignment checks. | Requires cylinder and die inspection, web-tension maintenance, bearings, registration, and lubrication checks. | Requires lens and mirror cleaning, focus calibration, filtration, extraction maintenance, and laser-source monitoring. | A strong supplier should provide preventive-maintenance intervals, spare-parts availability, and calibration procedures. |
| Main Advantages | Versatile, strong mechanical cutting force, good for varied substrates, and suitable for creasing or embossing. | High productivity, repeatable web processing, and economical unit cost for large, stable production volumes. | Digital flexibility, no conventional die cost, fast design changes, and excellent capability for complex contours. | The best technology depends on order volume, substrate, geometry, changeover frequency, and required edge appearance. |
| Main Limitations | Physical tooling is required, and frequent design changes can increase die cost and setup time. | Less economical for short runs or frequent artwork changes; tooling and web setup can be complex. | Thermal effects, fumes, material compatibility, and laser-safety requirements can limit applications. | No single cutter type is best for every application; supplier selection should be based on validated samples and lifecycle cost. |
| Recommended Production Scenario | Short-to-medium runs, structural packaging, gaskets, foam parts, and jobs requiring creasing or embossing. | High-volume labels, flexible packaging components, repetitive web products, and long production campaigns. | Prototyping, customized products, intricate shapes, short runs, and jobs with frequent digital revisions. | For mixed production, a supplier offering more than one cutting platform may provide better application coverage. |
| Supplier Verification Checklist | Request repeatability data, die-life estimates, sample cuts, pressure maps, and alignment test results. | Request web-tension data, registration samples, rotary-tooling specifications, speed tests, and waste calculations. | Request laser wavelength and power data, focus tests, kerf measurements, extraction details, and safety documentation. | Require a documented acceptance test showing dimensional results at multiple positions and across repeated production cycles. |
What Are the Best Die Cutter Manufacturers in China?
Choosing a die cutter manufacturer requires more than comparing prices and machine photos. CE compliance should be verified through the actual Declaration of Conformity, technical documentation, and relevant test reports. A CE logo alone proves very little. Check whether the documents match the exact model, voltage, safety functions, and intended use. Ask for risk assessments, emergency-stop details, and updated manuals. A careful supplier should explain these items clearly, not avoid technical questions.
Factory capacity also needs physical verification. Request a live video tour or schedule an independent audit. Look for machining areas, assembly lines, testing stations, and finished machines awaiting shipment. Ask how many units the factory produces monthly and how production schedules are controlled. A large showroom may impress buyers, but it cannot replace evidence. I would also inspect sample cutting accuracy, waste removal, noise levels, and electrical wiring. No audit is perfect. Recheck important claims.
Tips: Ask for customer references using similar materials and machine sizes. Confirm warranty length, spare-parts availability, installation guidance, and technician response times in writing. Clarify whether remote troubleshooting includes video support and replacement-part advice. Some suppliers promise fast service but provide vague timelines. Set measurable standards, such as a response within one business day and spare-part dispatch within a defined period. Keep every commitment in the purchase contract.
Recommended evidence priorities for checking CE compliance, factory capacity, and after-sales support
CE verification should include the EU Declaration of Conformity, technical documentation, risk assessment, and applicable machine-safety standards. Factory capacity is best validated through equipment lists, production records, quality-control procedures, and factory audits. After-sales support should be confirmed through warranty terms, spare-parts availability, remote service, and technician response procedures. These percentages are due-diligence priorities, not company rankings or market-share data.
Matching Chinese die cutter manufacturers to applications requires more than comparing machine speed. The Future of Global Packaging to 2028 forecasts global packaging demand above 1.2 trillion dollars by 2028. That growth increases pressure on cutting accuracy, changeover time, and material efficiency. For folding cartons, choose a flatbed system with stable pressure control and automatic stripping. For corrugated boxes, prioritize a wider working format, high feeding stability, and quick tooling changes. Small errors become expensive during long production runs.
Label converters need precise registration and clean waste removal. Rotary or semi-rotary equipment may fit better than a general-purpose flatbed machine. For foam inserts, gaskets, and protective materials, ask about low-pressure cutting, dust control, and tolerance testing.
The 2024 Global Packaging Machinery Market report estimates a 52.8-billion-dollar market in 2023, with approximately 5.5% annual growth through 2030. Chinese suppliers often offer flexible configurations and competitive automation. However, the lowest quotation can hide costly tooling limits, slower service, or unclear spare-parts planning. That part deserves skepticism.
A practical audit should include customer-supplied samples, a recorded cutting test, and measured waste rates. Request tolerance data, power requirements, software language options, and maintenance intervals. Check whether the manufacturer can support your material thickness before discussing output speed. A perfect shortlist rarely exists. Your own production data should challenge the supplier’s brochure.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

