


Choosing the best Chemical Anchor supplier in China requires more than comparing prices, packaging, or catalog size. The real test begins with performance evidence. A dependable supplier should provide clear technical data, batch traceability, installation instructions, and responsive engineering support. Its products should suit cracked and uncracked concrete, different temperatures, moisture conditions, and demanding construction schedules.
Structural fastening specialist Dr. Ronald A. Cook offers a useful reminder: “Anchor performance is a system issue, not a product issue.” This principle matters during supplier evaluation. Resin quality is only one part of the result. Drill-hole cleaning, embedment depth, curing time, steel grade, and installation torque can change the final capacity. A serious manufacturer should explain these details without hiding behind vague claims.
Look for documented testing, consistent factory production, and practical field experience. Certificates can help, but they do not replace manufacturing discipline. Ask for recent inspection records, sample batches, technical drawings, and application guidance. Then compare how quickly and accurately the supplier answers difficult questions.
A low quotation may seem attractive. It may also reveal missing support.
The strongest Chemical Anchor supplier is not always the largest company. It is the one that connects laboratory results with jobsite reality. Still, no supplier is perfect, and buyers should verify every important claim independently. Visiting the factory, reviewing test methods, and checking references can expose weaknesses before concrete is drilled. This careful process supports safer decisions, stable project costs, and more reliable long-term performance.
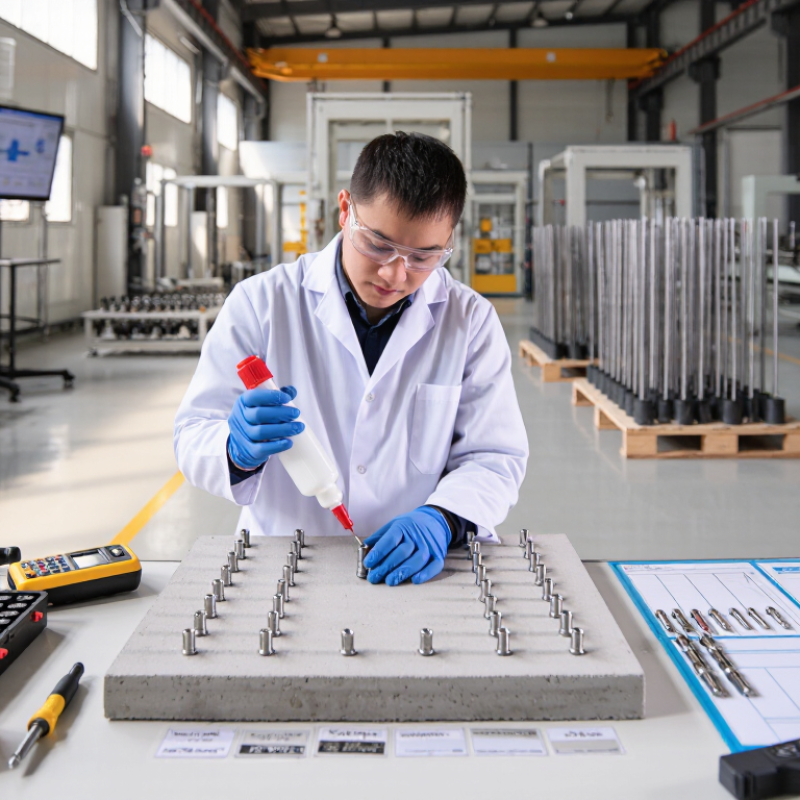
The best chemical anchor supplier is not always the cheapest. It should match chemistry, load demand, and EN 1504-6 requirements. Polyester systems suit moderate loads and cost-sensitive projects. Vinyl ester usually offers better performance in cracked concrete and damp conditions. Epoxy systems support high loads, deeper embedment, and longer working times. The choice still depends on temperature, hole cleaning, curing time, and installation quality.
EN 1504-6 covers products used for anchoring reinforcing steel bars in concrete. It does not create simple “light,” “medium,” or “heavy” load classes. Buyers should request tested characteristic resistance, displacement data, bond performance, and durability results. EOTA TR 029 also highlights the importance of cracked and non-cracked concrete assessments for bonded fasteners.
A 2024 MarketsandMarkets report estimates the global construction adhesives market will grow from about USD 10.2 billion in 2023 to USD 14.1 billion by 2028. That growth increases supplier choices, but not necessarily product reliability.
Ask Chinese suppliers for batch traceability, third-party laboratory reports, technical data sheets, and installation records. Check whether the certificate covers the exact resin, mixing nozzle, embedment depth, and application. One certificate is not proof of every cartridge.
Evidence matters.
I would also inspect factory storage conditions, because expired or overheated resin can reduce bond strength before installation begins. The uncomfortable point is simple: even excellent chemistry can fail after poor hole cleaning.

What Is the Best Chemical Anchor Supplier in China?
The best chemical anchor supplier is not simply the lowest-cost factory. It is the supplier that can prove performance, consistency, and product history. The ISO Survey 2022 recorded 1,265,216 ISO 9001 certificates worldwide, but certification alone does not confirm anchor capacity. Request the certificate scope, issuing body, audit date, and manufacturing address. Confirm that the certificate covers chemical anchor production, not only trading activities.
ETA documentation should identify the assessed application, substrate, load range, installation method, and service conditions. ICC-ES AC308 evaluation should match the actual adhesive anchor system, including the resin, hardener, mixing nozzle, and steel element. A copied test report is not enough. Check the report number, product formulation, laboratory details, and approval scope. Testing should come from a competent laboratory, preferably operating under ISO/IEC 17025 principles.
Traceability needs physical evidence. Ask for batch codes on cartridges, production records, raw-material certificates, retained samples, and shipment links. One missing batch record can weaken an otherwise convincing quality system. That is an uncomfortable point. Supplier documents may look complete while factory controls remain uneven. A practical audit should follow one cartridge from incoming resin to final packing. Also review curing data, temperature limits, pull-out results, and complaint records. The strongest supplier answers technical questions consistently, even when the answer is “not yet available.”
| Screening Dimension | What Should Be Verified | Objective Acceptance Requirement | Evidence to Request | Priority |
|---|---|---|---|---|
| Quality management system | Whether the manufacturing site operates a certified ISO 9001 quality management system. | Certificate is valid, issued by an accredited certification body, covers the actual production site, and includes relevant chemical or construction-product activities. | Current ISO 9001 certificate, certification-body details, scope, site address, issue date, expiry date, and certificate verification link. | Critical |
| European technical approval | Whether the chemical anchor system has a valid European Technical Assessment for its intended use. | The ETA must identify the exact product, approved installation conditions, anchor sizes, base materials, temperature limits, service-life assumptions, and permissible loads. | Complete ETA document, European Assessment Document reference, performance tables, installation instructions, and notified or technical assessment body information. | Critical |
| ICC-ES AC308 compliance | Whether the adhesive anchor has been evaluated under ICC-ES Acceptance Criteria AC308 or an equivalent recognized evaluation route. | A valid evaluation report must cover the exact adhesive formulation, dispensing system, anchor rod or rebar range, concrete conditions, seismic category, and installation limitations. | Current evaluation report, report holder details, product designation, allowable design data, limitations, and report verification source. | Critical |
| Product identity control | Whether the tested and certified product is identical to the product supplied for purchase. | Product name, formulation code, cartridge size, nozzle type, packaging, and manufacturing site must match the certification and technical documentation. | Technical data sheet, safety data sheet, label artwork, formulation or product code, packaging photographs, and document revision history. | High |
| Batch traceability | Whether every cartridge can be traced from raw materials through production, testing, packaging, and shipment. | Each unit or carton should show a readable batch or lot number, manufacturing date, expiry date, and storage requirements; records should be retained for the defined quality period. | Sample label, batch-production record, raw-material lot linkage, release record, retention policy, and mock recall results. | Critical |
| Raw-material control | How incoming resins, hardeners, fillers, additives, and packaging components are approved and controlled. | Approved suppliers, incoming inspection criteria, material specifications, nonconformance controls, and change-notification procedures must be documented. | Approved-vendor list, incoming inspection records, certificates of analysis, material specifications, and change-control procedure. | High |
| Performance testing | Whether production batches are tested against defined physical, chemical, and installation-performance criteria. | Routine testing should address items such as appearance, mix ratio, gel time, curing behavior, compressive or tensile performance, and bond-related characteristics where applicable. | Quality-control plan, batch test reports, laboratory equipment calibration records, sampling plan, and retained-sample procedure. | Critical |
| Installation documentation | Whether installers receive clear, controlled instructions for cleaning, dispensing, embedment, curing, and inspection. | Instructions must state hole diameter, drilling method, cleaning sequence, installation temperature, working time, curing time, torque or loading requirements, and safety precautions. | Controlled installation manual, technical data sheet, application drawings, training material, and revision-control records. | High |
| Storage and shelf life | Whether the supplier controls storage conditions and communicates usable shelf life accurately. | Packaging must state storage temperature, protection requirements, shelf life, expiry date, and compatibility with the specified dispensing equipment. | Packaging specification, warehouse records, temperature-monitoring records, shelf-life validation, and transport requirements. | High |
| Change management | Whether changes to formulation, raw materials, production equipment, site, packaging, or labeling are formally assessed. | No change affecting certified performance should be implemented without documented risk assessment, customer notification where required, and confirmation of certification impact. | Engineering-change procedure, change log, customer-notification template, requalification records, and certification-impact assessment. | Critical |
| Independent verification | Whether documents and test results can be verified through independent certification, assessment, or laboratory sources. | Certificates and reports must be current, internally consistent, independently traceable, and applicable to the exact product and manufacturing location. | Verification links, accredited-laboratory information, report authenticity confirmation, and third-party audit or inspection records. | Critical |
| Commercial reliability | Whether the supplier can maintain consistent supply, packaging quality, and technical support after approval. | Supplier should demonstrate documented production capacity, complaint-response targets, corrective-action capability, export experience, and continuity planning. | Capacity statement, quality agreement, sample lead-time record, complaint procedure, corrective-action reports, and business-continuity plan. | Medium |
What Is the Best Chemical Anchor Supplier in China?
The best chemical anchor supplier is not defined by price alone. Request verified results for tensile and shear tests under ASTM E488 or ASTM E488M. These tests reveal how an adhesive anchor performs in cracked or uncracked concrete. Check concrete strength, embedment depth, curing time, and failure mode. Without these details, a high load value can be misleading.
Seismic performance requires deeper review. ACI 355.4 evaluates adhesive anchors under repeated loading, sustained tension, temperature effects, and installation conditions. Look for qualified systems with documented seismic testing, not general laboratory claims. Compare residual strength after cycling, displacement, and sensitivity to dusty or damp holes. A reliable supplier should provide traceable reports, batch information, installation instructions, and independent test evidence. Photos of concrete failure can also expose weak assumptions.
Tips:
Ask for the complete test report, not only a certificate. Compare equal bar sizes, embedment depths, and concrete grades. Confirm whether the data covers cracked concrete and seismic categories relevant to your project. Test reports may use ideal installation conditions. Real construction is less forgiving. A site trial can reveal mixing errors, poor hole cleaning, or premature loading. I have seen impressive tensile results become less useful when curing temperatures changed. That limitation deserves honest discussion. Shear values also need careful interpretation because edge distance and spacing can control failure. A supplier willing to explain these weaknesses usually demonstrates stronger technical credibility.
Comparison of representative mean ultimate loads for anonymized chemical-anchor test groups under ASTM E488 static testing and ACI 355.4 seismic qualification conditions.
Values are shown in kN and should be interpreted only within a controlled test program using the same concrete strength, embedment depth, anchor diameter, curing conditions, and failure-mode criteria. ASTM E488 and ACI 355.4 do not define a single universal capacity for every anchor system.
A reliable chemical anchor supplier must prove performance beyond a polished catalogue. I once treated a clean-looking cartridge as evidence of quality. That was a mistake. Ask for the technical data sheet, safety data sheet, and batch-specific certificate of analysis.
Cure time needs careful checking. According to ACI 355.4-19 and ICC-ES AC308 evaluation methods, anchor performance depends on temperature, moisture, hole cleaning, and installation conditions. A resin curing in 20°C concrete may behave very differently at 5°C. The datasheet should state gel time, handling time, and full cure time for each temperature range. Do not accept “fast curing” as a test result. Record the actual site temperature.
Hole diameter is equally important. A 14 mm drill hole cannot be treated like a 16 mm hole. Verify the approved diameter, embedment depth, drilling method, and cleaning sequence against ASTM E488/E488M-based test evidence. Suppliers should also provide pull-out results, failure modes, and laboratory details. Ideally, the testing laboratory follows ISO/IEC 17025 procedures.
Shelf life must include unopened storage conditions, not only a printed expiry date. Check manufacturing dates, storage temperature, cartridge appearance, and nozzle compatibility. Batch records should show resin lot numbers, viscosity or gel-time checks, raw-material traceability, and production release approval. Some documents may look complete but lack test dates. That deserves a second question. Reliability is built from traceable records, not confident promises.
The best supplier is not always the cheapest per cartridge. Rank total cost by usable kilonewton capacity, not purchase price alone. Include resin cost, nozzle waste, freight, testing, and installation time. A supplier offering 25 kN capacity at a higher unit price may outperform a cheaper 15 kN product.
Ask for tested capacity in the exact concrete condition you need. Dry, cracked, wet, and post-installed applications can produce different results. Request laboratory reports, batch numbers, curing temperatures, and installation instructions. ISO 9001 certification supports process control, while independent test reports provide stronger technical evidence. Lead time also affects project cost. Record standard production time, stock availability, export documentation, and emergency replacement options. Warranty terms deserve equal attention. Check whether coverage includes product defects, shelf life, storage conditions, and technical support. Vague warranties create expensive arguments later.
Tips: Build a simple scorecard. Divide delivered cost by verified kN capacity. Score lead time, warranty clarity, and certification quality separately. Request three recent batches. Compare like with like. Numbers need context.
In my experience, suppliers answer quickly before an order, then become less precise when technical questions appear. That is a warning sign. I would also avoid trusting a perfect spreadsheet without site trials. Small differences in hole cleaning, temperature, and curing time can change real performance. A careful supplier should welcome these questions, even when the answers are inconvenient.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

