


Choosing the right Arm Cylinder is a practical decision for global equipment buyers. It affects lifting force, operating speed, stability, maintenance, and total ownership cost. A cylinder that looks suitable on paper may fail in dusty quarries, cold ports, or humid construction sites. Conditions matter.
Hydraulics author Andrew Parr offers a useful engineering principle: “A cylinder is only as reliable as the system around it.” That principle guides this 2026 comparison. Welded cylinders provide compact strength for mobile machinery. Tie-rod cylinders support easier servicing in controlled industrial environments. Telescopic cylinders suit limited installation spaces and long extension requirements. Custom cylinders may solve unusual mounting or stroke demands, but they often require longer lead times and closer technical communication.
Global buyers should examine bore diameter, rod size, stroke length, working pressure, mounting style, seal materials, and surface protection. They should also confirm compatibility with local hydraulic oil, temperature ranges, replacement seals, and available service skills. A low purchase price can become expensive when spare parts travel across borders. Small details become large problems.
This guide compares major Arm Cylinder types through practical selection criteria. It considers real equipment pressures, not only catalogue ratings. Some recommendations may change after field testing. That is worth admitting. Manufacturer data can be incomplete, and installation quality still controls much of the final result. Buyers should verify drawings, pressure limits, certifications, and performance evidence before placing large orders. Reliability begins with careful questions.
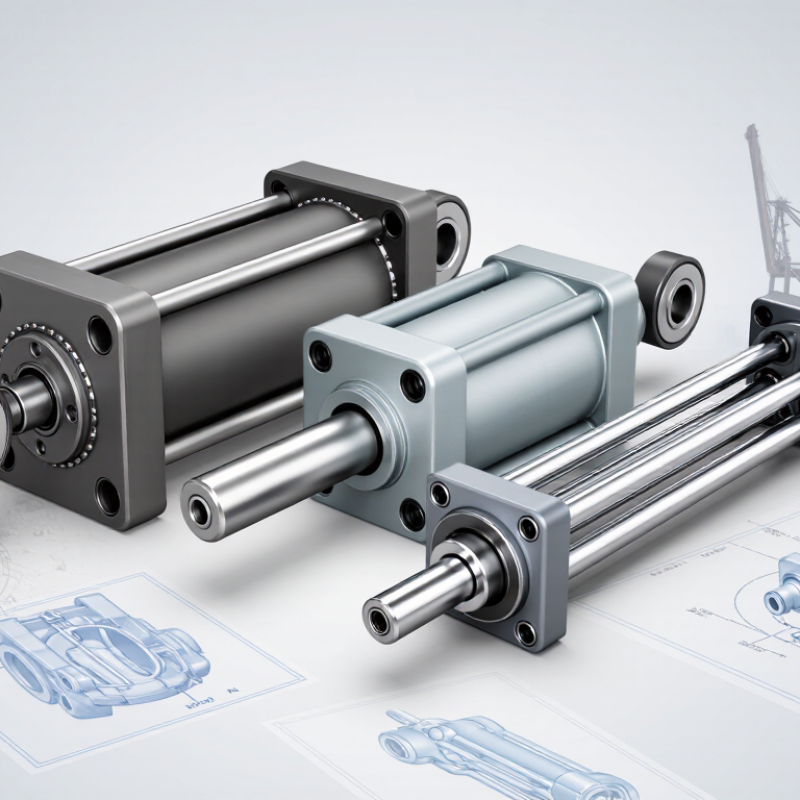
An arm cylinder converts hydraulic pressure into controlled linear movement. A pump sends oil through a directional valve. The valve fills one side of the cylinder, pushing the piston and rod outward. Reversing the flow retracts the rod. This is the core operating principle behind most excavator and material-handling arms.
Common designs include welded cylinders, tie-rod cylinders, double-acting cylinders, and cushioned cylinders. Welded models suit heavy equipment because their compact bodies tolerate demanding loads. Tie-rod designs allow easier servicing in lighter applications. Double-acting cylinders provide powered extension and retraction. Cushioning reduces impact when the piston reaches the end of its stroke. However, cushioning cannot correct poor sizing or excessive side loading.
Bore diameter controls pushing force, while rod diameter affects buckling resistance and retraction force. Stroke length determines the arm’s working range. Buyers should check working pressure, pin dimensions, mounting style, seal materials, and oil cleanliness. A clean calculation may still fail in muddy conditions. Field inspections often reveal bent rods, loose pins, or damaged seals before pressure readings show trouble.
Tips: Measure the existing cylinder before ordering. Confirm bore, stroke, rod size, and closed length. Choose corrosion-resistant protection for wet environments. Keep hydraulic oil filtered. Do not judge capacity from appearance alone. A small alignment error can create expensive wear.

Arm cylinders are usually double-acting hydraulic cylinders, but their structures vary by duty. Welded cylinders use a continuously welded barrel, integrated ports, and a threaded or welded head. They are compact and resist vibration, making them common on excavator arms. Tie-rod cylinders use four external rods to clamp the end caps against the barrel. They are easier to service, but exposed rods can collect mud and suffer corrosion. Telescopic cylinders use nested stages for longer stroke in limited spaces. Their structure is more complex, with tighter sealing and greater alignment demands.
The choice should follow load, stroke, installation space, and side-loading risk. ISO 6020/2 and ISO 6022 provide useful dimensional and pressure references for metric hydraulic cylinders. A 2024 Fortune Business Insights report valued the global hydraulic cylinders market at about USD 14.5 billion in 2023 and projected continued growth through 2032. This supports demand, but market growth does not make every design suitable.
For heavy arm applications, welded double-acting cylinders usually offer better stiffness and contamination protection. Mill-duty designs add thicker barrels, stronger glands, and replaceable wear components for severe cycles. Chrome-plated rods help, yet poor pin alignment can still damage seals. Field inspections often find this issue first. A clean specification should state rod diameter, bore, stroke, retracted length, working pressure, mounting dimensions, and cushioning. Buyers sometimes compare only pressure ratings. That is not enough. A lighter cylinder may fit perfectly, then fail under repeated side loads.
2026 Best Arm Cylinder Types for Global Buyers
How to Match Cylinder Specifications with Equipment Requirements
Choosing an arm cylinder starts with the machine’s real operating conditions, not a catalog photo. Most excavator arms need double-acting welded cylinders for controlled extension and retraction. Bore size determines pushing force, while rod diameter affects buckling resistance. Stroke must match the arm’s full movement without bottoming out. According to Grand View Research’s 2024 hydraulic cylinder assessment, the global market was valued at approximately USD 15 billion in 2023, with construction equipment remaining a major demand sector. That growth reflects stronger needs for reliable, application-specific sizing.
Pressure ratings also require careful checking. A cylinder rated for 250 bar may fail early if shock loads, contaminated oil, or repeated side loading are ignored. ISO 6020/2 and ISO 6022 provide useful dimensional and performance references, but they do not replace field calculations. In my experience, buyers often focus on bore and stroke, then overlook pin diameter, mounting width, seal temperature range, and hose routing. That is an expensive gap. A slightly larger rod can improve stability, yet it may reduce speed and increase machine weight. The “best” specification is rarely perfect.
Tips: Record working pressure, peak load, cycle frequency, ambient temperature, and oil type. Select corrosion protection for coastal or humid sites. Confirm retracted length before ordering. Leave tolerance for alignment. It matters. When data is incomplete, request load-cycle testing instead of guessing.
Materials and sealing systems should match the working market, not only the machine drawing. Grand View Research estimated the global hydraulic cylinder market at about USD 14 billion in 2023. Its forecast also indicates continued growth through 2030. Construction and material handling remain major demand areas. These sectors punish weak surface finishes and poor contamination control.
For general construction, honed steel barrels and induction-hardened chrome rods offer practical durability. Medium-carbon alloy steel can handle repeated loading, but corrosion protection needs attention near coasts. NBR seals suit many mineral-oil systems between roughly -30°C and 100°C. Polyurethane seals resist abrasion better in dusty worksites. FKM performs better at higher temperatures, although it costs more. PTFE backup rings help control extrusion under high pressure.
Regional standards change the buying decision. ISO 6020/2 and ISO 6022 define common mounting and pressure expectations for metric cylinders. North American buyers often compare designs with NFPA hydraulic cylinder practices. European equipment commonly requires evidence supporting the Machinery Regulation framework and applicable EN standards. Japan and China may expect JIS or GB conformity documents. ISO 4413 also stresses cleanliness, pressure control, and safe hydraulic-system design. MarketsandMarkets reported construction equipment as a leading hydraulic-cylinder application in its 2024 market analysis.
Still, catalog pressure ratings can mislead. Actual life depends on side load, rod alignment, oil cleanliness, and temperature cycling. I would request test data, seal compound details, and fatigue results before approving a large order. Some suppliers provide too little evidence.
Choosing an arm cylinder in 2026 requires more than comparing prices. Welded cylinders suit excavators because they tolerate vibration and limited space. Tie-rod designs can simplify servicing, while telescopic cylinders fit specialized lifting applications. MarketsandMarkets’ 2024 Hydraulic Cylinders report projects roughly 6% annual market growth through 2029. That growth increases supplier choice, but also increases quality differences.
Quality starts with measurable details. Check bore diameter, stroke length, rod coating, seal material, rated pressure, and mounting dimensions. ISO 6020/2 and ISO 6022 provide useful dimensional and pressure references. Compatibility remains critical. A cylinder can look correct and still fail because of a two-millimeter pin mismatch. Confirm hydraulic ports, oil type, operating temperature, and machine control settings. Total cost includes freight, installation, downtime, spare seals, and warranty response. A low quotation may become expensive after one damaged rod. Support matters most when a machine stops in a remote yard. Ask for inspection records, pressure-test results, drawings, and replacement-part lead times. Documentation is not decoration.
Tips: Request one sample unit before a volume order. Measure the old cylinder in person. Keep photos of pins, ports, and mounting brackets. Compare landed cost, not factory price. Some buyers still overlook local repair capability. That is worth reconsidering. A supplier with slower delivery but dependable technical support may protect productivity better than a cheaper unknown source. Feedback from mechanics should influence the final decision.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

