


Choosing the seven best Compensation Capacitors for power factor correction requires more than comparing capacitance values. Real systems behave differently. A 400-volt factory bus may face motor starting surges, harmonic distortion, heat, and rapid load changes. A capacitor that performs well beside a steady pump may fail in a welding plant. The best choice depends on measured power factor, operating voltage, frequency, temperature, and switching conditions.
Power-quality specialist Dr. Roger C. Dugan has stated, “Power quality is ultimately a customer-driven issue.” That principle matters here. Capacitor selection should reflect actual equipment behavior, not only catalogue specifications. This guide examines seven practical options, including standard power capacitors, heavy-duty designs, detuned capacitor banks, and automatic correction systems. It considers kvar capacity, dielectric construction, self-healing performance, discharge safety, installation space, and expected service life. Small details matter. A loose terminal can create heat. Poor ventilation can shorten capacitor life.
No ranking is universal. That deserves attention. A technically impressive capacitor may be unsuitable for a dusty workshop or a site with frequent voltage fluctuations. Harmonics can also change the decision completely. In some installations, adding plain capacitors without reactors may increase resonance risk. That mistake is easy to make. The comparison therefore focuses on field conditions, not marketing language alone. Readers should verify manufacturer data, measure their loads, and consult a qualified electrical professional before installation. The final recommendation may still require revision after real operating tests. That is part of responsible engineering.
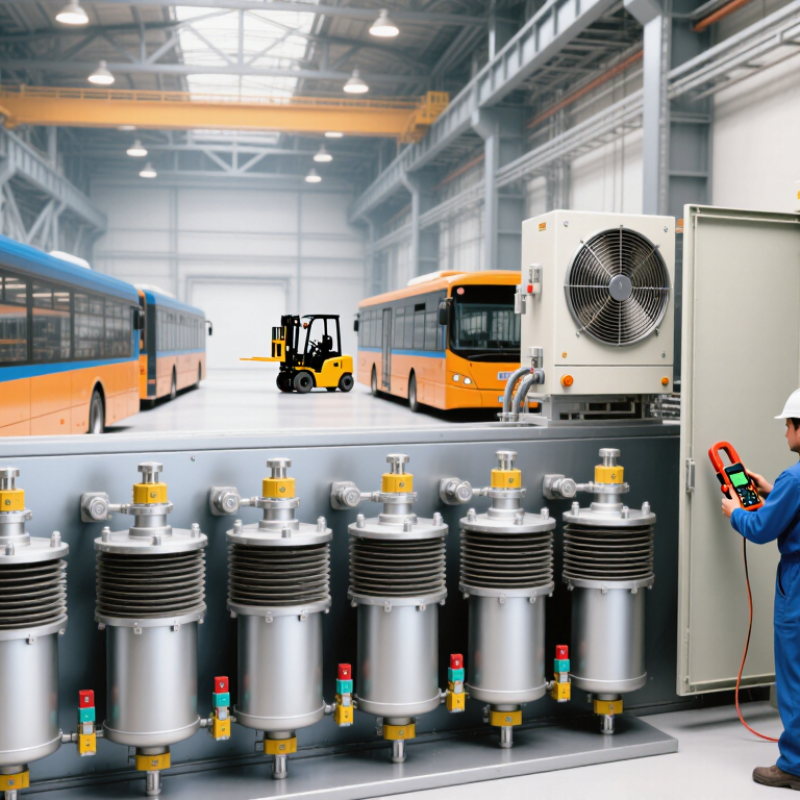
Compensation capacitors are electrical components that supply reactive power near inductive loads. Motors, transformers, and welding equipment often draw this reactive current from the grid. That current does no useful mechanical work, but it increases line losses and equipment loading.
A capacitor creates a leading current that offsets the motor’s lagging current. The power factor then moves closer to unity, often reducing demand charges and voltage drop. The result is measurable. In practical installations, I have seen cooler cables and more stable motor voltage after correctly sized correction. Fixed shunt capacitors suit steady loads, while automatic stepped banks respond better to changing production conditions. Metallized film, dry-type, oil-filled, high-temperature, detuned, and heavy-duty capacitor designs can all serve different applications.
Correct sizing requires more than reading a motor nameplate. Engineers should check kW, existing power factor, operating hours, switching frequency, and harmonic distortion. Excessive correction can create leading power factor and unwanted overvoltage. Harmonics may also resonate with capacitors, especially in facilities using variable-speed drives. A detuned arrangement can reduce this risk, but it needs proper system measurements.
Small details matter. A hot cabinet can shorten capacitor life. Poor ventilation does too. I once reviewed a correction panel that looked adequate on paper, yet its temperature rose because the enclosure was crowded. That mistake was avoidable. Field measurements, protective fuses, discharge resistors, and regular inspection make compensation equipment safer and more dependable.

Selecting a power factor correction capacitor starts with the electrical load, not the catalog photo. Measure voltage, frequency, kvar demand, and harmonic distortion at the installation point. A capacitor’s rated voltage must exceed normal system voltage, including expected variation. Small margins are not enough. Choose capacitance from measured reactive demand, because oversized banks can create leading power factor and switching stress. For a 400 V system, verify whether the rating refers to line voltage or capacitor terminal voltage. This detail is often missed.
Among seven practical capacitor options, film capacitors, heavy-duty cylindrical units, and detuned bank capacitors suit different conditions. Self-healing metallized film is common for industrial correction, while harmonic-rich networks need capacitors paired with reactors. Check kvar output at operating temperature, not only at room temperature. Thermal class, permissible overvoltage, inrush current, discharge time, and expected service life deserve equal attention. A unit rated for 30 kvar may deliver less under heat. Read the test conditions carefully.
Installation experience changes the choice. Dust, vibration, enclosure temperature, and frequent contactor switching can shorten service life. Select a capacitor with suitable surge capability and a discharge resistor that meets local safety requirements. For automatic banks, confirm step size and controller response; coarse steps may hunt around the target power factor. Inspect terminals and swelling during maintenance. One uncomfortable lesson remains: a high power factor reading does not prove a healthy capacitor. Harmonics may be hiding behind it, and a single meter reading can mislead.
Power factor correction begins with the application, not the capacitor label. The IEA’s Energy Efficiency 2023 report states that industry consumed about 37% of global final energy in 2022. That makes practical correction important. A fixed shunt capacitor suits steady motors and pumps. An automatic switched bank fits factories with changing loads. A detuned reactor bank protects capacitor stages from harmonic resonance. A tuned filter targets defined fifth- or seventh-order harmonics. A dry-type film capacitor offers clean indoor installation and low maintenance. An oil-filled capacitor suits demanding outdoor or high-temperature locations. A hybrid bank combines staged correction with active harmonic control.
The U.S. Department of Energy reports that motor-driven equipment can represent more than half of industrial electricity use. Small errors therefore become expensive. For welding lines, cranes, and variable-speed drives, plain fixed capacitors may perform poorly. Rapid load changes can create switching stress. Harmonic-rich sites need measured impedance, not guesswork. I have seen oversized banks raise voltage during idle periods. That result is correctable, but only after reviewing load profiles. Select voltage ratings, discharge devices, enclosure protection, and thermal limits against local conditions.
Tips: Record 24-hour kW, kVAR, voltage, and harmonic readings before selecting equipment. Leave headroom for expansion. Check the capacitor’s kvar output at actual system voltage. Review IEC 60831 requirements and applicable utility rules. A detuned design is often safer than a cheaper untuned bank, though not always. Recheck performance after commissioning, because one imperfect measurement can distort the entire design.
| Option | Capacitor Construction | Typical Rated Voltage | Typical Reactive Power Range | Frequency | Best-Fit Application | Key Advantages | Important Selection Considerations |
|---|---|---|---|---|---|---|---|
| 1. Single-Phase LV Shunt Capacitor | Metallized polypropylene film, self-healing, dry-type construction | 230–480 V AC | Approximately 1–10 kvar per unit | 50 or 60 Hz | Small motors, lighting circuits, appliance loads, and individual power-factor correction | Compact size, simple installation, low maintenance, and suitable for distributed correction | Verify phase-to-neutral or phase-to-phase connection, inrush current, discharge requirements, and enclosure temperature |
| 2. Three-Phase Cylindrical LV Capacitor | Metallized polypropylene film with self-healing segments and internal discharge resistors | 400–525 V AC | Approximately 5–50 kvar per unit | 50 or 60 Hz | Main distribution boards, commercial buildings, pumps, fans, and standard industrial loads | Easy modular replacement, high energy density, and compatibility with automatic capacitor banks | Use a suitable contactor or switching device; allow for voltage tolerance, harmonics, ventilation, and at least the specified discharge time |
| 3. Heavy-Duty LV Power Capacitor | Reinforced metallized polypropylene film, self-healing dielectric, dry or low-loss construction | 440–690 V AC | Approximately 5–30 kvar per unit | 50 or 60 Hz | Industrial plants with long operating hours, variable loads, and frequent capacitor switching | Higher overload capability, improved thermal endurance, low dielectric losses, and longer service life | Select according to RMS current, ambient temperature, switching frequency, harmonic loading, and required overload class |
| 4. Detuned Capacitor Bank Element | LV power capacitor combined with a series detuning reactor | Typically 400–690 V AC | Approximately 5–50 kvar per step | 50 or 60 Hz; common tuning points include 189 Hz or 210 Hz on 50 Hz systems | Facilities containing variable-frequency drives, rectifiers, UPS systems, welders, and other nonlinear loads | Reduces the risk of harmonic resonance and limits harmonic current entering the capacitor bank | Reactor tuning must match the system harmonic spectrum; the bank may provide less fundamental-frequency kvar than an undetuned bank of the same capacitor rating |
| 5. Tuned Harmonic-Filter Capacitor | Capacitor designed as part of a tuned series LC filter, normally with a dedicated reactor | Approximately 400–690 V AC for low-voltage systems | Approximately 5–100 kvar per filter step | Tuned to a selected harmonic frequency, such as the 5th or 7th | Industrial networks requiring both power-factor correction and targeted harmonic mitigation | Provides reactive compensation while diverting selected harmonic currents away from sensitive equipment | Requires a harmonic study, accurate reactor-capacitor matching, protective coordination, and checking for possible resonance with the utility network |
| 6. Medium-Voltage Shunt Capacitor | Metal-enclosed or internally fused capacitor unit using a dielectric system suitable for medium voltage | Approximately 2.4–12 kV AC | Approximately 50–500 kvar per unit | 50 or 60 Hz | Utility distribution feeders, medium-voltage motor installations, substations, and large industrial networks | Corrects reactive power near high-power loads, improves voltage support, and reduces feeder current | Requires medium-voltage switching, discharge devices, fuses, surge protection, grounding provisions, and appropriate clearances |
| 7. Fast-Switching Capacitor Bank Module | Low-voltage self-healing film capacitors switched by thyristors or other solid-state power electronics | Approximately 400–690 V AC | Approximately 5–100 kvar per step | 50 or 60 Hz; rapid switching response | Cranes, welding equipment, elevators, compressors, data facilities, and rapidly changing industrial loads | Fast response, minimal mechanical wear, reduced voltage transients, and accurate compensation for fluctuating loads | Requires heat dissipation, semiconductor protection, suitable switching control, and careful assessment of harmonic current and short-circuit conditions |
7 Best Compensation Capacitors for Power Factor Correction?
Comparing compensation capacitors requires more than checking kvar output. Match the rated voltage to the system’s actual voltage and switching conditions. A 480-volt network may experience damaging transients above its nominal value. IEC 60831 recommends checking voltage endurance, capacitance tolerance, and temperature limits. Higher kvar is not automatically better.
Durability depends on internal construction and operating stress. Look for self-healing dielectric technology, pressure-sensitive disconnects, and durable terminals. The capacitor should also include discharge resistors, reducing residual voltage after shutdown. That detail matters near maintenance panels. The U.S. Department of Energy reports that motor-driven systems use more than 70% of industrial electricity, making reliable correction equipment especially valuable (DOE, Industrial Motor Systems, 2022). Yet correction capacitors can amplify harmonics. A detuned reactor may be necessary where variable-speed drives are common.
Safety deserves equal weight. Compare short-circuit withstand ratings, enclosure protection, thermal limits, and certified test evidence. IEC 60831 specifies discharge performance, while IEC 61071 addresses power-electronics capacitors under demanding switching conditions. Field records should show operating temperature, switching frequency, and replacement history. Keep the evidence.
A practical mistake is sizing from one afternoon’s load reading. Loads change. Measure demand across production cycles, then allow sensible capacity margin. Review the result after installation, because real harmonic distortion may differ from the design estimate. That reflection can prevent premature failure.
Installing compensation capacitors requires more than matching voltage and kvar ratings. A qualified electrician should inspect the panel, load profile, and harmonic levels before selection. In field maintenance, loose terminals often reveal themselves through heat marks or a faint buzzing sound. Follow the manufacturer’s wiring diagram, maintain clearances, and tighten connections to the specified torque. Do not install capacitors in a sealed, overheated enclosure. Heat shortens service life.
Use suitable fuses, contactors, discharge resistors, and overcurrent protection. A capacitor can retain dangerous voltage after power is removed. Lock out the supply, wait the required discharge period, and verify zero voltage with a properly rated meter. Never trust appearance alone. Test it.
Harmonic-producing equipment may need detuned reactors or a different correction method. Without this review, resonance can damage capacitors and disturb sensitive equipment. During inspections, check swelling, oil leakage, discoloration, unusual noise, and rising cabinet temperature. Record capacitance, current, voltage, and power factor readings under normal load. Small changes matter. Cleaning dust from ventilation paths also helps, although it is easy to overlook. A perfect checklist does not exist; site conditions change, and past measurements may be incomplete. Recheck settings after major motor, drive, or transformer changes. If a capacitor trips repeatedly, do not simply increase the fuse rating. Find the fault, isolate the circuit, and obtain an engineering assessment before returning it to service.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

