How to Choose a 2026 Top OEM Rubber Seal O Ring Factory?

Choosing a 2026 Top OEM Rubber Seal O-Ring Factory requires more than comparing prices or browsing polished websites. The right partner must prove stable compound quality, accurate tooling, controlled production, and dependable delivery. A factory should explain its rubber formulation, hardness range, compression-set results, temperature limits, and media resistance clearly. Vague answers deserve caution.

Robert M. Flitney, a respected sealing engineer and author of Seals and Sealing Handbook, offers a useful principle: “Choose the seal for the application, not merely the material.” This idea remains highly practical. An EPDM O-ring may perform well with water, yet fail quickly in petroleum-based fluids. A poorly selected FKM compound may harden under unsuitable temperatures. Small details matter.

Look for an OEM Rubber Seal O-Ring Factory with documented inspection procedures and traceable batches. Ask whether technicians check dimensions with calibrated equipment. Request sample reports, material certificates, and realistic production tolerances. If the application serves automotive, hydraulic, food, medical, or industrial equipment, confirm relevant compliance capabilities before approval. Certifications help, but they do not replace factory evidence.

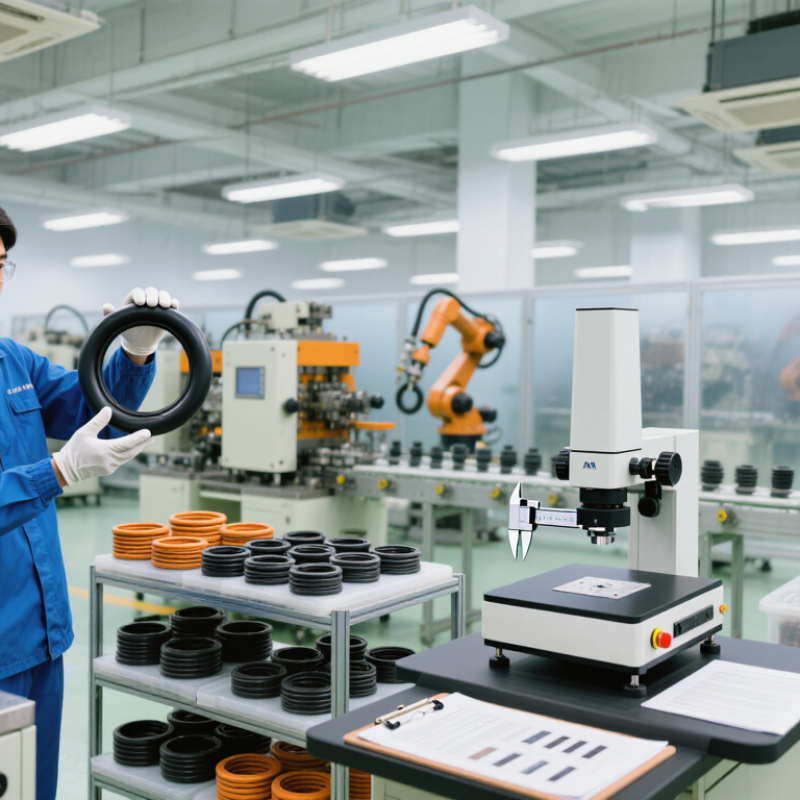
Walk through the process mentally. A mold closes. Rubber fills the cavity. Flash is removed. Each ring is inspected under bright light. That sequence should be controlled, repeatable, and measurable. Still, no supplier is perfect. Even experienced buyers can overlook packaging, storage humidity, or delayed engineering feedback. A strong factory admits possible weaknesses and explains how it corrects them. That honesty may reveal more than a perfect presentation.
How to Choose a 2026 Top OEM Rubber Seal O Ring Factory?

Define Your OEM Rubber Seal O-Ring Requirements and Application Conditions

Choosing a 2026 top OEM rubber seal O-ring factory starts with a clear application definition. A vague drawing creates costly revisions later. Specify the groove dimensions, inner diameter, cross-section, and acceptable tolerances. State whether the seal works in static or dynamic movement.

Operating Conditions Record the real operating conditions, not only the design values. Include temperature peaks, pressure cycles, fluid type, exposure time, and installation speed. Material selection depends on these details. Oils, fuels, steam, cleaning agents, and outdoor ozone can affect rubber differently. Hardness also matters because soft compounds seal uneven surfaces better, while harder compounds resist extrusion more effectively. Details matter.

Quality Verification and Field Feedback Ask the factory for compound data, batch traceability, dimensional inspection records, and sample validation. Request testing under conditions close to your equipment. A reliable manufacturer should explain compression set, swelling risk, aging behavior, and tolerance control in practical terms. Check packaging and storage guidance too. O-rings can deteriorate before assembly when exposed to heat, sunlight, or contamination. Small oversights remain common. A first specification is rarely perfect, and field feedback may reveal a groove problem rather than a material problem. Share installation photos, failure samples, and service history with the engineering team. This evidence helps the OEM factory adjust tooling, compound formulation, or inspection frequency without guessing.
Assess Material Quality, Standards, and Custom Formulation Capabilities

Choosing a 2026 OEM rubber seal O ring factory requires more than comparing prices. Material quality should be verified through batch records, traceability, and physical testing. Ask whether the factory controls hardness, tensile strength, compression set, and swelling resistance. A reliable supplier can explain test methods clearly. Vague answers deserve caution.

Inspect the rubber compound, not only the finished ring. Fluoroelastomer, silicone, EPDM, and nitrile suit different temperatures and fluids. The wrong formulation may look acceptable during assembly, then fail after repeated pressure cycles. Request samples from actual production batches. Check surface finish, flash, dimensional tolerance, and odor. Small defects matter.

Standards support confidence, but certificates never replace technical judgment. Confirm whether the factory follows relevant quality systems and maintains calibrated inspection equipment. Review process controls for mixing, molding, post-curing, and packaging. Custom formulation capability is equally important. Engineers should adjust polymer type, filler balance, hardness, and curing conditions for your working environment. Provide pressure, temperature, media, movement, and service-life data. Better inputs create better compounds.

I have seen teams approve a seal after one short test. That was a mistake. Long-term aging and compression recovery often reveal hidden weaknesses. A capable factory should welcome repeated testing and explain failures without hiding them. Still, no supplier is perfect. Communication gaps can remain, especially during formulation changes. Record every revision, test result, and approval before mass production.

How to Choose a 2026 Top OEM Rubber Seal O-Ring Factory

Material capability is a practical starting point when evaluating an OEM O-ring factory. The chart compares typical continuous service-temperature ranges for widely used elastomers. Actual limits depend on compound formulation, media compatibility, compression, pressure, and testing. A qualified supplier should support compound development and validation against requirements such as ISO 3601, ASTM D2000, ISO 815-1, ISO 37, and ISO 188.

Verify Manufacturing Equipment, Production Controls, and Testing Systems

Choosing a 2026 OEM rubber seal O-ring factory starts with the equipment behind its promises. During a supplier audit, inspect injection presses, rubber mixers, curing ovens, and automated trimming tools. A stable press should show consistent temperature, pressure, and cycle records. Ask to see maintenance logs, not only polished production samples. Missing records are a warning. Check mold storage, too. Clean, labeled molds usually reflect stronger process discipline.

Production controls reveal how reliably a factory repeats quality. Review material certificates, compound recipes, and batch identification methods. Each batch should connect to mixing, molding, inspection, and shipment records. Effective factories measure hardness, dimensions, flash, and surface defects during production. Statistical process checks can expose drift before defective seals reach customers. I have seen attractive samples hide weak traceability. That mistake can become expensive.

Testing systems deserve direct attention. Confirm whether the laboratory uses calibrated equipment for tensile strength, elongation, compression set, aging, and leakage tests. Test conditions should match the seal’s working temperature, pressure, fluid, and service time. Request recent reports with sample numbers, dates, methods, and acceptance limits. Do not accept vague claims like “tested successfully.” A practical factory should explain failures and corrective actions without defensiveness. One imperfect result is not automatically disqualifying. Repeated unexplained results are. Ask to witness a test, because documents alone cannot show every daily habit.

Compare Factory Experience, Capacity, Lead Times, and Quality Certifications

How to Choose a 2026 Top OEM Rubber Seal O Ring Factory?

Factory experience should be measured by evidence, not age alone. Ask how many years the team has produced comparable O rings, compounds, and tolerances. Experienced engineers can identify flash, shrinkage, compression set, and mold design risks before mass production. Request sample inspection reports and customer-approved drawings. A polished website proves very little.

Capacity must match your demand without weakening quality. Review machine numbers, mold availability, production shifts, and backup equipment. A factory producing millions of seals monthly may still struggle with a sudden custom order. Check whether raw materials are traceable by batch. Ask how rejected parts are isolated and recorded. These details reveal operational discipline.

Lead time needs separate estimates for sampling, tooling, approval, and production. A credible supplier explains each stage and provides realistic buffer time. Very short promises can hide rushed inspections. Sometimes, I have seen buyers focus on unit price and ignore delayed tooling; that decision becomes expensive later. Quality certifications, such as ISO 9001 or IATF 16949, add confidence, but certificates alone are insufficient. Verify their scope, validity, audit records, and daily use. Review dimensional reports, material test results, calibration records, and corrective-action responses. Then compare factories using the same checklist, because inconsistent questions create unreliable comparisons.

How to Choose a 2026 Top OEM Rubber Seal O Ring Factory? - Compare Factory Experience, Capacity, Lead Times, and Quality Certifications

Anonymized supplier comparison framework based on commonly verified OEM rubber-seal manufacturing requirements

Evaluation Dimension Anonymized Factory A Anonymized Factory B Anonymized Factory C What Buyers Should Verify
Operating history 15+ years 8–15 years 3–8 years Business registration, production records, customer references, and continuity of operations
OEM rubber-seal experience High; custom tooling, compound development, and drawing-based production Medium to high; standard and moderately customized parts Medium; mainly standard O rings and simple profiles Approved drawings, tolerance capability, tooling ownership, and first-article records
Typical material capability NBR, EPDM, FKM, silicone, HNBR, and custom compounds NBR, EPDM, FKM, silicone, and selected specialty compounds NBR, EPDM, FKM, and silicone Polymer type, hardness, temperature range, media compatibility, and compound traceability
Annual O-ring capacity Approximately 80–150 million pieces Approximately 30–80 million pieces Approximately 10–30 million pieces Molding-machine count, mold utilization, staffing, shift pattern, and confirmed available capacity
Typical monthly capacity utilization 60–80% 65–85% 70–90% Current order loading, seasonal peaks, maintenance downtime, and reserved capacity
New mold development 15–30 calendar days 20–40 calendar days 30–60 calendar days Design approval, steel availability, trial schedule, revision policy, and mold maintenance responsibility
Prototype lead time 7–15 working days after drawing and compound approval 10–20 working days after drawing and compound approval 15–25 working days after drawing and compound approval Whether lead time includes tooling, inspection, documentation, and sample shipping
Standard production lead time 15–25 working days after approval 20–35 working days after approval 25–45 working days after approval Order size, compound availability, production queue, inspection time, and shipment terms
Dimensional inspection Digital vision systems, profile projectors, gauges, and sampling plans Profile projectors, gauges, calipers, and documented sampling plans Manual gauges and basic dimensional inspection Calibration certificates, inspection frequency, measurement uncertainty, and retained records
Material and performance testing Hardness, tensile strength, elongation, compression set, aging, and fluid-resistance testing Hardness, tensile strength, elongation, compression set, and selected aging tests Hardness and basic physical-property testing; external testing for special requirements Test methods, acceptance limits, laboratory capability, and third-party reports where required
ISO 9001 quality management Certified Certified Verify current certificate Certificate scope, issuing body, validity dates, site address, and audit status
IATF 16949 automotive quality system Available for automotive programs Verify program scope Not confirmed Required only when specified by the customer or automotive supply chain
ISO 14001 environmental management Certified Verify current certificate Not confirmed Environmental objectives, waste handling, restricted substances, and certificate scope
Regulatory documentation Can provide applicable declarations and test reports Available for selected compounds and applications Usually arranged through external laboratories Confirm application-specific requirements such as food contact, drinking water, medical, or automotive compliance
Traceability system Compound batch, production lot, mold, operator, and inspection records Compound batch, production lot, and inspection records Basic batch and shipment records Retention period, recall process, certificate of analysis, and lot identification on packaging
Best-fit project profile High-volume, safety-critical, automotive, industrial, and highly customized applications Medium-volume OEM programs requiring balanced cost, capability, and lead time Standard O rings, lower-volume orders, and cost-sensitive applications with simpler requirements Match supplier capability to risk level, annual demand, certification needs, and delivery urgency

Recommended supplier-selection checks

Request current certificates, audit the production site, approve the rubber compound and drawing, validate first articles, review inspection records, and obtain a written production schedule before placing a 2026 OEM order. Capacity and lead-time figures should be confirmed for the specific part number, compound, quantity, packaging requirement, and delivery destination.

Evaluate Pricing, Communication, Sample Approval, and Long-Term Support

How to Choose a 2026 Top OEM Rubber Seal O Ring Factory?

Price should start the evaluation, not end it. The 2024 Freedonia industry analysis shows that demand for industrial rubber products remains tied to transportation, machinery, and industrial equipment production. That pressure encourages factories to quote aggressively. However, a low unit price may hide tooling fees, inspection costs, or unstable compound quality. Request a complete quotation with material grade, tolerance, packaging, mold ownership, and delivery terms. Compare total cost over twelve months.

Communication is easier to test than promised. Send a technical drawing with one unclear tolerance. Observe whether the factory asks precise questions. Good engineers should discuss ISO 3601 dimensions, compression set, temperature range, and media compatibility. Keep every change in a written approval record. Short replies are not always efficient.

Sample approval needs measurable evidence. Ask for compound certificates, dimensional reports, hardness results, and aging data. The 2023 Rubber Industry Report by Smithers highlights continuing demand for higher-performance elastomers in demanding industrial applications. A sample that seals today may fail after heat, pressure, or chemical exposure. Test under realistic conditions. Do not approve only by appearance.

Long-term support deserves equal weight. Check spare-mold planning, batch traceability, corrective-action speed, and engineering response after delivery. A factory should explain its backup process honestly. No factory is perfect. During one supplier review, a delayed report revealed weak internal coordination, but the team corrected it transparently. That response mattered more than a polished presentation. Reliability grows through repeated evidence, not confident promises.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.