


2026 Top Galvanized Tube Types for Global Buyers

Global buyers need more than a bright zinc surface when selecting a Galvanized Tube. They must compare coating method, steel grade, wall thickness, dimensions, and intended service conditions. A tube used for greenhouse frames may face different demands from one installed in outdoor handrails or water-support structures. This guide introduces the leading galvanized tube types expected to shape international purchasing in 2026.

Hot-dip galvanized tubes remain widely valued for their thick, durable zinc coating and strong outdoor performance. Pre-galvanized tubes often offer cleaner dimensions and efficient pricing for light fabrication. Electro-galvanized options can provide a smoother appearance, but they may require additional protection in harsh environments. Welded tubes suit many structural applications, while seamless tubes may be considered where pressure, stress, or specification requirements are more demanding. The right choice depends on evidence, not appearance alone.

Standards matter. Buyers should confirm relevant ASTM, EN, ISO, or regional requirements before approving samples. They should also review mill certificates, coating thickness reports, welding quality, dimensional tolerances, and corrosion-test results. Experienced suppliers can explain how zinc coverage changes at corners, weld seams, and cut ends. Small details matter.

No single type wins every project. That assumption deserves review. Shipping distance, moisture exposure, fabrication methods, and local inspection practices can change the decision. Product data should be checked against the final application, not copied from a previous order. Even reliable suppliers can make mistakes when specifications remain vague. A disciplined comparison helps global buyers balance service life, cost, availability, and technical risk.
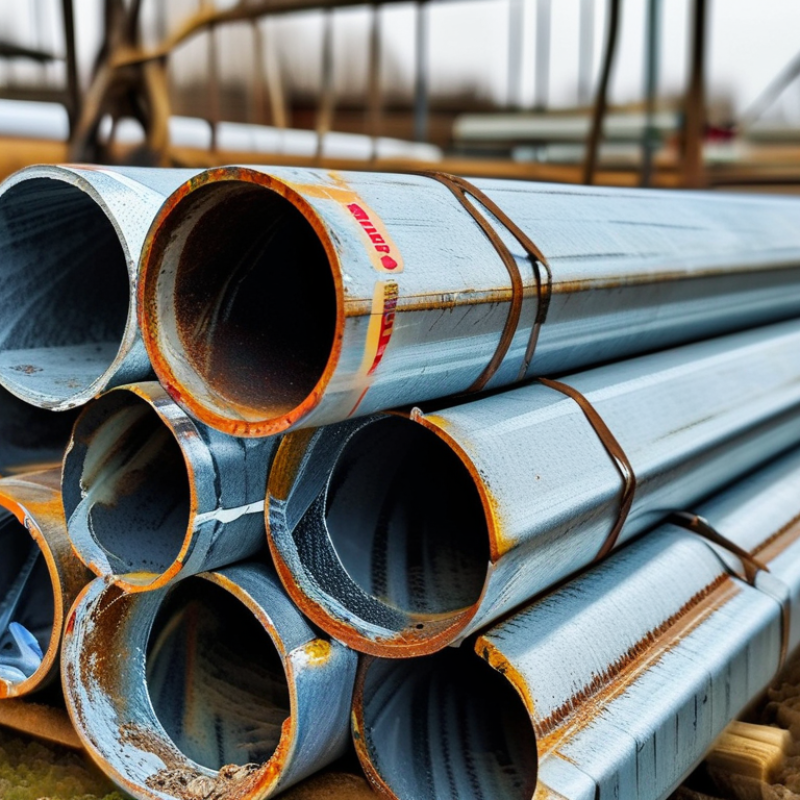
2026 Top Galvanized Tube Types for Global Buyers

Galvanized Tube Basics and Key Features for Global Buyers

Galvanized Tube Basics and Key Features for Global Buyers

Galvanized tubes use a zinc coating to slow corrosion on steel surfaces. For global buyers, coating method matters as much as tube size. Hot-dip galvanizing usually creates a thicker, more durable layer for outdoor structures. Electro-galvanizing offers a smoother finish but may provide less protection in severe environments. The choice should match exposure, service life, and budget. No coating is perfect.

A dependable specification starts with the steel grade, outside diameter, wall thickness, and tube length. Buyers should confirm whether measurements follow metric or imperial systems. Coating mass, adhesion, and surface appearance also need clear requirements. Inspection documents can include chemical analysis, tensile results, dimensional checks, and coating tests. Ask for batch traceability. This detail is easy to miss.

Environmental exposure changes performance significantly. Indoor, dry applications may need less protection than coastal or industrial sites. Salt, moisture, and trapped water can attack cut edges and welded areas. Proper drainage and sealed connections reduce these risks. Threading or drilling after galvanizing may expose bare steel, so repair treatment should be specified. A common assumption deserves reconsideration: a bright surface does not always indicate a thicker zinc layer. Buyers should compare test results rather than relying on appearance alone. Supplier communication can still fail when drawings, tolerances, and inspection terms remain vague.

2026 Top Galvanized Tube Types for Global Buyers - Galvanized Tube Basics and Key Features for Global Buyers
Galvanized Tube Type Manufacturing and Zinc-Coating Method Common Size Range Typical Zinc-Coating Information Key Advantages Common Global Applications Relevant Standards to Check Important Buyer Considerations
Hot-Dip Galvanized Round Structural Tube Steel tube is fabricated first and immersed in molten zinc, producing a metallurgically bonded coating on the external and accessible internal surfaces. Common supply range: approximately 12.7–219.1 mm outside diameter and 0.8–8.0 mm wall thickness, depending on production capability and structural specification. Coating requirements are normally specified by zinc mass or thickness. Minimum local coating thickness is commonly about 45–85 μm, depending on the steel thickness and governing standard. Strong long-term atmospheric corrosion protection; suitable for outdoor service; the coating protects exposed steel through barrier and sacrificial action. Outdoor frames, guardrails, agricultural structures, solar-support components, fences, walkways and general construction. ISO 1461EN ISO 1461ASTM A123/A123MASTM A500 Confirm whether the structural tube specification and the galvanizing specification are both required. Check vent and drain-hole design, thread protection, straightness and post-galvanizing dimensional tolerances.
Pre-Galvanized ERW Round Tube Cold- or hot-rolled steel strip is zinc-coated in coil form and then roll-formed and welded into tube. Common supply range: approximately 10–165 mm outside diameter and 0.6–3.2 mm wall thickness. Common coating designations include Z120–Z275 g/m² total on both surfaces, equivalent to approximately 8–19 μm per side when evenly distributed. Consistent surface appearance, efficient production, competitive cost and good protection for normally exposed surfaces. Light structural work, greenhouse components, shelving, furniture frames, cable support systems, interior construction and general fabrication. EN 10346ASTM A653/A653MJIS G3302 Forming and welding can expose small areas at the seam or cut ends. Specify repair treatment for damaged areas and assess suitability for continuously wet, buried or highly corrosive environments.
Pre-Galvanized Square and Rectangular Hollow Section Zinc-coated strip is roll-formed into square or rectangular hollow sections, usually using electric resistance welding. Common supply range: approximately 15 × 15 mm to 200 × 200 mm square; rectangular sections commonly range from about 20 × 10 mm to 200 × 100 mm, with 0.8–8.0 mm wall thickness. Typical commercial coating levels are about Z120–Z275 g/m² total on both sides; actual coating class depends on the ordered material grade and applicable standard. Efficient load distribution, easy fabrication, clean appearance and convenient flat surfaces for mounting or connection. Racking, partition frames, machinery guards, fencing, construction subframes, signage supports and light structural assemblies. EN 10346EN 10219ASTM A500ASTM A653/A653M Check corner radius, squareness, weld-zone appearance, diagonal dimensions and the condition of cut ends. For heavy outdoor exposure, a post-fabrication hot-dip coating may provide more complete coverage.
Hot-Dip Galvanized Square and Rectangular Structural Tube Square or rectangular hollow section is fabricated and then hot-dip galvanized after forming and welding. Common supply range: approximately 20 × 20 mm to 300 × 300 mm square and up to about 400 × 200 mm rectangular, with wall thicknesses commonly from 1.5–12 mm. Coating thickness is determined by the steel thickness and the applicable galvanizing standard; typical minimum local values are often about 45–85 μm. High durability for outdoor environments, better coverage of fabricated surfaces than pre-galvanized material and reduced need for repeated painting. Bridges and access platforms, outdoor stairs, highway furniture, utility supports, agricultural buildings and coastal or industrial structures. ISO 1461EN ISO 1461ASTM A123/A123MEN 10219 Provide suitable vent and drain holes for closed sections. Allow for zinc buildup at corners and threaded areas, and verify lifting, handling and weld-repair procedures.
Electro-Galvanized Precision Tube A zinc layer is deposited electrochemically after tube production, generally providing a smooth and uniform appearance. Common supply range: approximately 6–100 mm outside diameter and 0.5–3.0 mm wall thickness. Typical commercial coating thickness is approximately 5–25 μm, although the specified class may vary significantly by product standard and corrosion requirement. Good dimensional control, smooth finish, suitable for indoor or mildly exposed applications and convenient for further forming or painting. Automotive components, interior equipment, furniture, appliances, light-duty frames and precision fabricated parts. ISO 2081ASTM B633EN 10152 Usually less suitable than hot-dip galvanizing for severe outdoor, marine, buried or continuously wet service. Confirm passivation, salt-spray performance, surface class and post-forming corrosion protection.
Rigid Galvanized Steel Electrical Conduit Steel conduit is zinc-coated to protect the raceway from corrosion; the coating arrangement can vary between external-only and external-plus-internal protection. Common nominal sizes are approximately 16–63 mm, with wall thickness commonly around 1.2–3.5 mm, depending on the conduit classification. Coating requirements depend on the conduit system. Hot-dip galvanized conduit generally provides a thicker, more durable coating than electro-galvanized conduit. Mechanical protection for cables, fire-resistant metallic raceway, grounding continuity when correctly installed and good suitability for exposed installations. Industrial buildings, commercial electrical systems, infrastructure projects, exposed cable routes and areas requiring robust mechanical protection. IEC 61386-21IEC 61386-1EN 61386-21 Check nominal size, thread form, coupling compatibility, internal burr control, corrosion category, grounding requirements and local electrical-code acceptance.
Galvanized Mechanical Tube for Fabrication Low-carbon or alloy steel tube is produced for forming and fabrication, then supplied with either pre-galvanized or electro-galvanized protection. Common supply range: approximately 8–120 mm outside diameter and 0.7–5.0 mm wall thickness. Coating levels vary by process and purchase specification; pre-galvanized products commonly use Z120–Z275 g/m² total coating, while electro-galvanized products often use thinner zinc layers. Good weldability and formability when the steel grade is selected correctly; suitable for repeatable component production. Automotive brackets, equipment frames, seating structures, agricultural machinery parts, racks and fabricated assemblies. EN 10346ISO 2081ASTM A653/A653MASTM B633 Confirm steel chemistry, yield strength, elongation, bending radius, weld procedure, coating damage after fabrication and requirements for zinc-fume control during welding.
Galvanized Water and Utility Pipe Steel pipe is normally hot-dip galvanized after manufacture, with zinc applied to the exterior and, where specified, the interior. Common nominal pipe sizes range from approximately 15–150 mm, with wall thickness selected according to the pressure, service and regional pipe classification. Coating requirements should be defined by the relevant pipe or galvanizing standard. Actual internal coverage and coating continuity must be verified separately. Useful for certain utility, service and non-potable applications where mechanical strength and corrosion protection are required. Compressed-air lines, agricultural utilities, fire-protection-related systems where approved, temporary services and non-potable water systems. ISO 1461EN ISO 1461ASTM A123/A123MEN 10255 Do not assume suitability for drinking water, hot water or chemical service. Confirm local health regulations, pressure rating, fluid compatibility, threaded-end protection and internal corrosion risk.
Buyer note: Size ranges, coating values and standards shown are common reference ranges rather than universal limits. Final purchasing documents should specify outside diameter or nominal size, wall thickness, steel grade, coating mass or thickness, test requirements, tolerances, surface condition, packing and the destination-market compliance requirements.

Main Galvanized Tube Types Available in the 2026 Market

2026 Top Galvanized Tube Types for Global Buyers

Main Galvanized Tube Types Available in the 2026 Market

Hot-dip galvanized round tubes remain popular for outdoor structures, fencing, handrails, and agricultural frames. Steel tubes receive a zinc coating after fabrication, including welded areas and external surfaces. This process usually provides stronger protection than basic pre-galvanized material. Buyers should check coating weight, wall thickness, weld quality, and dimensional tolerance. A bright surface is not automatically better.

Pre-galvanized tubes use zinc-coated steel strip before forming. They are often lighter, cleaner, and more economical for indoor frames, furniture parts, cable supports, and general fabrication. However, cut edges and new welds may need additional protection. This detail is often missed. It can matter in humid warehouses or coastal projects.

Square and rectangular galvanized hollow sections suit gates, structural frames, shelving, and equipment supports. Their flat faces simplify cutting and assembly. Round tubes remain easier to bend and drain during outdoor use. Mechanical tubes may require tighter outside-diameter tolerances, while structural sections focus more on load performance. Buyers should compare ASTM, EN, JIS, or local specifications carefully, because similar sizes may not share the same wall thickness. In practical inspections, measure several points along the tube, examine the weld seam, and test packaging against moisture. Specifications are sometimes incomplete, and that deserves a second look.

How Coating Methods Affect Tube Performance and Service Life

2026 Top Galvanized Tube Types for Global Buyers

How Coating Methods Affect Tube Performance and Service Life

Galvanized tubes do not all age in the same way. Hot-dip galvanizing creates a thicker zinc layer and protects exposed steel through sacrificial action. It suits outdoor frames, agricultural supports, and humid construction sites. In field inspections, I often find small scratches are less serious than trapped moisture inside poorly drained tubes. Drainage matters.

Electro-galvanizing applies a thinner, more uniform coating. It offers a cleaner surface and tighter dimensional control, which helps indoor assemblies and light-duty components. However, its thinner zinc layer may lose protection sooner in coastal air or areas with road salt. Zinc-rich coatings can repair damaged zones, but surface preparation decides the result. A dusty or oily surface will weaken adhesion. No coating choice is perfect.

Tips: Ask for coating thickness records, steel grade, tube dimensions, and test results before purchasing. Check whether the coating standard matches the destination market. Examine cut ends, weld areas, and drilled holes, because these points often need extra protection. Also, confirm packaging prevents trapped water during sea transport. This detail is easy to miss. A reasonable buyer should compare expected exposure, maintenance access, and service life rather than choosing the thickest coating automatically. Manufacturers should document preparation methods and inspection conditions clearly. Some assumptions remain uncertain, especially when local pollution, condensation, and handling damage vary between projects.

Choosing Galvanized Tubes by Application, Standards, and Environment

2026 Top Galvanized Tube Types for Global Buyers

Choosing galvanized tubes requires more than comparing prices or zinc appearance. Application, standards, and environment must be evaluated together. The World Steel Association reported global steel demand of about 1.75 billion tonnes in 2024, showing the scale of infrastructure and manufacturing needs. Yet, not every tube suits every project.

For outdoor frames, agricultural structures, and general fabrication, hot-dip galvanized tubes offer a thick, bonded zinc layer after fabrication. ASTM A123 and ISO 1461 provide useful coating requirements, while ASTM A500 and ASTM A53 address common structural and pipe specifications.

Continuous galvanized tubes can provide cleaner dimensions and smoother surfaces. They may fit indoor systems or lightly exposed applications better.

Measure the coating.

Environmental selection is equally important. Zinc durability guidance indicates corrosion rates can remain below 1 micrometre per year in many rural atmospheres. Coastal salt, humidity, and industrial pollutants can increase loss significantly. ISO 12944 exposure categories help buyers compare atmospheric risks, although the standard mainly supports coating-system planning, not every tube purchase.

For C4 or C5 conditions, specify additional protection, sealed tube ends, drainage holes, and compatible paint systems.

That shortcut fails.

A shiny surface does not prove long service life. Buyers should request coating mass, wall thickness, weld condition, test certificates, and traceability before approval. Specifications still need local review.

Global Buying Factors: Quality, Cost, Supply, and Compliance

Global buyers usually compare galvanized tubes by quality, cost, supply stability, and compliance. Hot-dip galvanized tubes suit outdoor structures because their zinc coating handles moisture well. Pre-galvanized tubes can reduce cost for lighter indoor applications. Seamless tubes may support demanding pressure work, but they often require higher budgets.

In my sourcing reviews, I check coating thickness, wall tolerance, weld appearance, and tube straightness. Mill certificates and batch traceability help verify these details. A low quote can hide weak packaging, inconsistent dimensions, or limited inspection records. Delivery capacity matters too. Ask for production schedules, loading photos, and realistic lead times.

Cheap is not always efficient.

Tips: Request samples from the actual production batch. Compare coating reports with your project requirements. Confirm the destination’s accepted standards before ordering. Check packing against sea moisture and rough handling. Keep one independent inspection step, even when the supplier seems reliable. No checklist is perfect. I still review rejected pieces, because recurring small defects often reveal larger process problems. Compliance should cover material records, marking, testing, and customs documents. Requirements differ by market, so written confirmation is safer than assumptions.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.


