


Choosing a Standing Pouch Making Machine in 2026 takes more than comparing advertised speeds. Flexible packaging is a large and evolving market. Grand View Research estimated its global value at USD 261.5 billion in 2023 and projected a 4.8% compound annual growth rate from 2024 to 2030. That figure describes the wider flexible packaging market, not pouch-making equipment sales. Still, it signals why manufacturers are examining pouch formats, materials, and production capacity.
The right machine depends on the pouch you actually need to make. Consider pouch dimensions, zipper or spout options, film structure, sealing method, and changeover time. Then check whether the quoted output applies to your material and product—not just an ideal test run. Ask suppliers for a factory trial using your film, and inspect seal consistency, waste levels, and finished pouches. Small details matter. A pouch that looks neat on a display can fail at the seal.
Service matters, too. Confirm spare-parts availability, operator training, and support response times before ordering. Compare these details with your production plans and budget. Be cautious with broad performance claims; real output can shift with film, settings, and operator experience. A machine may look impressive. Your own trial data is more useful. No checklist removes every risk, but careful testing can reveal weak points before installation.
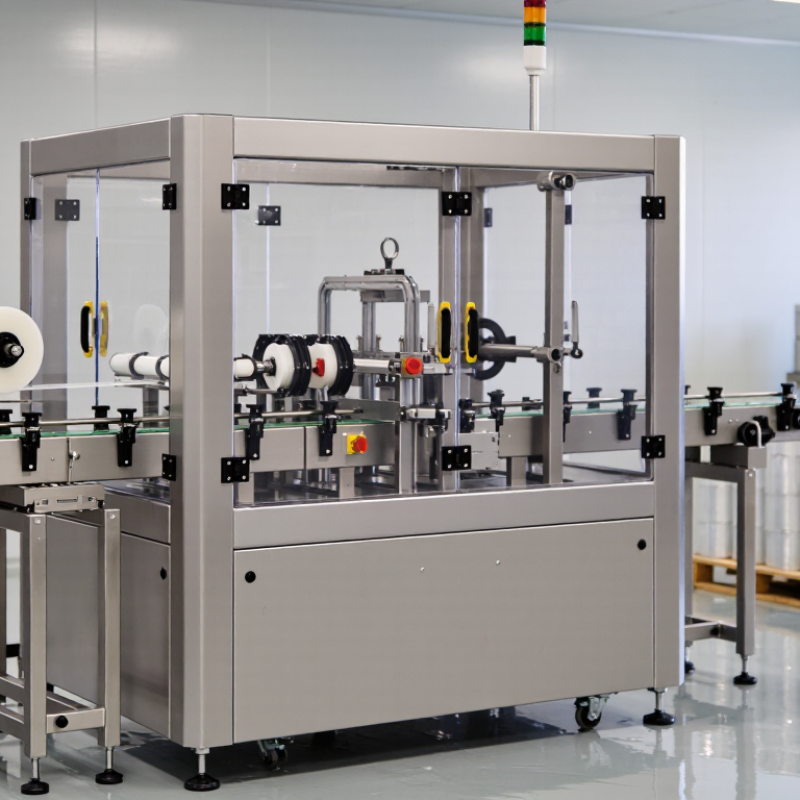
Standing pouch machines usually fall into two practical groups: premade-pouch fillers and rollstock form-fill-seal systems. A premade-pouch machine takes finished bags from a magazine, opens them, fills them, and seals the tops. It suits varied pouch designs and shorter production runs. Rollstock equipment forms pouches from a continuous film web, then fills and seals them. It can reduce pouch costs at higher volumes, but setup and changeovers may take longer.
Know your product first. Powder can cling to seals; chunky foods need a wider filling path. A typical line grips each pouch, opens it with air or suction, doses the product, then heat-seals and cools the top. Simple steps, but small faults matter. A crooked zipper or dusty seal area can cause leaks. Ask suppliers to test your actual pouch material and product, not just a sample film. Check achievable speed, filling accuracy, cleaning access, and options such as zipper or spout handling. Leave room for operator adjustments. Real production is rarely as tidy as a brochure suggests.

Choosing a standing pouch making machine starts with the pouch formats you actually plan to produce. Record the pouch width, height, bottom-gusset depth, and zipper position. A 500-gram pouch may look simple, but a wider base can change forming and sealing settings. Measure real samples, not only drawings. Small differences matter.
Next, match the machine to the packaging material. Laminated films can vary in thickness, stiffness, and seal behavior. Ask suppliers for material specifications, then test the exact film structure under production conditions. Check seal strength, edge alignment, and whether the film tracks smoothly through forming rollers. One test is not enough. Humidity and roll tension can also affect results, so leave room for adjustment.
Estimate output using your expected product mix, rather than the highest advertised speed. A line running one pouch size may perform differently when operators change formats or refill film rolls. Consider changeover time, required operators, and available floor space. If future demand is uncertain, avoid choosing capacity based on optimistic forecasts alone. That assumption is easy to make, and harder to undo. Share sample pouches, film rolls, and realistic hourly targets when requesting a machine trial.
| Pouch Format | Typical Size or Feature | Common Material Structure | Suitable Machine Setup | Indicative Output Planning Range | Key Selection Checks |
|---|---|---|---|---|---|
| Standard stand-up pouch | Small to medium formats; bottom gusset allows the filled pouch to stand upright | PET/PE, PET/CPP, or other product-compatible laminate structures | Premade-pouch filling and sealing machine, or rollstock form-fill-seal equipment | Premade-pouch systems often run at tens of pouches per minute; rollstock systems may achieve higher rates depending on lanes and product | Confirm pouch width, height, gusset depth, sealing area, and product dosing method |
| Stand-up pouch with zipper | Resealable opening; zipper position and width must match the pouch design | Heat-sealable laminated film with a compatible zipper profile | Premade-pouch machine with zipper-opening and pouch-mouth handling features; rollstock line with zipper insertion where required | Typically lower than a comparable pouch without a zipper because opening, filling, and sealing require additional handling | Test zipper opening, filling clearance, seal placement, and zipper integrity after sealing |
| Stand-up pouch with spout | Spout and cap positioned at a corner or near the center of the top seal | Flexible barrier laminate selected for the liquid or semi-liquid product | Premade-pouch filler with spout handling, or a pouch-forming line with spout insertion and welding capability | Depends on spout insertion, filling viscosity, and leak-test requirements; validate with production trials | Check spout dimensions, insertion method, weld strength, cap fit, and leak-test procedure |
| Quad-seal or box-bottom pouch | Structured base and side seals create a more box-like pack appearance | Printable outer layer, barrier layer if needed, and heat-sealable inner layer | Machine specifically configured for the required panel, gusset, and seal layout | Often requires more forming and sealing steps than a basic stand-up pouch; confirm speed with the exact format | Verify forming geometry, seal-jaw configuration, registration, and changeover requirements |
| High-barrier pouch | Used when oxygen, moisture, aroma, or light protection is important | Structures may include metallized film, foil, or barrier-coated layers with a sealant layer | Machine with temperature, pressure, and dwell-time controls suited to the selected laminate | Line speed depends on the laminate’s sealing window and required seal inspection | Confirm barrier needs with the product and shelf-life specification; test seals on the actual film |
| Recyclability-oriented mono-material pouch | Designed around a single primary polymer family where suitable collection and recycling systems exist | Compatible PE-based or PP-based film structures, subject to pack design and application | Machine with adjustable sealing settings and film-tension control for the selected structure | Establish speed through trials because seal behavior can differ from conventional laminates | Check seal strength, stiffness, barrier performance, machineability, and local recycling guidance |
| Short runs or frequent product changes | Multiple pouch sizes, recipes, or artwork versions with regular changeovers | Varies by product; material specifications should be documented for each SKU | Flexible setup with accessible change parts, recipe storage, and straightforward cleaning | Assess usable production time as well as rated speed; setup and cleaning affect daily output | Compare changeover time, operator requirements, dosing flexibility, and cleaning access |
| High-volume production | Stable pouch format and product with sustained demand | Qualified film structure with consistent roll or premade-pouch supply | Automated feeding, dosing, sealing, discharge, and inspection matched to the production line | Set the target from required good pouches per hour, planned shifts, and expected downtime | Request a trial using the intended pouch, film, product, and inspection criteria; confirm achievable good output |
Planning note: Output figures are application-dependent, not guaranteed machine ratings. Actual performance varies with pouch dimensions, film properties, product flow, filling accuracy, operator practices, inspection requirements, and changeovers. Compare equipment using tested good pouches per minute on the intended production setup.
When comparing a standing pouch making machine, look beyond its advertised speed. Ask for sustained output using your pouch size and actual film structure. A line rated at 120 pouches per minute may run slower when seals need extra cooling or film tension changes. Check pouch width and length ranges, film thickness limits, sealing temperature control, and changeover time. Small details matter.
Compare how each machine controls registration, web tension, and sealing pressure. Photoelectric sensors can correct print alignment, while automatic tension control helps prevent wrinkles and uneven feeding. Ask whether operators can save settings for repeat jobs. Useful alarms should identify problems clearly, not just flash a fault code. Simple controls help.
Automation can reduce routine adjustments, but it cannot fix poor setup or inconsistent material. Request a demonstration with a representative laminate, then inspect seal edges, dimensions, and reject rates across a sustained run. Check whether format changes need tools, and how long a trained operator needs to complete one. These are practical measures, though factory conditions may not match your floor. I would also ask about spare-part availability, maintenance access, and operator training before comparing prices. A cheaper machine may need more hands-on attention than expected.
For a 2026 standing pouch making machine, judge quality with the pouch you actually plan to produce. Ask for a run using your film, pouch dimensions, and target speed. Inspect seal consistency, zipper alignment, cutting edges, and finished pouch dimensions. A clean sample matters. So does a stable run, not just a brief demonstration.
Safety deserves a close look. Check whether guards cover moving parts and whether emergency stops are easy to reach. Ask how operators access the machine during cleaning or changeovers. Clear instructions and practical training reduce mistakes on busy shifts. Details matter. A polished control screen alone is not proof of safe operation.
Service and total cost of ownership can change the buying decision. Confirm technician availability, spare-part lead times, warranty coverage, and remote support hours. Then estimate energy use, routine maintenance, film waste, and downtime over several years. Compare those costs with the purchase price. I would leave room for uncertainty: production estimates can look precise, but changeovers and operator learning often take longer than expected. Request a written cost breakdown and verify its assumptions against your planned schedule.
A machine’s specifications tell only part of the story. Ask the supplier to run your actual film, pouch dimensions, zipper, and filling requirements. Inspect finished samples for seal consistency, pouch shape, cutting accuracy, and easy opening. Check several pouches from different points in the run, not just one perfect sample. Small details matter. A slightly uneven seal may become a costly problem during longer production.
Plan a witnessed test using your intended materials and realistic operating speeds. Record changeover time, reject rate, and output over a continuous run. Ask how operators adjust temperature, pressure, and film tension, and whether those settings are saved between jobs. A short demonstration can hide interruptions. That said, even a longer test cannot reproduce every condition at your facility, so treat results as evidence, not a guarantee.
Tips: Share site dimensions, power supply, air requirements, and floor access before installation. Confirm who handles commissioning, operator training, and acceptance checks. Keep a sample roll and finished pouches for later comparison. If a test result seems unusually clean, ask what was adjusted; I would not rely on appearance alone.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

