2026 Top Hex Socket Bolt Types for Global Buyers
Global buyers need more than a familiar drive shape when selecting a Hex Socket Bolt. They must match the bolt with the joint, load, environment, and production standard. A socket head cap screw may suit compact machinery, while a button head version offers a smoother external profile. Countersunk designs sit flush with panels. Low-head and shoulder types solve tighter clearance problems, but they may provide less usable thread engagement.
Dr. John H. Bickford, a respected fastener engineering author, states, “A bolt is only one element of a bolted joint.” That warning remains practical in 2026. Buyers should review tensile strength, proof load, hardness, thread tolerance, drive depth, and dimensional compliance. ISO 4762 is commonly associated with socket head cap screws, yet regional specifications and customer drawings may differ. Never treat a certificate as a complete quality guarantee. Traceability, sampling, inspection records, and supplier process control still matter.
Material choice changes performance. Alloy steel supports demanding mechanical loads. Stainless steel helps resist corrosion, although it can face galling during installation. Zinc, black oxide, and specialized coatings offer different protection levels. The right option depends on humidity, temperature, chemicals, and maintenance access. Small details matter here. A shallow socket can slip under torque. An unsuitable coating can alter thread fit. A beautiful finish may hide poor control.
This guide compares the leading Hex Socket Bolt types for international purchasing teams. It considers design, strength, corrosion resistance, standards, application fit, and sourcing risk. Some choices will remain imperfect. That is why careful verification beats assumptions.
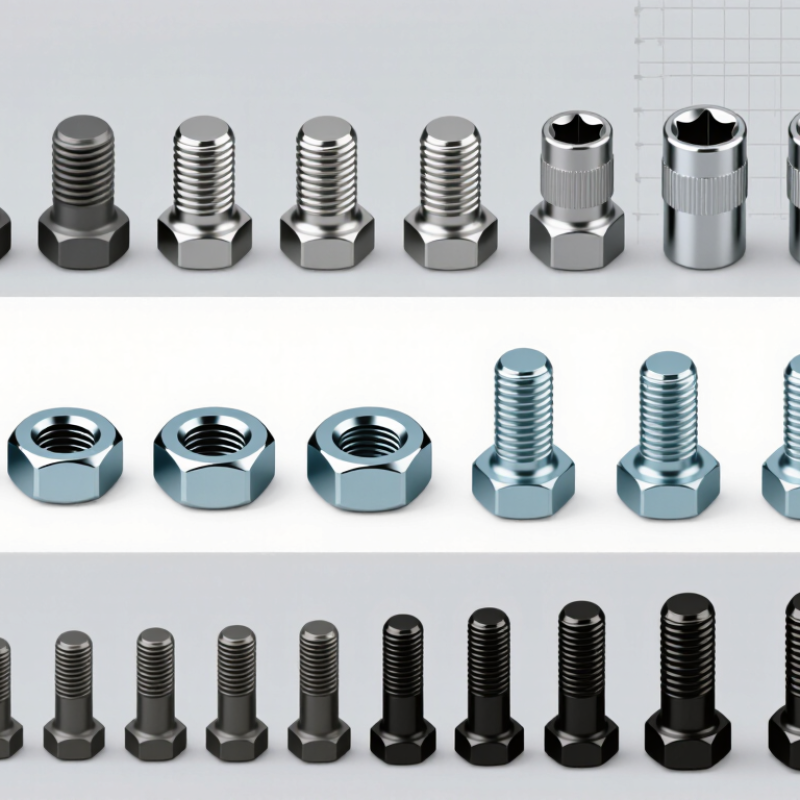
What Hex Socket Bolts Are and How They Work
What Hex Socket Bolts Are and How They Work
Hex socket bolts have a recessed six-sided drive in the head. An Allen key or hex bit fits inside this socket. Unlike external hex bolts, they need less clearance around the head. This makes them useful in machinery, furniture frames, automotive assemblies, and compact equipment.
The bolt works by converting turning force into clamping force. As the threaded shaft enters a matching nut or threaded hole, the bolt stretches slightly. This tension pulls the connected parts together. Correct torque matters because too little force may cause loosening, while too much can damage the threads or socket.
Small details affect performance. The socket must be clean and fully engaged. A worn key can round the recess, especially during removal. I have found that hand-starting the bolt prevents cross-threading better than using a power tool immediately. It takes longer, but it avoids expensive rework.
Buyers should check thread size, length, head style, material, strength class, and surface finish. Stainless steel can resist corrosion, but it may not match the strength of hardened alloy steel. Lubrication also changes the final clamping force at the same torque. This point is often overlooked. In exposed assemblies, buyers should also confirm washer use, installation torque, and environmental conditions before selecting a bolt.
Key Hex Socket Bolt Types for Global Buyers in 2026
Key Hex Socket Bolt Types for Global Buyers in 2026
Global buyers need more than a familiar fastener shape. The correct hex socket bolt depends on load, access, corrosion risk, and assembly speed. Socket head cap bolts suit high-strength joints where space is limited. Their cylindrical heads provide strong clamping force and reliable tool engagement. Button head bolts offer a rounded profile for exposed assemblies. They reduce sharp edges but usually provide less driving depth. Flat countersunk bolts sit nearly flush with a surface. They are useful for panels, rails, and compact equipment. Low-profile socket bolts help when head height is restricted. However, they may reduce available tightening torque.
In procurement reviews, I have found that thread accuracy matters as much as material grade. Confirm diameter, pitch, length, head dimensions, and socket size before ordering. Stainless steel supports humid environments, while alloy steel suits demanding structural applications. Surface treatments can improve corrosion resistance, but compatibility with nearby materials still requires checking. Request inspection records, material certificates, and dimensional reports. Packaging should protect threads from impact and moisture during long-distance shipping. A low-profile head may look efficient, but I have sometimes underestimated tool clearance. That mistake can delay installation.
Tips: Match the bolt type to the joint design, not only the catalog image. Check whether metric or imperial threads are required. Test a small sample before approving a large shipment. Ask suppliers about tolerance control and batch traceability. Keep a spare socket tool on site. It sounds minor, yet missing tools can stop an entire assembly line.
Materials, Strength Grades, Coatings, and Performance Features
2026 Top Hex Socket Bolt Types for Global Buyers
Hex socket bolts differ by material, strength grade, coating, and head design. Carbon steel suits general machinery and controlled indoor environments. Alloy steel supports higher tensile loads, especially in compact assemblies. Stainless steel resists moisture and chemical exposure, but its strength may be lower. Always verify the applicable standard, such as ISO 4762, and confirm thread dimensions before ordering.
Metric grades 8.8, 10.9, and 12.9 serve different load requirements. Grade 12.9 is strong, but it is not automatically the best choice. Higher hardness can increase brittleness and installation sensitivity. Zinc coatings help resist corrosion, while black oxide offers limited protection without additional oil. Zinc flake and hot-dip galvanizing can perform better outdoors. Electroplating high-strength bolts requires careful hydrogen embrittlement control. Testing should include dimensional checks, hardness verification, and tensile inspection. Small errors matter.
Tips: Match the bolt to the joint, not only the advertised strength. Check temperature, vibration, salt exposure, and tightening torque. A stainless bolt may gall during installation, so controlled speed and suitable assembly lubricant can help. For coated fasteners, measure the coating thickness and review torque-tension data. Do not assume identical torque values across materials. Supplier documentation should identify heat treatment, batch traceability, inspection results, and packing protection. In practice, packaging is often overlooked, yet damp cartons can damage otherwise compliant fasteners.
How to Select the Right Hex Socket Bolt for Each Application
2026 Top Hex Socket Bolt Types for Global Buyers
How to Select the Right Hex Socket Bolt for Each Application
Selecting a hex socket bolt starts with the joint, not the catalog title. For compact machinery, socket head cap bolts provide high clamping force in narrow spaces. Button head bolts suit exposed surfaces where a lower profile reduces snagging. Flat countersunk heads work when the fastener must sit flush with a panel. Shoulder bolts are useful when a controlled unthreaded section guides movement.
Check the load direction, material thickness, and available clearance. A coarse thread can perform well in general steel assemblies, while a fine thread may offer better adjustment and preload control. Thread engagement matters. As a practical rule, the engaged length should match the material and loading conditions, not a convenient guess. Use compatible bolt and nut materials to reduce galling and galvanic corrosion. Outdoor equipment may need corrosion-resistant alloys or a suitable protective finish.
Do not ignore the hex socket size. A small drive can round during installation, especially with contaminated or worn tools. Apply the specified torque with a calibrated wrench, and inspect the first assembled joint. I once focused too heavily on bolt strength and overlooked washer seating; the joint loosened under vibration. That mistake still influences my checks. Temperature, vibration, repeated assembly, and access for future maintenance can change the correct choice. Test samples when the joint carries critical loads. Specifications help, but real fit and installation conditions deserve the final review.
Global Standards, Sizing, Quality Checks, and Sourcing Factors
Global buyers comparing hex socket bolts should begin with the required standard, not the lowest quotation. ISO 4762 covers socket head cap screws, while ASME B18.3 serves many inch-based applications. Property classes under ISO 898-1, such as 8.8, 10.9, and 12.9, indicate mechanical performance. Size checks should include thread diameter, pitch, length, head height, and hex-drive depth. Small dimensional errors can cause assembly failure.
Material selection deserves equal attention. The World Steel Association reported approximately 1.88 billion tonnes of crude steel production in 2023, yet steel origin alone does not prove bolt quality. Buyers should request heat numbers, chemical analysis, tensile results, hardness readings, and coating details. ASTM F606/F606M provides recognized mechanical test methods for fasteners. Inspectors should also sample the actual shipment, not only review certificates. Certificates can be correct, but mismatched lots still happen.
The 2024 Grand View Research assessment estimated the global fasteners market at about USD 90.6 billion in 2023, with continued growth expected through 2030. That scale increases sourcing choices and quality risks. Compare total landed cost, minimum order quantity, packaging, lead time, and inspection access. Clarify whether dimensions follow metric or inch systems. Ask for thread gauges and a first-article sample. It takes minutes.
Salt-spray results may look impressive, but they do not replace torque testing or field experience. I would also question unusually low prices. They may reflect thinner coatings, mixed grades, or incomplete inspection. A reliable supplier should explain tolerances clearly and accept independent verification before volume production.





