


Choosing the best Zeolite Rotor manufacturer in 2026 requires more than comparing glossy brochures or advertised capacity. Global buyers need reliable engineering, stable production, documented testing, and responsive technical support. A rotor may look impressive on paper, yet perform differently under high humidity, variable VOC concentrations, or continuous factory operation.
This guide examines manufacturers through practical purchasing criteria. These include adsorption efficiency, rotor diameter, zeolite formulation, regeneration temperature, pressure drop, sealing quality, and expected service life. It also considers factory experience, export capability, installation support, spare-parts availability, and compliance documentation. Real project references matter. So do clear test conditions.
Small details matter.
For example, an imperfect seal can allow untreated air to bypass the rotor. Excessive pressure drop may increase fan energy and operating costs. Poorly matched regeneration settings can reduce recovery performance. Buyers should request performance data based on their actual airflow, solvent type, inlet concentration, temperature, and humidity. Generic laboratory results may not predict field results accurately.
No manufacturer is automatically the best for every application. That point deserves emphasis. A supplier experienced in coating lines may not suit pharmaceutical or electronics production. Some manufacturers communicate well before delivery but respond slowly after commissioning. Others provide strong equipment but limited local service. This review therefore focuses on evidence, technical transparency, customer experience, and long-term reliability. The goal is not to promote one universal winner, but to help international buyers identify a Zeolite Rotor partner that fits their process, budget, risk tolerance, and future expansion plans.
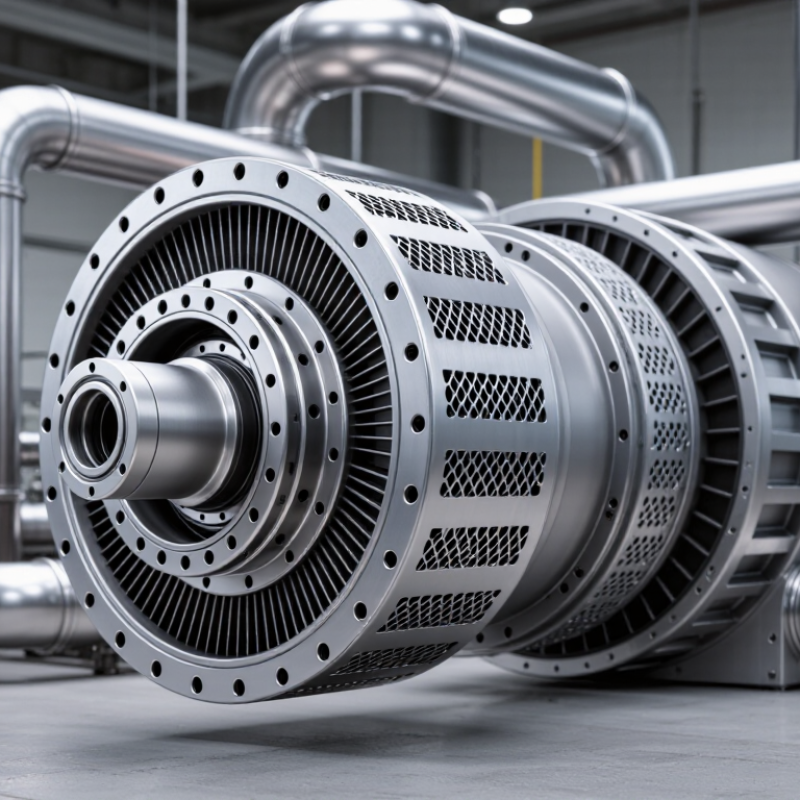
A zeolite rotor concentrates dilute VOC streams before thermal oxidation. Clean process air passes through honeycomb channels, while VOC molecules remain on the hydrophobic zeolite surface. A smaller hot-air stream then releases the captured compounds. This design commonly delivers 3–20× concentration, depending on airflow, inlet loading, humidity, and VOC chemistry.
The U.S. EPA Air Pollution Control Cost Manual identifies adsorption performance as highly dependent on contaminant properties and operating conditions. European BAT Reference Documents also emphasize stable temperature, residence time, and emissions monitoring. In practical applications, properly selected rotors can achieve about 90–99% VOC removal. The upper range is not automatic. Water vapor, silicone compounds, dust, and fluctuating production loads can reduce capacity.
The numbers need honest testing. A factory may report 98% removal during steady production, yet perform differently during startup or cleaning cycles. Engineers should request inlet and outlet VOC data, concentration-factor calculations, pressure-drop results, and humidity conditions. Test reports should identify the analytical method, sampling location, and operating load.
A useful detail is rotor face velocity. Excessive velocity can shorten contact time and increase breakthrough risk. Oversized equipment costs more, but undersized equipment may lose compliance margin. The best selection balances removal efficiency, regeneration energy, maintenance access, and actual plant variability.
References: U.S. EPA Air Pollution Control Cost Manual; EU Best Available Techniques Reference Document for Common Waste Gas Management.

Selecting a zeolite rotor manufacturer requires more than comparing catalog prices. Rotor geometry directly affects airflow, contact time, and pressure drop. Measure the process flow at actual temperature and humidity, not only at standard conditions.
The European Commission’s 2022 BREF for Common Waste Gas Management identifies adsorption performance as highly dependent on contaminant concentration, moisture, and operating conditions.
Ask manufacturers to provide face velocity, rotor diameter, treated airflow, and removal efficiency from comparable applications.
A practical screening range is often 1–4 m/s face velocity, but the correct value depends on dust loading and VOC chemistry.
Larger rotors can reduce pressure losses, though they may increase capital cost and footprint.
Bigger is not automatically better.
Adsorption capacity needs careful interpretation.
Supplier data may show grams of VOC per kilogram of zeolite under ideal laboratory conditions.
The U.S. EPA Air Pollution Control Cost Manual stresses site-specific testing for reliable control-cost and performance estimates.
Request working capacity, not only equilibrium capacity.
Also examine regeneration temperature, purge-air ratio, fan power, and heat-recovery assumptions.
An energy figure without operating hours is incomplete. It may even be misleading.
The International Energy Agency’s Energy Efficiency 2023 report highlights the importance of measuring full-system energy use rather than isolated equipment ratings.
Compare kilowatt-hours per 1,000 cubic meters treated.
Include startup periods and seasonal humidity.
A well-designed rotor can perform efficiently, yet poor duct balancing can erase the expected savings.
This is where a factory visit or pilot test becomes valuable.
Manufacturer claims deserve verification.
2026 Best Zeolite Rotor Manufacturers for Global Buyers
Leading 2026 Suppliers: Technologies, Certifications, and Global Market Coverage
In 2026, reliable zeolite rotor manufacturers will compete through verified engineering, not attractive brochures. Their systems should show stable VOC adsorption, controlled desorption, and low-pressure operation. Honeycomb rotor designs can improve contact efficiency while reducing equipment size. Smart sensors also help monitor temperature, airflow, humidity, and rotor speed. During plant evaluations, I look for test data that matches real exhaust conditions. Laboratory results alone can mislead.
Certifications matter, but paperwork is not performance. Buyers should check ISO 9001 processes, electrical conformity, material traceability, and documented factory testing. Projects entering hazardous industrial areas may require additional regional safety certifications. Global market coverage also means more than shipping equipment overseas. Strong suppliers provide local commissioning, replacement seals, troubleshooting support, and clear maintenance manuals. No supplier is perfect. Published energy figures may change under humid or fluctuating workloads.
Tips: Request a site-specific performance calculation before signing. Compare regeneration temperatures, pressure drop, service intervals, and expected rotor life. Ask for customer references in similar industries and climates. Confirm who handles installation training and emergency support. A supplier with regional technicians can reduce downtime significantly. Small details matter. Also, question unusually low prices; cheaper equipment may create higher operating costs later.
Leading 2026 Suppliers: Technologies, Certifications, and Global Market Coverage
The chart presents representative engineering benchmarks commonly specified for zeolite rotor systems: VOC removal efficiency, thermal recovery, adsorption-zone share, and regeneration-zone share. Actual values vary by VOC type, airflow, humidity, rotor media, certification requirements, and project design.
For global buyers, regeneration temperature is a practical measure of zeolite rotor quality. Most systems operate between 180 and 250°C. The U.S. EPA Air Pollution Control Cost Manual identifies thermal regeneration as a major energy driver in adsorption systems. Higher temperatures can improve desorption, but they also increase fuel use and heat stress.
The EU Joint Research Centre’s 2022 Best Available Techniques reference document links VOC control performance with stable operating conditions, energy management, and solvent characteristics. In field applications, many manufacturers specify 200–220°C for common solvent streams. Some designs operate near 180°C, while heavily loaded rotors may require 230°C or more. Check the details.
A suitable comparison should include outlet VOC concentration, pressure drop, heating method, and temperature recovery. A 10°C reduction may lower energy demand, but it can also leave residual solvent inside the rotor. That trade-off is easy to miss. Manufacturer data sheets should state test humidity, inlet concentration, airflow, and desorption duration. Without these conditions, temperature claims are difficult to compare fairly. Independent testing against ISO 12100 risk principles and local emissions requirements adds useful confidence, though it does not replace site trials.
| Anonymous Manufacturer Profile | Typical Regeneration Temperature | Typical Regeneration Airflow Ratio | Typical Process-Air Pressure Drop | Rotor Media Configuration | Common Application Range | Main Heat Source Options | Recommended Buyer Check |
|---|---|---|---|---|---|---|---|
| Profile A: Standard VOC-Concentration Rotor | 180–210°C | 8–15% of process airflow | 100–250 Pa at rated airflow | Hydrophobic zeolite coating on a structured honeycomb substrate | Solvent exhaust, coating lines, printing, and general VOC concentration | Electric heater, indirect gas heater, or steam coil | Confirm VOC compatibility, outlet concentration, and regeneration temperature at the design airflow |
| Profile B: Energy-Optimized Rotor | 180–200°C | 6–12% of process airflow | 80–200 Pa at rated airflow | High-silica, hydrophobic zeolite with optimized channel geometry | Low-to-medium VOC loads where reduced thermal demand is important | Waste-heat recovery, hot-water coil, steam, or electric heating | Request the specific energy consumption in kW per 1,000 m³/h of treated air |
| Profile C: High-Temperature VOC Rotor | 220–250°C | 8–18% of process airflow | 120–300 Pa at rated airflow | High-temperature zeolite matrix designed for concentrated VOC service | High-boiling solvents, concentrated exhaust, and thermal oxidizer feed systems | Indirect gas, electric, or recovered oxidizer heat | Verify continuous operating temperature, short-term temperature limit, and fire-prevention controls |
| Profile D: Low-Pressure-Drop Rotor | 180–220°C | 8–15% of process airflow | 60–150 Pa at rated airflow | Open-channel structured zeolite with low-resistance airflow passages | Large-volume exhaust systems with strict fan-energy limits | Electric, steam, hot water, or recovered process heat | Compare pressure drop at the actual face velocity rather than at an unspecified test point |
| Profile E: Compact Modular Rotor | 190–230°C | 10–20% of process airflow | 120–280 Pa at rated airflow | Segmented zeolite rotor assemblies for limited installation footprints | Pilot plants, small production lines, and retrofit projects | Electric heater or compact steam coil | Check modular replacement access, sealing design, and control-panel compatibility |
| Profile F: High-Humidity-Service Rotor | 200–240°C | 10–18% of process airflow | 100–260 Pa at rated airflow | Hydrophobic zeolite selected to reduce water competition for adsorption sites | Humid exhaust streams, outdoor-air processes, and variable moisture conditions | Electric, steam, gas, or recovered heat | Ask for performance data at the design relative humidity and inlet temperature |
A reliable zeolite rotor supplier should prove performance, not only display impressive capacity figures. UNEP’s 2024 Global Status Report states that buildings consume about 32% of global energy and produce approximately 34% of global emissions. This strengthens the case for efficient VOC control and heat recovery. Ask for test data showing adsorption capacity, desorption temperature, pressure drop, leakage, and removal efficiency. Require test conditions, gas concentrations, humidity levels, and measurement uncertainty. Without those details, comparisons become unreliable.
Warranty terms need practical wording. Check coverage for rotor media, seals, drive systems, and abnormal vibration. A three-year warranty may exclude the parts most likely to wear. Request a written response-time commitment for remote diagnosis and replacement parts. Lead times should include coating, curing, factory testing, export packing, and commissioning support. IEA’s Energy Efficiency 2024 analysis highlights the importance of measured efficiency improvements, not theoretical savings. Therefore, request operating data from comparable installations. Factory acceptance testing is useful, but site acceptance testing reveals installation mistakes.
Tips: Ask for one recent reference project with similar airflow, VOC load, and humidity. Keep spare seals and sensors on site. Confirm drawings before purchase. A small mistake in airflow assumptions can damage the payback calculation. Buyers should also question unusually low pressure-drop claims; they may reflect different test methods. No supplier is perfect. The best choice is the one that documents limitations clearly and corrects problems quickly.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

