


Choosing the right Compression Moulding Parts in 2026 requires more than comparing shapes, prices, or catalog photographs. Each part must suit its material, load, temperature, and production environment. A thick electrical insulator behaves differently from a thin automotive seal. Small design choices matter.
Dr. James L. Throne, a respected plastics-processing specialist, has emphasized this practical principle: “The mold is part of the process, not merely a container for the material.” That idea remains highly relevant. Compression pressure, cure time, mold temperature, fiber direction, and release behavior can influence dimensional accuracy. They also affect surface finish and service life. A polished cavity may produce a clean face, but poor venting can still leave trapped air near sharp corners.
This guide examines the 2026 best types of Compression Moulding Parts for industrial, automotive, electrical, medical, and composite applications. It considers thermoset components, rubber parts, fiber-reinforced structures, and specialty molded products. The discussion focuses on practical selection, not marketing claims. Material compatibility comes first. Repeatability matters too.
There is no universal “best” part.
A component that performs well in a high-volume factory may fail in a low-temperature installation. Engineers should review tolerances, testing records, maintenance needs, and supplier consistency before approving a design. Some recommendations may require adjustment after real production trials. That is normal. Even experienced teams can underestimate shrinkage, flash, or uneven pressure distribution. Careful evaluation turns those imperfections into useful design information.
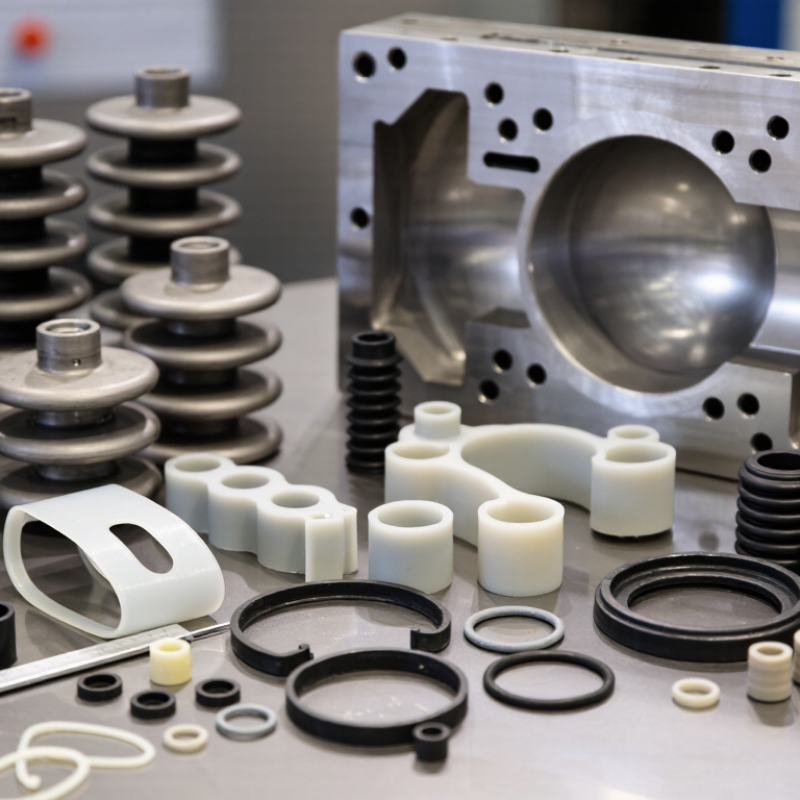
Compression moulding parts are components formed by pressing a measured material charge inside a heated mould. The charge may be rubber, thermoset plastic, or fibre-reinforced composite. Heat softens or cures it. Pressure then creates the required shape.
Common examples include gaskets, seals, electrical insulators, vehicle panels, handles, and protective housings. A finished part often shows smooth edges, stable dimensions, and visible moulding lines. These details matter. A poorly placed charge can create thin areas, voids, or uneven fibre distribution. The process is not flawless.
PlasticsEurope’s Plastics—The Fast Facts 2023 reports 400.3 million tonnes of plastics were produced worldwide in 2022. That scale increases demand for repeatable moulded components, especially in transport, electrical, and industrial equipment. The U.S. Department of Energy also identifies lightweight composite materials as a route to reducing vehicle mass and energy use. Compression moulding supports this aim by shaping strong parts with relatively low material waste.
Material selection still requires testing. Rubber parts may need tensile and compression-set testing under ASTM methods. Plastic components require checks for impact strength, heat resistance, and dimensional stability. ISO 20457 also provides guidance for tolerances in moulded plastic parts. Designers sometimes focus too heavily on appearance. Service temperature, moisture, pressure, and ageing can matter more. A small sealing part may fail quietly, then damage an entire assembly.

Compression moulding parts are best classified by material, geometry, and end use. Material classification usually separates thermosets, elastomers, and thermoplastic composites. Thermoset parts include phenolic, epoxy, and silicone components. Elastomeric parts include seals, gaskets, and vibration pads. Thermoplastic composite parts use heated sheets or charge materials. They can be reshaped during processing.
Geometry provides another practical classification. Flat panels need controlled pressure and even heating. Deep housings require careful material flow. Ribbed covers need accurate charge placement. Thin sealing rings demand stable mould temperatures. The classification affects flash control, cycle time, and dimensional inspection. It is not only a design label.
Market data supports this wider view. The Plastics—The Fast Facts 2024 report recorded global plastics production at about 414 million tonnes in 2023. However, that figure covers many processes, not compression moulding alone. Industry forecasts also estimate steady growth for compression moulding through 2029, driven by lightweight transport and electrical applications. Forecasts differ.
That matters. Report boundaries are inconsistent. Some include composite compression parts, while others count only moulding equipment or materials. Engineers should therefore classify each part using three fields: material family, shape complexity, and functional purpose. A part may fit several categories. That is normal, but it can weaken purchasing comparisons without shared definitions.
2026 Best Types of Compression Moulding Parts
Which Materials Are Used in Compression Moulding Parts?
Compression moulding parts commonly use thermoset compounds, rubber, and engineering composites. Sheet moulding compound and bulk moulding compound combine resin, fillers, and reinforcing fibres. They suit electrical housings, vehicle panels, and structural brackets. Phenolic compounds resist heat and flame. Epoxy compounds deliver strong adhesion and dimensional stability. Silicone rubber remains useful for seals exposed to heat and moisture. Material choice depends on pressure, temperature, impact, and surface requirements.
Grand View Research estimated the global compression moulding market at about USD 6.5 billion in 2023. Its report forecasts approximately 5.2% annual growth from 2024 to 2030. This growth reflects demand for lighter parts and stable production cycles. MarketsandMarkets also identifies thermoset composites as important for transport and electrical applications. Yet published forecasts differ. They use different product boundaries and regional data. That limitation deserves attention.
Tips: Start with the service environment, not the cheapest compound. Check operating temperature, moisture, chemical contact, and required stiffness. Ask for fibre content, shrinkage data, and batch traceability. A small pilot run can reveal warpage or incomplete filling. It is not glamorous, but it prevents expensive tooling changes. Recycled fillers may reduce material impact, but they can change flow and strength. Test them before approving production.
Which materials are used in compression moulding parts?
Compression moulding commonly uses thermoset compounds and elastomers for electrical housings, automotive components, seals, gaskets, cookware handles, structural panels, and industrial parts. The chart shows representative moulding temperatures for widely used material groups. Actual values vary according to grade, part thickness, pressure, and curing system.
Compression moulding begins with a measured charge of thermoset compound, rubber, or composite material. Operators place it inside a heated mould cavity. The upper mould then closes and applies controlled pressure. Heat softens the charge, while pressure drives it into ribs, bosses, and thin edges. The material cures inside the cavity before ejection.
Typical parts include electrical housings, automotive covers, sealing rings, handles, and structural panels. Sheet moulding compound suits larger reinforced panels. Bulk moulding compound works well for compact, detailed components. Rubber compounds need accurate temperature control because under-curing leaves weak areas. Over-curing can create brittle edges.
Small details matter.
A 2024 MarketsandMarkets assessment estimated the compression moulding compounds market at about 5.9 billion US dollars in 2023. It also projected growth toward roughly 8.2 billion dollars by 2028. These figures reflect wider demand for lightweight and electrically insulating parts. However, market forecasts are not production guarantees. Actual results depend on tool design, material moisture, charge placement, and cycle discipline.
During manufacturing, technicians inspect the charge weight, mould temperature, closing speed, cure time, and flash thickness. A practical temperature range may fall near 140–180°C, but each compound requires its own validated schedule. After demoulding, trimming removes excess flash. Dimensional checks, visual inspection, and hardness or strength tests reveal defects. A single surface reading can mislead. Internal curing may still be incomplete, which is why process records and sampled testing remain essential.
Compression moulding parts serve demanding applications where heat, pressure, and repeatability matter. Manufacturers place measured material charges into heated moulds, then apply controlled pressure. This method produces covers, brackets, housings, seals, and structural panels with stable dimensions. Thermoset compounds, rubber, and fibre-reinforced materials are common choices.
Automotive systems use these parts under the bonnet, inside electrical modules, and around battery compartments. They can resist vibration, chemicals, and elevated temperatures when the material is correctly specified. Electrical equipment also uses compression-moulded insulators, switch components, and protective enclosures. Their low electrical conductivity helps separate live components from surrounding structures. The fit matters.
In construction and industrial equipment, moulded parts appear as pipe seals, pump components, handles, and corrosion-resistant panels. Fibre-reinforced mouldings can provide stiffness without excessive weight, supporting transport and energy equipment applications. Medical and laboratory products may use compression moulding for rigid trays or chemically resistant components, but material traceability and validation remain essential. The process is not flawless. Uneven charge placement can create voids, warping, or weak edges. I would not judge quality from appearance alone. Engineers should verify cure time, pressure records, dimensional tolerances, and finished-part performance. Small changes in moisture, temperature, or mould wear can affect long production runs. That practical risk is often underestimated.
| Compression Moulding Part Type | Common Material Families | Key Functional Properties | Main Applications | Typical End-Use Industries | Why Compression Moulding Is Suitable |
|---|---|---|---|---|---|
| Electrical Insulators and Covers | Thermoset compounds such as epoxy, phenolic, melamine and unsaturated polyester moulding compounds | Electrical insulation, dimensional stability, flame resistance and resistance to heat and chemicals | Switchgear barriers, terminal covers, fuse bodies, connector housings and insulating supports | Power distribution, electrical equipment and industrial control systems | Thermoset materials cure into rigid, heat-resistant parts with reliable insulating performance |
| Automotive Exterior Panels | Glass-fibre-reinforced sheet moulding compound (SMC), carbon-fibre compounds and other thermoset composites | Low density, corrosion resistance, good surface finish and useful stiffness-to-weight ratio | Hood panels, roof modules, trunk lids, body panels and underbody shields | Passenger vehicles, commercial vehicles and specialty vehicles | Large composite panels can be formed with integrated ribs, mounting points and multiple contours in one operation |
| Automotive Structural and Under-Hood Parts | Glass-fibre-reinforced thermoset compounds, long-fibre thermoplastics and high-temperature engineering compounds | Structural stiffness, vibration damping, heat resistance and resistance to automotive fluids | Battery trays, air-intake components, engine covers, brackets, fan shrouds and cross-car structures | Automotive powertrain, chassis and electric-vehicle systems | Fibre reinforcement improves mechanical performance while compression moulding supports repeatable, complex geometries |
| Rubber Seals and Gaskets | Silicone rubber, EPDM, nitrile rubber, fluorocarbon rubber and natural rubber compounds | Elastic recovery, sealing capability, resistance to temperature, weathering, oils or chemicals depending on the compound | O-rings, flange gaskets, valve seals, pipe seals, cable seals and custom sealing profiles | Fluid handling, automotive, medical equipment, HVAC and industrial machinery | The process applies controlled heat and pressure to cure elastomers into durable, flexible sealing parts |
| Rubber Vibration and Impact Components | Natural rubber, synthetic rubber, silicone rubber and polyurethane elastomer compounds | Vibration isolation, shock absorption, resilience, noise reduction and fatigue resistance | Engine mounts, bushings, anti-vibration pads, bump stops and suspension components | Automotive, rail transport, industrial machinery and construction equipment | Compression moulding is effective for producing thick elastomeric parts with controlled hardness and damping characteristics |
| Composite Sporting Goods | Carbon-fibre, glass-fibre or aramid-fibre reinforced epoxy and other thermoset resin systems | High specific strength, stiffness, fatigue resistance and design flexibility | Bicycle components, protective equipment, racket frames, board components and sporting braces | Cycling, outdoor recreation, fitness and professional sports equipment | Fibre orientation and laminate construction can be tailored to achieve lightweight, directional performance |
| Aerospace Interior and Composite Parts | Carbon-fibre or glass-fibre reinforced epoxy, phenolic and high-temperature thermoset composites | Low weight, stiffness, fire-smoke performance potential and resistance to temperature and chemicals | Interior panels, seat components, trays, brackets, access panels and aerodynamic fairing parts | Aircraft interiors, unmanned aircraft and aerospace equipment | Heated compression tooling can consolidate fibre-reinforced laminates and produce repeatable thin or contoured parts |
| Industrial Wear Plates and Liners | Phenolic composites, fibre-reinforced thermosets, polyurethane elastomers and engineering thermoplastics | Abrasion resistance, low friction, impact resistance and dimensional stability | Conveyor wear strips, guide plates, bearing pads, chute liners and machine slide components | Material handling, mining, manufacturing and process equipment | Compression moulding can produce dense, durable parts with consistent thickness and embedded reinforcement |
| Household and Appliance Components | Melamine-formaldehyde, phenolic, urea-formaldehyde and glass-fibre-reinforced moulding compounds | Heat resistance, electrical insulation, hardness, scratch resistance and dimensional stability | Cookware handles, appliance knobs, switch components, heat-resistant housings and structural supports | Domestic appliances, kitchen equipment and consumer products | Compression moulding supports economical production of rigid thermoset components with good surface quality |
| Medical and Laboratory Components | Medical-grade silicone, thermoset composites and selected engineering polymer compounds | Flexibility, chemical resistance, temperature tolerance and suitability for sterilisation requirements when properly formulated | Seals, diaphragms, protective covers, instrument components and fluid-handling parts | Medical devices, laboratory equipment and healthcare systems | The process is suitable for repeatable shapes and controlled material properties in low-to-medium volume specialist parts |
Note: Material selection, mould temperature, pressure, cure time and part performance depend on the specific formulation, design requirements and applicable industry standards.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

