


The 2026 Best Industrial Grippers for Global Buyers guide examines a small component with a major production role. A gripper may touch every part, from a warm cast-metal housing to a delicate medical tray. Its performance affects cycle time, product damage, operator safety, and maintenance costs.
The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023. It also recorded more than 4.28 million industrial robots operating globally. These figures show why reliable end-of-arm tooling deserves closer evaluation. However, robot growth does not guarantee gripper suitability. Jaw force, payload, stroke, grip geometry, air consumption, and sensor feedback must match the real application. A fast gripper can still fail on oily surfaces or inconsistent part dimensions.
Application evidence matters more than attractive specifications. ISO 10218 provides a useful safety framework for industrial robot systems, while ISO/TS 15066 offers guidance for collaborative robot applications. Buyers should also review testing records, spare-part availability, technical support, and regional compliance documentation. Supplier claims require verification. No shortlist is flawless.
This guide compares pneumatic, electric, magnetic, vacuum, parallel, and angular designs for global purchasing teams. It considers precision assembly, packaging, machining, logistics, and harsh factory environments. Energy use deserves attention too. The U.S. Department of Energy identifies compressed-air systems as significant industrial energy users, especially when leaks remain unnoticed. A well-selected Industrial Gripper can reduce wasted motion and rejected parts. Yet selection still depends on the product, robot, tooling interface, and production culture. That judgment cannot be automated completely.
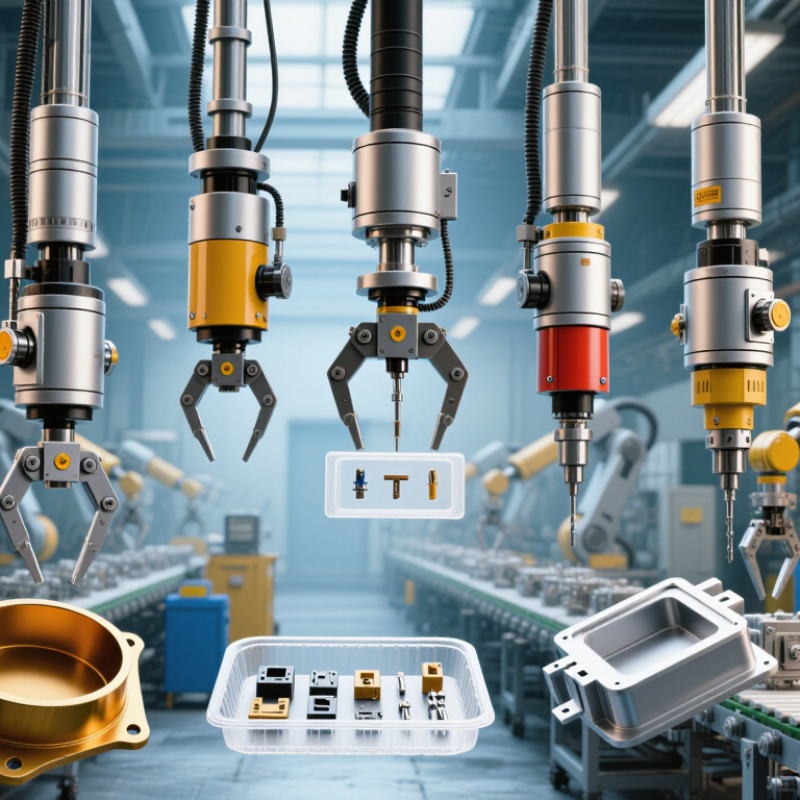
Industrial grippers are not interchangeable tools.
The best choice depends on part geometry, surface condition, payload, cycle speed, and failure risk. A 2-jaw gripper suits rectangular parts and general pick-and-place work. Its simple layout makes setup easier. A 3-jaw gripper centers round components more evenly, especially during machining or inspection. However, extra jaws can reduce access around the workpiece.
Vacuum grippers handle smooth, sealed surfaces such as glass, panels, and cartons. They are lightweight and fast, but dust, oil, or textured materials can weaken the seal. Add vacuum monitoring and a suitable backup system when a dropped load could damage equipment.
Magnetic grippers work well with ferrous steel sheets and rough surfaces. They do not suit aluminum, plastic, or non-magnetic alloys. Check residual magnetism too, since some parts may need clean release.
Soft grippers protect delicate fruit, packaging, and irregular products through flexible contact. They are useful when hard jaws might leave marks. Yet soft fingers can wear faster and may offer less positional accuracy.
No design wins every time. In real production reviews, buyers often focus on gripping force and overlook jaw stroke, sensor compatibility, and maintenance access. That is a costly mistake.
Confirm the actual payload, center of gravity, air pressure, temperature, and surface finish before ordering. Request test results using your own parts when possible. Safety margins should reflect vibration and acceleration, not just static weight. A compact gripper may appear efficient, but limited clearance can create daily frustration. Reliable selection is practical, documented, and willing to question the first attractive specification.

2026 Best Industrial Grippers for Global Buyers
Industrial grippers should be selected by measured performance, not attractive catalog numbers. A 10 N gripper may suit delicate handling, while demanding fixtures can require up to 10,000 N. Confirm whether the rated force applies per finger or to the complete gripping system. That distinction matters.
Stroke requirements also vary sharply. A compact mechanism may need only 1 mm for stable positioning, while large workpieces may require 500 mm. Leave practical clearance for part variation, jaw wear, and installation errors. A 0.05 mm repeatability rating sounds impressive, but it may depend on speed, load, temperature, and mounting rigidity. Small errors grow.
Experienced buyers should request test conditions, force curves, duty-cycle data, and maintenance intervals. Check performance with the actual material, surface finish, and gripping direction. Pneumatic, electric, and hydraulic designs can behave differently under rapid cycling. Real conditions differ. A gripper that performs well in a clean test cell may lose accuracy beside vibration, dust, or changing temperatures.
I would also challenge overly precise specifications. Repeatability does not guarantee absolute positioning accuracy, and maximum force does not define safe working force. Use a safety margin, then validate the complete assembly through repeated trials. Record opening time, holding force, slip, noise, and temperature rise. The first test may expose an uncomfortable truth: the strongest gripper is not always the most reliable choice.
Choosing an industrial gripper starts with the workpiece, not the catalog. Pneumatic grippers suit fast pick-and-place lines and simple open-close cycles. They are compact, affordable, and easy to maintain. However, compressed air can waste energy, especially across long production shifts. Electric grippers provide controlled stroke, force, and speed. They work well with fragile parts, variable sizes, and data-based quality checks. Their wiring and software require more planning. Hydraulic grippers deliver high force for heavy components. They need strong infrastructure, clean fluid management, and careful leak control. Servo grippers add precise feedback and adjustable motion. They are valuable when alignment, insertion depth, or part variation matters. No drive wins every line.
Tips: Measure real gripping force, not only rated force. Test parts when oily, warm, or slightly misaligned. Check cycle time at the required load. Leave room for jaw wear and future tooling.
In field evaluations, operators often prefer simple pneumatic units for repetitive handling. Engineers may choose electric or servo models when traceability matters. A hydraulic solution can be practical for harsh, force-heavy applications, but maintenance access must be realistic. Supplier documentation should state force curves, duty limits, protection ratings, and replacement procedures. Ask for sample testing with your actual parts. A clean factory trial can hide problems found on the production floor. Noise, cable routing, air quality, and emergency stopping behavior also deserve attention. Small oversights become expensive after installation.
Industrial grippers in 2026 must prove more than lifting strength. Global buyers should verify safety evidence, environmental protection, and integration records before comparing cycle times.
ISO 10218 defines safety requirements for industrial robot systems and applications. ISO/TS 15066 adds guidance for collaborative operation, including contact limits and risk assessment.
A gripper is not automatically collaborative because it uses low force. The complete robot cell needs validation.
IFR World Robotics 2024 reported 541,302 industrial robots installed worldwide in 2023. More installed robots mean more pressure for consistent safety documentation.
CE marking confirms conformity with applicable European requirements, but it is not a universal safety certificate. Importers should request the Declaration of Conformity, technical file references, and test conditions.
IP65
IP65 protection means dust-tight construction and resistance to water jets. It does not guarantee protection against immersion, chemicals, or hot washdown.
In a factory, look for sealed connectors, protected sensors, and visible gasket inspection points. Small gaps often become expensive failures.
Tips:
Match the gripper’s IP rating to the real cleaning routine. Ask whether ISO 10218 and ISO/TS 15066 assessments cover the entire cell. Check payload at the longest jaw extension, not only at the catalog’s ideal position.
Keep records of validation tests. Documentation is sometimes treated as paperwork, yet it can reveal weak assumptions before installation.
No standard replaces a site-specific risk assessment.
Choosing the best industrial gripper in 2026 requires more than checking maximum payload. In factory trials, a gripper lifting 8 kilograms may fail when acceleration, offset load, and emergency stops are added. Apply a safety margin of 20–30%, then verify force at the actual jaw position. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023. That scale makes dependable end-of-arm tooling a practical purchasing issue, not a minor accessory decision.
Cycle life needs evidence. Ask for tested cycles, jaw wear limits, seal replacement intervals, and performance after contamination. A specification sheet alone is weak evidence. During acceptance testing, record grip force, repeatability, and dropped-part events over several shifts. Energy use also deserves attention. The U.S. Department of Energy notes that compressed-air systems can represent 10–30% of industrial electricity use, while leakage can waste a significant share of output. Electric grippers may reduce air demand, but their standby consumption and maintenance costs still require measurement.
Compatibility affects hidden costs. Check robot payload, flange standards, control protocols, cable routing, guarding, and available spare parts before ordering. Total cost of ownership should include tooling, installation, air preparation, electricity, downtime, and technician hours. The cheapest unit may become expensive after one unplanned stoppage. I would still avoid promising a universal winner. Production dust, fragile surfaces, and irregular parts can overturn laboratory results. Test with real components, not clean samples.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

