


2026 Best Hot Sealing Machine Types for Packaging

Choosing a Hot Sealing Machine in 2026 is no longer a simple matter of comparing price and speed. Packaging lines now handle thinner films, recyclable structures, dusty products, and frequent format changes. A machine that performs well on clean polyethylene bags may struggle with laminated pouches or uneven fill levels.

Packaging educator Walter Soroka defined packaging as “the science, art, and technology of enclosing and protecting products for distribution, storage, sale, and use.” His statement remains highly relevant to heat sealing. A reliable seal protects more than appearance. It supports shelf life, transport safety, product hygiene, and customer confidence. In practical terms, operators must examine sealing temperature, dwell time, jaw pressure, seal width, and cooling behavior. Small adjustments matter. A wrinkled film edge can create a hidden leak.

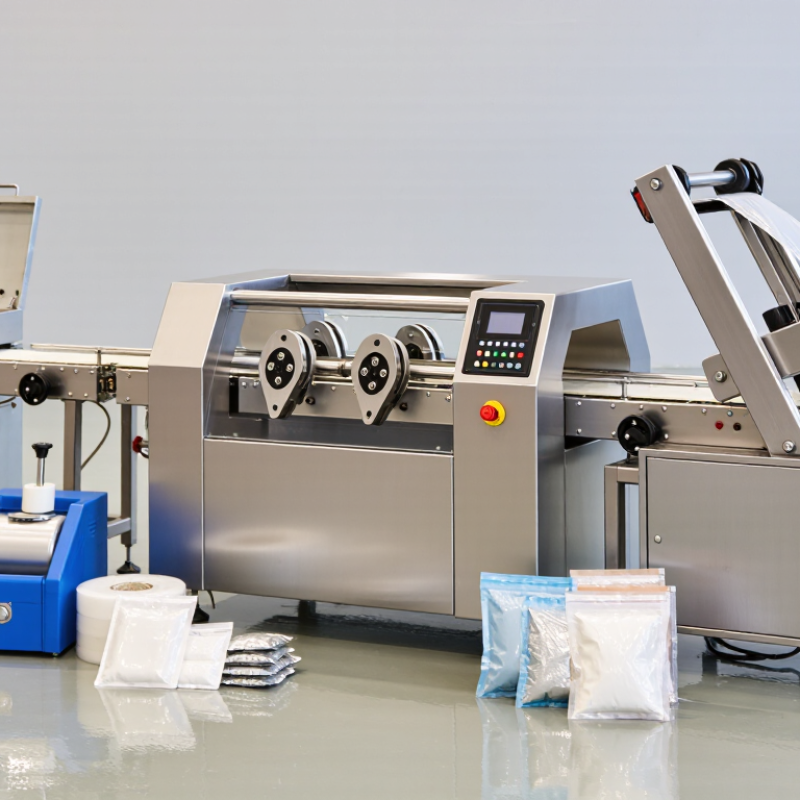
The 2026 market includes impulse sealers, constant-heat sealers, continuous band machines, vacuum sealers, and automated rotary systems. Each type suits different materials, production volumes, and quality requirements. Some lines need a compact bench unit beside a weighing station. Others require stainless steel equipment, conveyor integration, and recorded sealing data. The best choice depends on evidence, not impressive specifications. This guide compares the leading Hot Sealing Machine types, their strengths, limitations, and operating details. It also considers energy use, maintenance access, operator training, and testing methods. No machine is perfect. That is worth remembering. A technically advanced sealer can still fail when the film, settings, or cleaning routine is poorly controlled.
2026 Best Hot Sealing Machine Types for Packaging

Hot Sealing Fundamentals: Temperature, Pressure, and Dwell Time per ISO 11607-2

2026 Best Hot Sealing Machine Types for Packaging

Hot sealing machines may use constant heat, impulse heat, or heated bands. Each type controls temperature, pressure, and dwell time differently. ISO 11607-2 focuses on validating the sealing process, not choosing one universal machine setting. The correct window depends on the pouch film, paper structure, seal width, and product contamination risk.

Temperature must soften the sealant layer without scorching the package. Pressure should create even contact across the seal, while dwell time allows heat transfer and bonding. A practical trial may use a calibrated temperature sensor, a verified pressure gauge, and controlled dwell settings. For example, operators can inspect a 10-millimeter seal after changing one variable at a time. Small wrinkles, channel leaks, or weak peel resistance often reveal unstable conditions.

Visual inspection alone is not enough. Seal-strength testing, leak testing, equipment calibration, and documented process qualification provide stronger evidence. ISO 11607-2 supports a controlled validation approach, including installation, operational, and performance qualification. In real production, a clean seal can still fail after aging or handling. That is easy to overlook. Materials also vary between lots, so one successful trial should not become permanent proof. Review the process window regularly, train operators on actual defects, and record every meaningful adjustment. A reliable seal is a measured result, not merely a neat-looking line.


Impulse vs. Constant-Heat Sealers: Comparing 0.5–3 Second Dwell Times

Impulse and constant-heat sealers handle packaging films differently, especially across 0.5–3 second dwell times. An impulse sealer heats the sealing wire only during closure. This helps reduce energy use and limits heat exposure around the package. It often suits polyethylene bags, coated films, and lighter materials.

Constant-heat sealers keep the jaws warm before contact. They can produce steadier seals on thicker laminates, coated papers, and heat-sensitive structures requiring controlled contact. At 0.5 seconds, the seal may look acceptable but lack full bond strength. Around 1–2 seconds, many films develop a more stable seal when pressure remains even. Three seconds may improve bonding, yet excessive dwell can wrinkle film or distort the package edge.

Small details matter. In practical testing, I check seal width, peel resistance, channel leaks, and visible film damage. A clean seal can still fail under tension. I have also seen operators increase dwell time when the real problem was weak jaw pressure or uneven film placement. That shortcut wastes time. Material thickness, temperature, pressure, and cooling should be tested together. Record each trial with a timer and sample batch. If the film changes, repeat the validation. Packaging lines rarely behave perfectly on the first attempt.

2026 Best Hot Sealing Machine Types for Packaging - Impulse vs. Constant-Heat Sealers: Comparing 0.5–3 Second Dwell Times
Sealer Type Typical Dwell Time Typical Temperature Range Common Seal Width Suitable Packaging Materials Production Characteristics Main Advantages Key Limitations Typical Applications
Impulse Sealer 0.5–1.5 seconds Approximately 120–200 °C, depending on film structure and thickness 2–5 mm PE, PP, laminated films, coated aluminum foil, and other heat-sealable pouches or bags Heat is applied only while the sealing jaws are closed; suitable for intermittent operation and light-to-medium production volumes Low energy use between cycles, compact design, quick start-up, and relatively low equipment cost Usually requires a cooling or holding phase for stronger seals; less suitable for thick, contaminated, or continuously fed materials Retail bags, sample packs, laboratory bags, small e-commerce orders, and general flexible packaging
Heavy-Duty Impulse Sealer 1–2 seconds Approximately 140–220 °C, depending on material and seal configuration 5–10 mm Thicker PE bags, multi-layer laminates, gusseted bags, and medium-gauge flexible films Intermittent sealing with stronger clamping pressure and wider sealing elements than standard impulse units Handles thicker films better, produces wider seals, and provides good flexibility for different bag sizes Cycle time can increase with thick films; heating elements and sealing tapes require periodic replacement Industrial parts, frozen products, agricultural supplies, hardware, and warehouse packaging
Constant-Heat Sealer 1–3 seconds Approximately 130–230 °C, controlled by thermostatic or electronic temperature systems 3–12 mm Coated films, laminated structures, cellophane-type films, foil laminates, and materials requiring heat on both seal surfaces Sealing jaws remain continuously heated; suitable for repeatable intermittent production and materials needing sustained heat transfer Consistent heat penetration, stronger seals on compatible laminates, and better performance with thicker or less heat-responsive films Higher idle energy consumption than impulse models; overheated films may wrinkle, distort, or burn if settings are incorrect Food pouches, medical and laboratory packaging, laminated bags, and medium-volume production lines
Band Sealer with Constant Heat 0.5–2 seconds of effective heat exposure Approximately 120–200 °C, depending on film, speed, and seal design 6–15 mm PE, PP, laminated films, foil-laminated packaging, and many thermoplastic bags Continuous transport of bags through heated belts; throughput is controlled primarily by conveyor speed and sealing temperature Supports continuous operation, consistent seal placement, and higher throughput than manually operated jaw sealers Requires correct bag presentation and tracking; unsuitable for irregularly shaped products without additional handling equipment Powders, grains, snacks, chemicals, pet food, and high-frequency bag sealing
Vertical Continuous Band Sealer 1–3 seconds of effective heat exposure Approximately 120–220 °C, depending on package material and product conditions 6–15 mm Thermoplastic bags containing powders, granules, liquids, and other products that are filled vertically Continuous sealing with the package supported below or beside the sealing path; commonly used when product weight affects bag handling Suitable for heavier bags, improves seal consistency on vertically filled packages, and supports continuous production Requires more floor space and setup than handheld sealers; product dust or liquid near the seal can reduce seal quality Powdered foods, agricultural products, chemicals, pet food, and vertically filled industrial bags
Hot-Bar or Tray-Sealing Machine 1–3 seconds Approximately 140–230 °C, depending on tray, lidding film, and coating Typically 3–8 mm around the package perimeter Thermoformed trays, coated lidding films, PP containers, CPET trays, and compatible barrier structures Heated tooling applies pressure around a defined package perimeter; often integrated with cutting, vacuum, or gas-flushing functions Accurate seal geometry, professional package appearance, and compatibility with modified-atmosphere packaging systems Higher tooling and setup costs; seal performance depends strongly on flange cleanliness, pressure, temperature, and dwell time Ready meals, fresh foods, medical trays, industrial components, and tamper-evident containers
Technical note: Dwell time, temperature, pressure, cooling time, film thickness, coating type, and contamination at the seal area all affect final seal strength. The ranges above are typical operating guidelines rather than universal settings; production trials should be used to establish validated machine parameters for each packaging structure.

Continuous Band Sealers: 20–40 Packs per Minute and 3–12 mm Seal Widths

Continuous band sealers are practical choices for packaging lines that need steady output without constant manual heat pressing. In suitable conditions, they can seal approximately 20–40 packs per minute. Actual speed depends on bag material, product shape, operator handling, and conveyor settings. A stable rhythm matters more than the highest displayed speed.

Seal widths commonly range from 3 to 12 mm. Narrow 3–5 mm seals suit lightweight pouches and dry products. Wider 8–12 mm seals provide more tolerance when packaging heavier contents or flexible films. The correct width should match the film structure, not just the product weight. Overheating can wrinkle the film, weaken the seal, or leave a burnt edge. It happens more easily than expected.

In daily operation, technicians should check temperature, belt speed, pressure, and seal appearance together. A clean, even seal usually indicates balanced settings. Pull testing can reveal weak bonding before a shipment leaves the facility. Dust around the sealing area also causes inconsistent results. I have found that operators often increase heat when the real issue is low contact pressure. That assumption can be wrong. Record settings for each packaging material, then review them after changes in humidity, film thickness, or filling volume. Small adjustments are usually safer than sudden increases.

Ultrasonic vs. Induction Sealers: 20–40 kHz Operation and Foil-Liner Needs

Packaging demand is becoming more material-sensitive. Smithers’ The Future of Global Packaging to 2028 estimates the global packaging market will exceed 1.2 trillion US dollars by 2028. That scale makes sealing reliability more important than headline speed.

Ultrasonic sealers commonly operate between 20 and 40 kHz. A horn converts electrical energy into mechanical vibration, creating localized heat at thermoplastic layers. This process can seal some films without a foil liner. It also reduces dependence on pre-applied aluminum structures. In factory trials, I would inspect seal width, peel strength, and leakage after vibration testing. Frequency alone proves very little. Pressure, amplitude, material thickness, and dwell time can change results sharply. A 20 kHz system may suit heavier structures, while higher frequencies can offer finer control. That is not a universal rule.

Induction sealing requires a compatible foil liner inside the closure. Electromagnetic energy heats the liner’s polymer coating, bonding it to the container rim. It is fast and produces a visible tamper-evident seal. However, liner compatibility is non-negotiable. The wrong coating, cap gap, or container resin can create weak edges or incomplete adhesion. PMMI packaging machinery reports repeatedly identify changeover flexibility and quality verification as practical purchasing concerns. Operators should test filled containers, not empty samples. I would also question impressive laboratory results when humidity, dust, and line speed were excluded. Real production is less polite.

Machine Selection: ASTM F88 Seal Strength, HACCP Compliance, and Cost per Pack

Choosing a hot sealing machine in 2026 should begin with the seal, not the purchase price. In production trials, I record jaw temperature, dwell time, pressure, film structure, and line speed. These details expose weak seals that a showroom sample can hide. ASTM F88 testing then measures seal strength through controlled peel tests. A high value is not automatically better. Overheating can distort film, damage product edges, or increase opening force. Short trials mislead.

For food packaging, HACCP alignment requires more than a clean-looking machine. The sealing step should appear in the hazard analysis, with defined limits, monitoring records, corrective actions, and verification. Operators need accessible contact surfaces, repeatable settings, and simple cleaning routines. I also check whether temperature sensors remain stable after long shifts. A machine may pass an installation check, yet drift later. That gap deserves attention.

Cost per pack should include film loss, rejected seals, labor, electricity, maintenance, tooling, and changeover time. One calculation I once underestimated was warm-up waste during frequent product changes. Another was the cost of rechecking questionable seals. Compare several machine types using the same film and target output. Record packs per hour, acceptable seal percentage, and downtime.

2026 Best Hot Sealing Machine Types for Packaging

Machine selection benchmark: ASTM F88 seal strength, HACCP control readiness, and estimated cost per sealed pack

Continuous band and rotary heat sealers generally provide lower pack costs at higher throughput, while vacuum chamber and ultrasonic systems can deliver stronger, more controlled seals for demanding applications. Seal strength is shown in N/15 mm in line with ASTM F88-style testing. HACCP readiness is a comparative operational score based on cleanability, process control, seal monitoring, and validation capability; it is not a certification. Costs are representative ranges and vary by packaging material, labor, volume, and line configuration.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.
