


What Are the 2026 Best 36 Pipe End Caps?

Choosing the best 36 Pipe End Caps in 2026 requires more than comparing prices or polished product photos. Buyers must examine material grade, pressure rating, wall thickness, sealing design, and manufacturing traceability. In real installations, a cap may face vibration, moisture, heat, chemical exposure, or repeated maintenance. A small dimensional error can leave a visible gap, damage threads, or weaken a welded joint.

Industry data supports this careful approach. Grand View Research continues to identify infrastructure renewal, process industries, and energy investment as major drivers for industrial piping demand. MarketsandMarkets also reports sustained growth in industrial valves and flow-control equipment, where compatible fittings and end closures remain essential components. These reports do not measure 36 Pipe End Caps directly. That limitation matters. Market forecasts can show direction, but they cannot prove that one cap performs better in a specific plant.

Relevant standards provide a stronger comparison point. ASME B16.9 addresses factory-made wrought butt-welding fittings, including caps, while ASTM specifications help define material and mechanical performance. For stainless-steel applications, MSS SP-43 may support evaluation of lighter-wall fittings and corrosion-resistant designs. Certification should be checked, not assumed.

The strongest products combine accurate dimensions, clean edges, consistent finish, and clear documentation. Look for heat numbers, inspection records, and pressure-test evidence where applicable. A 36-inch cap needs different handling from a small threaded model. Packaging also matters. Bent rims and scratched sealing surfaces are common, avoidable failures.

Some rankings remain subjective. That is worth admitting. The best choice depends on service conditions, installation method, and maintenance access. This guide compares those practical factors, not marketing claims alone.
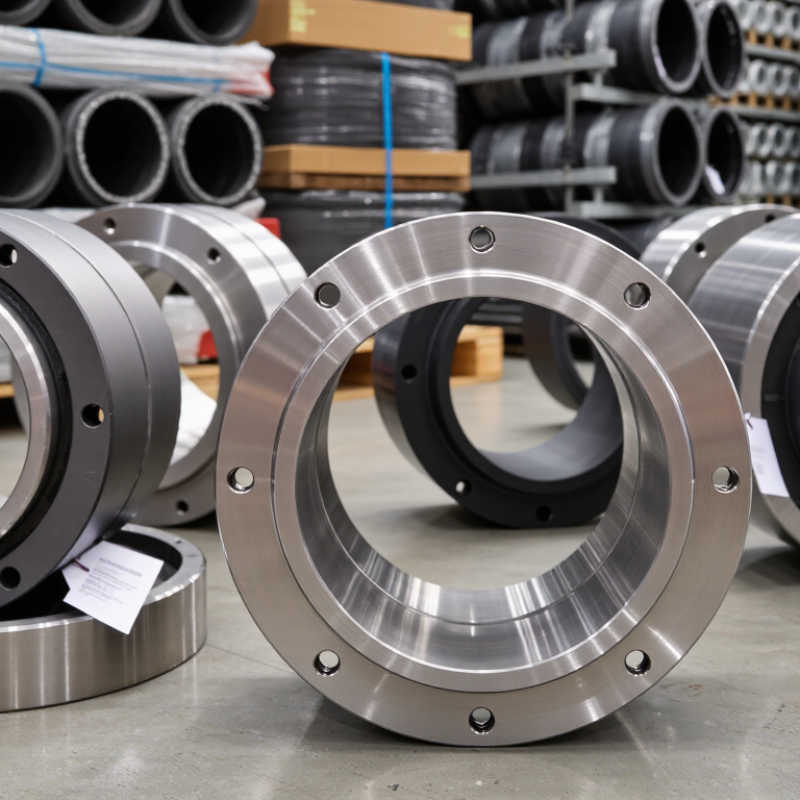
What Are the 2026 Best 36 Pipe End Caps?

## Defining 36 Pipe End Caps and Their Core Functions

A 36 pipe end cap is a protective fitting designed for a pipe with a nominal 36-inch diameter. It closes an open pipe end and helps prevent dust, rainwater, insects, and construction debris from entering. However, “36-inch” does not always equal the measured outside diameter. Pipe standards, wall thickness, and connection types can change the actual dimensions.

The core function is simple: provide a secure, stable closure. A suitable cap can also reduce corrosion risks, protect threads, and improve storage safety. Some caps support temporary isolation during transport or maintenance. Others are built for long-term outdoor exposure. Material selection matters. Plastic caps are lightweight and practical, while metal versions may offer stronger impact resistance. A reliable choice should match the pipe material, temperature range, pressure conditions, and installation method. Do not guess the fit. A small mismatch can cause movement, leakage, or damage. In practice, measurements are often rushed, and that is where mistakes begin.

Tips: Measure the pipe outside diameter, wall thickness, and end shape before ordering. Check whether the cap needs a seal, clamp, weld, or simple push fit. Inspect the cap after installation. It should sit evenly, without cracks, gaps, or excessive force. One detail is easy to overlook: removing the cap later should remain practical.

What Are the 2026 Best 36 Pipe End Caps? – Defining 36 Pipe End Caps and Their Core Functions

End Cap Type Connection Method 36-Inch Pipe Reference Common Materials Core Function Best-Fit Applications Key Selection Considerations
Butt-Weld Pipe Cap Welded directly to the pipe end NPS 36 has a nominal outside diameter of 36.00 in (914.4 mm); wall thickness depends on the selected pipe schedule Carbon steel, stainless steel, alloy steel Creates a permanent, pressure-resisting closure Process piping, water transmission, energy and industrial systems Match the cap wall thickness, material grade, weld procedure and design pressure to the pipe system
Ellipsoidal or Dished Cap Usually butt welded Available for large-diameter piping when a formed pressure boundary is required Carbon steel, stainless steel, nickel alloys Distributes internal pressure more efficiently than a simple flat plate High-pressure, high-temperature and vessel-connected piping Confirm the head geometry, thickness calculation, corrosion allowance and inspection requirements
Flat Plate End Cap Welded or mechanically attached Can be fabricated to suit a 36-in pipe outside diameter, subject to engineering design Carbon steel, stainless steel, aluminum Provides a basic end closure for low-pressure or non-pressure service Temporary isolation, atmospheric ducts, tanks and non-pressurized lines Not automatically suitable for pressure service; plate thickness and reinforcement must be engineered
Mechanical Test Cap Bolted, expanding or gasketed connection Sized for the actual 36-in pipe outside diameter and wall condition Steel, ductile iron, elastomeric sealing materials Allows temporary pressure testing without permanent welding Hydrostatic testing, commissioning and maintenance isolation Verify the rated test pressure, pipe roundness, gasket compatibility and required restraint
Threaded End Cap Internal or external pipe threads Generally uncommon for a 36-in main because large threaded connections are difficult to install and seal Malleable iron, carbon steel, stainless steel Provides a removable closure for smaller threaded piping Small-bore branches, instruments and low-volume service lines Usually not the preferred solution for a 36-in pipe; check thread standard, sealing method and access clearance
Flanged Blind End Closure Bolted flange with a gasket The flange size, bolt pattern and pressure class must match the 36-in pipe flange Carbon steel, stainless steel, alloy steel Provides a removable pressure boundary and convenient access Water mains, pump stations, inspection points and maintenance isolation Select the flange standard, pressure class, gasket type, bolt material and tightening method together
Push-On or Slip-On Protective Cap Push fit, clamp or light mechanical retention Sized to the actual outside diameter; not normally intended to seal a pressurized line Polyethylene, PVC, rubber, steel Protects pipe ends from impact, dirt, moisture and coating damage Storage, transportation, fabrication and site handling Confirm temperature range, ultraviolet exposure, chemical resistance and retention strength
Temporary Line-Stopping Cap Mechanical restraint, bolting or engineered closure system Requires an engineered design for the 36-in diameter, operating pressure and end-load forces Steel, ductile iron, elastomeric seals Temporarily isolates a section of pipeline during repair or modification Transmission pipelines, municipal water systems and emergency maintenance Use only with documented pressure limits, restraint calculations and qualified installation procedures
Technical note: In common piping terminology, “36-inch pipe” normally refers to NPS 36, whose nominal outside diameter is 36.00 in (914.4 mm). The actual wall thickness, inside diameter, pressure rating and end-cap dimensions depend on the pipe standard, schedule, material, connection type and service conditions. Butt-weld caps are commonly specified with ASME B16.9 dimensional requirements, while the applicable material and design standards must be confirmed for each project.

## Key Materials Used in 36 Pipe End Cap Manufacturing

For 2026, the best 36-inch pipe end caps will depend on material behavior, not appearance. Carbon steel remains practical for high-pressure industrial lines. ASTM A234 WPB covers common wrought fittings for moderate and elevated temperatures. Its weldable chemistry supports reliable fabrication, but field corrosion still demands coating or lining.

Stainless steel is valuable where moisture, chemicals, or cleaning cycles create aggressive exposure. ASTM A403 covers wrought austenitic stainless fittings, including grades commonly selected for corrosion resistance. The extra nickel and chromium increase cost. They also reduce maintenance risks. Still, stainless steel can suffer localized corrosion when chloride deposits remain under insulation.

Polyethylene offers another path for buried or water-service systems. The Plastics Pipe Institute’s PPI TR-4 lists PE4710 with a 1,600 psi hydrostatic design basis at 73°F. Its commonly applied hydrostatic design stress is 800 psi. That figure is useful, but temperature reduces pressure capacity. Installers must also control fusion alignment and cooling time. A slight ovality can remain unnoticed inside a 36-inch cap. That is an uncomfortable weakness. ASME B16.9 dimensional checks help control end-to-end fit, wall transitions, and welding preparation. In practice, I would inspect the bevel, measure wall thickness, and verify the pressure class before selection. The material choice is never complete without service temperature, fluid chemistry, joining method, and burial conditions.

## How to Compare the Best 36 Pipe End Cap Designs

Choosing the best 36 pipe end cap design requires more than checking its listed diameter. Confirm the pipe’s outside diameter, wall thickness, material, and service conditions. A cap that looks correct may still loosen under vibration or temperature changes. Measure the pipe twice. Small errors become expensive on large pipe.

For a 36-inch application, compare sealing method, wall strength, and installation effort. Push-fit caps suit temporary protection and clean storage areas. Bolted or welded designs offer stronger retention for demanding systems, but they require better preparation and inspection. Check pressure ratings, temperature limits, corrosion resistance, and available test records. Reliable suppliers should provide material details and clear dimensional drawings. I have found that removal access is often overlooked. A cap that seals well can still be frustrating during maintenance.

Tips: Inspect the rim for dents before fitting. Clean dust, oil, and burrs from contact surfaces. Use calibrated tools for measurement. Test the finished connection under controlled conditions. Do not choose the thickest cap automatically; excess weight can complicate handling. My own comparison process is not perfect, especially when field measurements are incomplete. Rechecking assumptions prevents a confident but unsuitable choice. Look for designs that balance protection, durability, traceability, and practical installation.

## Installation, Compatibility, and Maintenance Considerations

When evaluating the 36 best pipe end caps for 2026, installation begins with accurate measurement.

Confirm the pipe’s outside diameter, wall thickness, thread profile, and pressure rating. A cap that looks correct may still leak under vibration or thermal expansion. Measure twice.

Select the connection style according to the pipe system. Push-fit caps suit temporary closures, while threaded caps provide firmer service access. Welded or solvent-bonded caps need compatible materials and controlled preparation.

Clean the pipe end, remove burrs, and keep sealing surfaces dry. For pressurized lines, follow the applicable installation standard and test gradually after fitting. Do not tighten aggressively; damaged threads can be difficult to detect.

Compatibility also depends on temperature, chemicals, sunlight, and movement. Elastomer seals may harden in heat or swell when exposed to unsuitable fluids. Metal caps can resist impact, yet corrosion may appear inside hidden joints. During maintenance, inspect for cracks, staining, looseness, and seal distortion. Replace questionable parts rather than forcing them back into service.

I have found that simple visual checks miss small failures. Use a pressure gauge when the system allows it. Record installation dates and unusual operating conditions. That record helps identify repeated problems. Still, material charts are not perfect for every mixed system. A qualified technician should verify uncertain applications, especially where failure could interrupt essential service or damage nearby equipment.

## Safety Standards and Selection Criteria for 2026

What Are the 2026 Best 36 Pipe End Caps?

Safety Standards and Selection Criteria for 2026

For 36-inch piping, the best end cap begins with verified service conditions. Confirm the pipe’s outside diameter, wall thickness, design pressure, and operating temperature. A cap that fits physically may still fail under pressure. Fit matters. For welded systems, review dimensions against applicable standards such as ASME B16.9, when relevant. Material selection should match the pipe and the transported medium. Carbon steel, stainless steel, and alloy materials behave differently during welding and thermal cycling. Check the material certificate, heat number, and manufacturing records. Document everything.

Field experience shows that poor storage can damage an otherwise suitable cap. Inspect bevels for dents, corrosion, and sharp distortion before installation. For pressure service, require qualified welding procedures and competent welders. Non-destructive testing may include visual, radiographic, ultrasonic, or dye penetrant inspection, depending on the risk. Temporary dust covers are not pressure closures. Never confuse them. Consider internal cleanliness, drainage, lifting points, and access for inspection. Some selection decisions remain imperfect because project data arrives late. That weakness deserves review, not assumption. Ask whether the cap’s pressure rating, traceability, and inspection plan remain valid after installation. Reliable suppliers should provide clear test records, dimensional reports, and material documentation without unexplained gaps.

What Are the 2026 Best 36-Inch Pipe End Caps?

Safety Standards and Selection Criteria for NPS 36 / DN 900

The chart shows whether commonly referenced butt-welding fitting standards include NPS 36 (approximately DN 900) within their published size scope. A value of 1 means the size is included; 0 means it is outside the stated range.

For a safe 2026 selection, verify the applicable dimensional standard, material specification, wall thickness, design pressure and temperature, weld preparation, corrosion allowance, traceability, and required inspection or non-destructive examination. Final acceptance should follow the project specification and the applicable standard edition.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.


