


Choosing the right machine in 2026 requires more than comparing speed, price, and catalog photos. Global buyers need equipment that matches fin geometry, alloy behavior, production volume, and local service conditions. An Aluminum Fin Press Machine can shape delicate fins accurately, but its value depends on repeatability, tooling quality, and operator control. Small errors can cause uneven spacing, cracked edges, or rejected heat exchanger assemblies. Those details matter on the factory floor.
This introduction will examine major Aluminum Fin Press Machine types available to international manufacturers. It will consider mechanical, hydraulic, servo-driven, and customized configurations. Each type offers different benefits for speed, force control, energy use, maintenance, and expansion. Buyers should also review stroke length, die compatibility, feeding accuracy, safety systems, and spare-part availability. A machine may appear efficient during a demonstration. Real performance can change with thicker aluminum sheets, frequent die changes, or inexperienced operators.
Practical experience often reveals limitations that specifications hide. Service response times can matter as much as rated capacity. Supplier testing records, installation support, and training deserve careful attention. Certification requirements may also differ between markets, so technical documents should be verified before purchase. Not every recommendation fits every factory. Some conclusions remain conditional because production data is often incomplete. That uncertainty should be stated clearly, not disguised with impressive numbers. The following guide offers a balanced framework for comparing machine types, reducing avoidable costs, and selecting dependable equipment for long-term aluminum fin production.
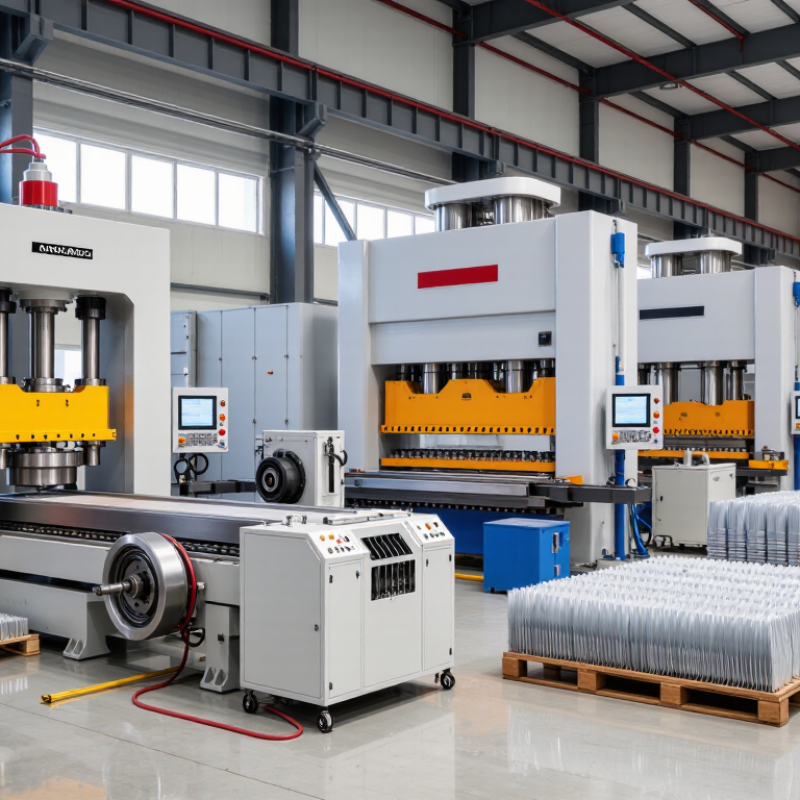
An aluminum fin press machine forms thin aluminum sheets into repeated fins for heat exchangers, radiators, and cooling coils. It uses a shaped punch and die to create louvers, collars, or corrugated profiles. The machine does not simply cut metal. It controls feeding, pressing, forming, and strip movement as one coordinated process.
A typical line includes a decoiler, straightener, servo feeder, press unit, and collection system. The decoiler releases the aluminum coil at a controlled speed. Rollers remove coil memory and flatten the strip. The feeder then advances a precise length before each stroke.
Inside the press, forming tools shape the fin geometry. Small errors matter. A slight pitch change can reduce airflow or complicate assembly.
Common 2026 configurations include high-speed stamping presses, multi-station fin presses, and flexible servo-driven models. High-speed machines suit stable, large-volume production. Multi-station systems perform several forming steps within one cycle. Servo models offer better control for varied fin heights and materials.
In practice, the first setup is rarely perfect. Operators may adjust feed length, tool clearance, and lubrication after inspecting several samples. Burrs, uneven collars, and wrinkled edges often reveal poor alignment rather than defective aluminum.
Experienced technicians check fin pitch with gauges and inspect the strip under consistent lighting. Machine speed helps, but repeatable accuracy matters more.

Aluminum fin press machines are mainly classified by how the strip changes shape. In factory evaluations, I usually separate them into stamping, progressive forming, and roll forming systems. Each method leaves different marks on production speed, fin geometry, and tooling cost.
Stamping presses use a punch and die to cut, pierce, or shape aluminum sheet. They suit flat fins, simple louvers, and moderate production volumes. Progressive presses perform several operations in one tool. The strip advances through stations, while cutting, drawing, and louvering happen in sequence. This method supports complex fins and high output. Roll forming uses paired rollers to create continuous waves or corrugations. It offers stable feeding and less interrupted production, but it may struggle with deep, irregular shapes. Some suppliers use hybrid lines, combining rolling and pressing. Classification can become less clear there.
Tips: Check the forming method against alloy temper, strip thickness, fin pitch, and target speed. Ask for sample parts, measured burr height, and repeatability data. A machine that looks fast may waste material during setup. I have seen buyers focus on strokes per minute and overlook die changes, feeding accuracy, and maintenance access. That mistake is understandable, but expensive. Run a realistic trial before approving the final configuration.
Choosing the right aluminum fin press machine depends on fin geometry, material thickness, and production volume. Different designs need different forming control.
For flat plate fins, a single-station mechanical press can suit small batches and frequent design changes. It offers simpler tooling and easier access for adjustments. Short runs matter.
Louvered and wavy fins usually require a high-speed press with accurate coil feeding. These machines maintain consistent pitch across long production cycles. A progressive die press is suitable for large quantities because it combines piercing, forming, and cutting in one sequence. However, complex dies cost more and require skilled maintenance.
For serrated, offset, or perforated fins, multi-station systems provide better control over each forming step. Servo feeding can improve positioning accuracy, especially when fin spacing is narrow. Production teams should check strip width, tensile strength, burr limits, and die-change time before purchase. A machine that handles thick aluminum may not perform well with thin foil.
From factory trials, unstable feeding often causes more waste than slow pressing speed. The first sample run may reveal springback, uneven louvers, or damaged edges. That result is useful, not embarrassing. Buyers should request measured samples under real material conditions, rather than trusting brochure capacity alone. Small manufacturers may prefer flexible presses, while high-volume plants need uptime, automation, and repeatable tolerances.#+#+#+#+
Indicative production-speed ranges help match machine types with fin designs and production scales. Mechanical and servo presses generally suit high-volume stamping, while pneumatic and hydraulic systems are better for flexible, lower-volume or heavier forming applications. Actual output depends on fin height, material thickness, pitch, tooling, stroke length and automation.
Global buyers should compare aluminum fin press machines by process results, not headline tonnage. The International Aluminium Institute reported about 70 million tonnes of primary aluminum production in 2023, showing the scale of pressure on efficient forming equipment. Check rated force, stroke length, ram speed, feed accuracy, and coil-width range. A practical machine should maintain stable pitch at high speed, even when thin aluminum strips flex or vary slightly. Speed is not everything.
Servo feeding can reduce pitch errors and support quick product changes. Ask for measured repeatability, not only brochure claims. A reasonable evaluation includes sample trials, dimensional inspection, noise readings, and energy consumption per finished meter. The U.S. Department of Energy’s industrial efficiency guidance emphasizes measuring equipment performance under actual operating conditions. That detail matters. Also compare die-change time, lubrication control, access for cleaning, and spare-part availability. Safety systems should align with ISO 12100 and applicable electrical safety requirements. Remote monitoring is useful, but poor sensors create misleading data. I would request at least three months of production records before trusting digital dashboards. A buyer should also inspect guarding, emergency stops, overload protection, and maintenance access. The best machine is rarely the fastest one; it is the one that keeps fin geometry consistent during long, ordinary shifts.
| Machine Type | Working Principle | Typical Production Speed | Typical Aluminum Strip Thickness | Typical Strip Width Range | Stroke / Feed Control | Dimensional Repeatability | Energy and Drive Characteristics | Best-Suited Fin Products | Key Advantages | Limitations to Compare |
|---|---|---|---|---|---|---|---|---|---|---|
| High-Speed Mechanical Fin Press | Motor-driven crankshaft or eccentric mechanism converts rotary motion into a fixed reciprocating slide motion. | Approximately 300–800 strokes/min | About 0.08–0.30 mm | 100–600 mm | Fixed or adjustable stroke; mechanical roll feeder or servo feeder is commonly used. | Generally suitable for stable, high-volume production when tooling, feeder alignment, and material quality are well controlled. | High installed power and efficient operation at full production speed; flywheel and clutch-brake condition are important. | Flat fins, louvered fins, wavy fins, and high-volume HVAC or automotive heat-exchanger fins. | High output Proven structure Lower cost per part | Less flexible for frequent changes in stroke profile; shock, noise, vibration, and clutch-brake maintenance must be assessed. |
| Servo-Driven Fin Press | A programmable servo motor directly controls slide position, speed, dwell, and motion profile. | Approximately 150–600 strokes/min | About 0.08–0.40 mm | 100–800 mm | Fully programmable stroke and feed synchronization; electronic cam profiles are available on advanced systems. | High repeatability, especially during short production runs, variable-pitch forming, and controlled forming zones. | Regenerative braking and variable-speed operation can reduce energy use during idle or low-load periods. | Variable-pitch fins, delicate louvered fins, multi-specification production, and applications requiring controlled forming. | Flexible motion control Lower setup waste Reduced mechanical shock | Higher initial investment; drive system, encoder, software, and servo motor support should be verified for local serviceability. |
| Hydraulic Fin Press | Hydraulic cylinders generate slide force through a pump, valve system, and controlled hydraulic circuit. | Approximately 20–100 strokes/min | About 0.15–1.00 mm | 200–1,200 mm | Adjustable stroke, pressure, speed, and dwell time; programmable control is commonly available. | Good force control and overload protection; final fin accuracy depends strongly on hydraulic stability and tooling condition. | Higher idle energy consumption is possible; hydraulic oil temperature, leakage prevention, and filtration are key considerations. | Thicker aluminum parts, low-to-medium volume production, large fin blanks, and forming operations requiring high force. | High forming force Adjustable pressure Overload protection | Lower production speed, possible oil leakage, more heat generation, and higher maintenance requirements than a basic mechanical press. |
| Progressive-Die Fin Press Line | A continuous strip passes through multiple die stations for piercing, louvering, forming, cutting, and other sequential operations. | Approximately 200–700 strokes/min | About 0.08–0.35 mm | 100–500 mm | Servo roll feed with automatic pitch control; die stations determine the complete forming sequence. | High part-to-part consistency when strip tension, die clearance, feed pitch, and press rigidity are properly controlled. | Efficient for continuous production; material utilization depends on strip layout and scrap management. | High-volume louvered, slit, pierced, and formed fins produced from coil stock. | Integrated operations High automation Consistent output | Die design and maintenance are complex; a tooling change may require significant time and skilled technicians. |
| Multi-Row or Multi-Lane Fin Press | Two or more fin lanes are formed simultaneously using shared or individually adjustable tooling and feeding systems. | Approximately 200–600 strokes/min | About 0.08–0.30 mm | 300–1,200 mm total working width | Multi-lane servo feed or synchronized mechanical feed; lane spacing and pitch should be adjustable. | Good productivity with consistent lane-to-lane quality when the press frame and feeder are sufficiently rigid. | Higher throughput per press footprint; power demand increases with the number of active lanes and forming load. | High-volume heat-exchanger cores requiring repeated fin widths, multiple lanes, or parallel production. | High area productivity Reduced floor space Parallel production | More complicated setup and alignment; one tooling problem can affect several lanes at the same time. |
| Cut-to-Length and Fin Forming Press Line | Coil material is uncoiled, straightened, cut or indexed, and formed into individual fin plates or segmented fin components. | Approximately 30–200 cycles/min | About 0.15–0.80 mm | 200–1,500 mm | Servo indexing with programmable blank length, feed pitch, and forming sequence. | Suitable for accurate blank length and repeatable formed geometry when straightening and cutting systems are correctly calibrated. | Energy consumption varies by cutting, forming, and material-handling equipment; line integration affects total efficiency. | Plate fins, segmented fins, thicker fins, and products that cannot be made efficiently by continuous high-speed stamping. | Flexible blank sizes Suitable for thicker stock Integrated handling | Usually slower than continuous strip stamping; line length, material handling, and changeover requirements can be greater. |
For global buyers, selecting an aluminum fin press machine means comparing more than stroke, speed, and tonnage. Progressive, high-speed, and servo-assisted presses suit different fin geometries and production volumes. A supplier should explain why one type fits your material thickness, coil width, and tolerance targets. Ask for sample parts, measured flatness, burr photos, and a recorded cycle test. Ask for evidence.
Supplier evaluation should begin with traceable engineering records, not polished brochures. Review machine drawings, component specifications, inspection procedures, and technician training records. An on-site audit can reveal poor guarding, improvised wiring, weak lubrication practices, or limited spare-part control. Request factory acceptance testing with your actual aluminum alloy and tooling. The results should include repeatability data, noise readings, emergency-stop checks, and an operator training log. Compliance documents must match the delivered machine, including risk assessments, electrical diagrams, manuals, and destination-market declarations. Documents can be copied.
Total operating cost often hides inside tooling changes, coil scrap, electricity, compressed air, maintenance, and unplanned downtime. Compare five-year costs using realistic shift hours and local utility rates. Include die refurbishment, software updates, technician travel, and disposal of worn components. A faster press may waste more metal if feeding is unstable. That trade-off matters. I would request references from buyers running similar fin profiles, though reference checks can be incomplete. One missed question remains: who owns process knowledge when production problems appear? Put response times, training scope, warranty limits, and spare-part availability into the contract.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

